Carbon black and coal powder are critical raw materials in various industrial applications, and efficient material handling systems are essential for their safe and reliable transport. This article explores the fundamental principles of carbon black and coal powder material handling systems, as well as the specific working scene characteristics that define their operational effectiveness. The discussion will focus on the technical aspects, design considerations, and practical applications of these systems, providing insights into how they contribute to industrial processes.
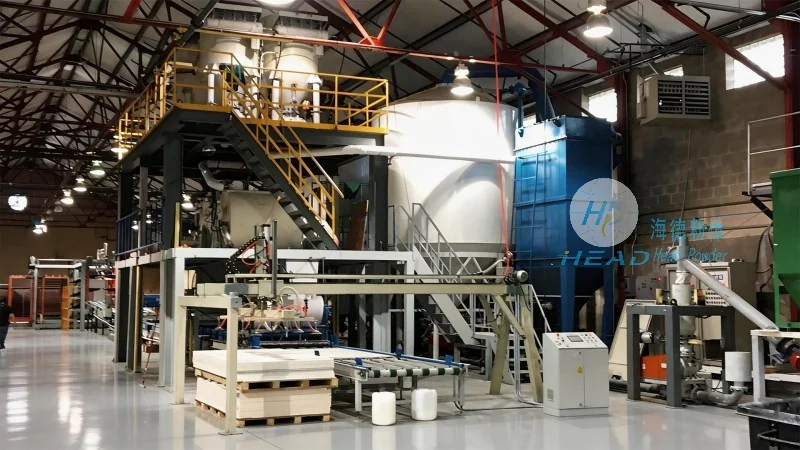
The core principle of carbon black and coal powder material handling systems revolves around the efficient and safe transfer of fine particulate materials. These systems are engineered to handle materials with high dust content and low bulk density, which can pose challenges in traditional conveying methods. The primary goal is to ensure minimal material loss, maintain consistent flow rates, and prevent dust emissions that could compromise safety and environmental compliance. Key components typically include feeders, conveyors, and control systems, all designed to work in harmony to achieve these objectives.
Carbon black and coal powder material handling systems operate in diverse industrial environments, each with unique characteristics that influence system design and performance. For instance, in manufacturing facilities, these systems may be integrated into production lines where materials are processed and transformed into end products. The working scene often involves high-volume material flow, requiring robust and reliable equipment that can handle continuous operation without interruption. Additionally, the systems must be adaptable to varying material properties, such as changes in moisture content or particle size, which can affect flow behavior and system efficiency.
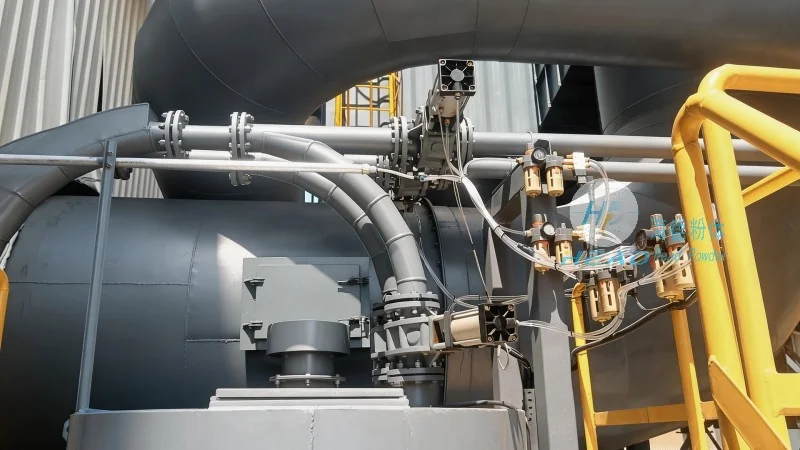
The design of carbon black and coal powder material handling systems is tailored to meet the specific demands of industrial applications. Key technical specifications include the type of conveyor (e.g., pneumatic, mechanical, or hybrid systems), the capacity of the system, and the control mechanisms used to regulate material flow. Pneumatic conveying systems, for example, use air pressure to transport fine powders, offering advantages in terms of low maintenance and the ability to handle abrasive materials. Mechanical conveyors, such as screw or belt conveyors, are also common, providing high efficiency and reliability in bulk material transport. The choice of system depends on factors like material characteristics, operational environment, and cost considerations.
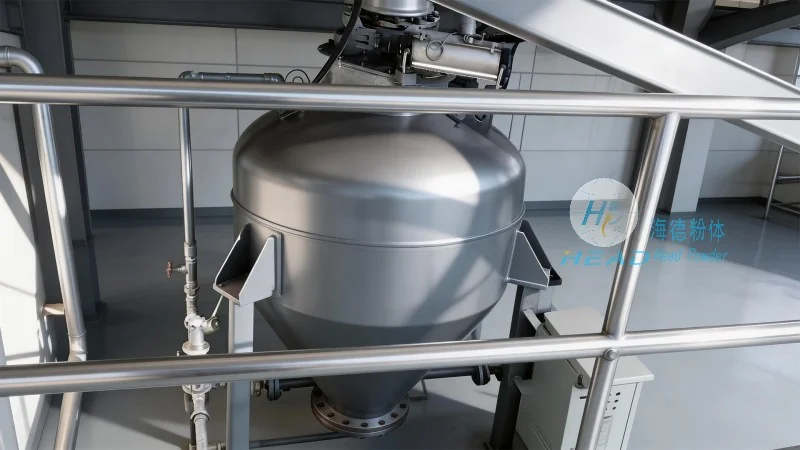
Carbon black and coal powder material handling systems are widely used across various industries, including chemical manufacturing, power generation, and mining. In the chemical industry, these systems facilitate the transport of raw materials to reactors and processing units, ensuring a steady supply of feedstock for production. In power plants, coal powder handling systems are critical for supplying fuel to boilers, while carbon black systems support the production of rubber and plastic products. The integration of these systems into industrial processes enhances productivity and reduces downtime, making them indispensable components of modern manufacturing operations.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized material handling solutions for carbon black and coal powder applications. With a strong presence in China, particularly in Shandong province, the company leverages advanced engineering and manufacturing capabilities to deliver high-quality systems that meet the unique needs of industrial clients. Headpowder's expertise lies in designing and implementing customized material handling solutions that optimize efficiency, safety, and environmental performance. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the industry, offering comprehensive support from system design to installation and maintenance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top