For industrial operations involving corn starch, efficient material handling is crucial to ensure smooth production processes and maintain product quality. The corn starch material handling system, as developed by Shandong HeadPowder Engineering Co., Ltd., is designed to address the unique challenges associated with transporting and managing this granular material. This system integrates advanced engineering principles and practical application scenarios to provide a reliable solution for various industrial environments.
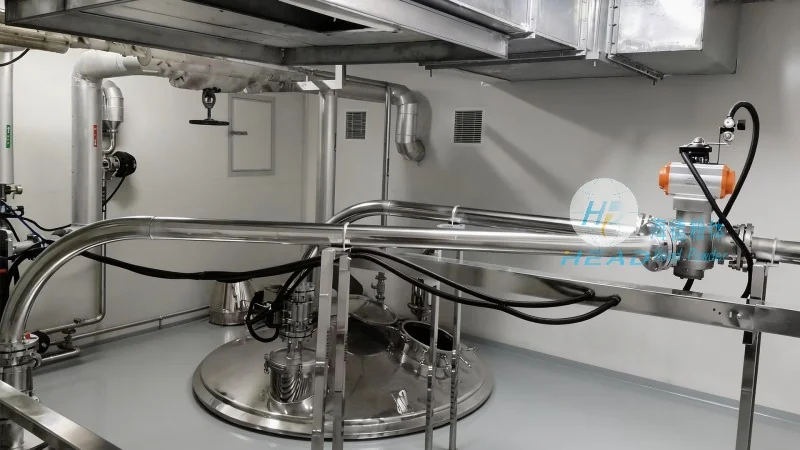
The core principle of the corn starch material handling system is based on the efficient transfer of bulk materials through a combination of mechanical components and control mechanisms. The system typically utilizes conveyor belts, screw conveyors, or pneumatic conveying equipment to move corn starch from storage areas to processing units or packaging stations. The design emphasizes minimal material degradation, consistent flow rates, and easy maintenance, which are critical factors for maintaining the integrity of corn starch products. The system's control system, often equipped with sensors and automation features, ensures precise monitoring of material levels, flow rates, and operational status, enhancing overall process control and reducing downtime.
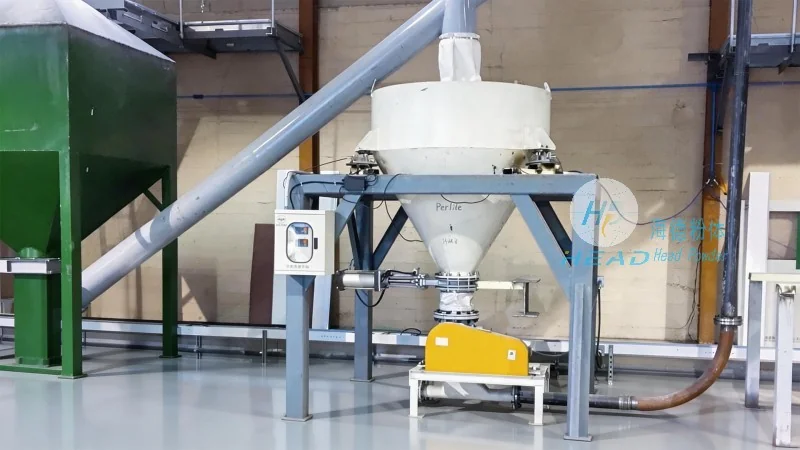
Several key components work in tandem to ensure the effective operation of the corn starch material handling system. The storage silos or hoppers are designed to hold large quantities of corn starch, with features such as aeration and temperature control to prevent caking or moisture buildup. The conveyor system, which may include belt conveyors for horizontal transport or bucket elevators for vertical movement, is engineered to handle the specific characteristics of corn starch, such as its fine particle size and potential for static electricity. The feeding mechanisms, often equipped with adjustable speed controls and material flow sensors, ensure a consistent feed rate to downstream equipment. Additionally, the system may incorporate dust collection and filtration systems to maintain a clean and safe working environment, which is essential for both operational efficiency and worker safety.
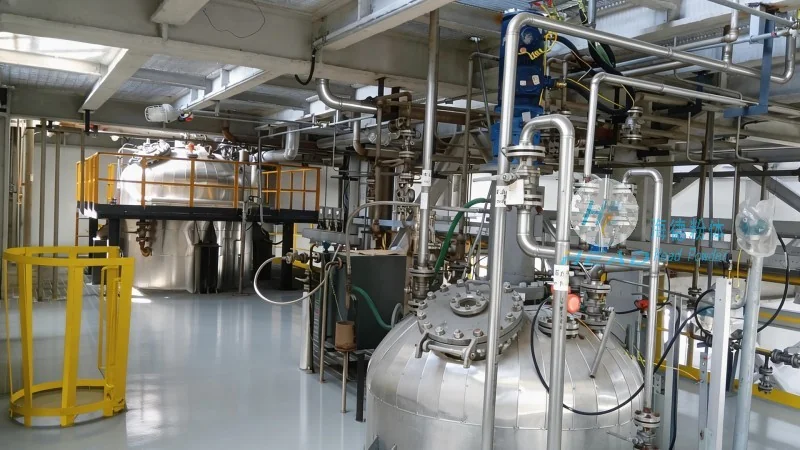
The working scene characteristics of the corn starch material handling system are tailored to meet the demands of different industrial applications. In food processing facilities, the system is designed to maintain high standards of hygiene and product purity, with components that are easy to clean and sanitize. In chemical or pharmaceutical applications, the system may incorporate additional safety features, such as explosion-proof designs and material compatibility checks, to ensure compliance with regulatory requirements. The system's adaptability also allows it to be integrated into existing production lines, minimizing the need for major infrastructure changes. Furthermore, the system's energy efficiency and low maintenance requirements make it suitable for continuous operation in large-scale industrial settings.
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented corn starch material handling systems in various industries, demonstrating their versatility and effectiveness. For example, in a large-scale corn starch production plant, the system was integrated to handle the entire material flow from raw corn processing to final product packaging. The system's ability to maintain consistent flow rates and prevent material degradation ensured a stable production output, while the automated control features reduced the need for manual intervention. Another application involved a food processing facility that required a system capable of handling both raw and processed corn starch, with the ability to switch between different product lines. The system's modular design allowed for easy reconfiguration, meeting the changing demands of the facility. These case studies highlight the practical benefits of the corn starch material handling system, including improved operational efficiency, reduced downtime, and enhanced product quality.
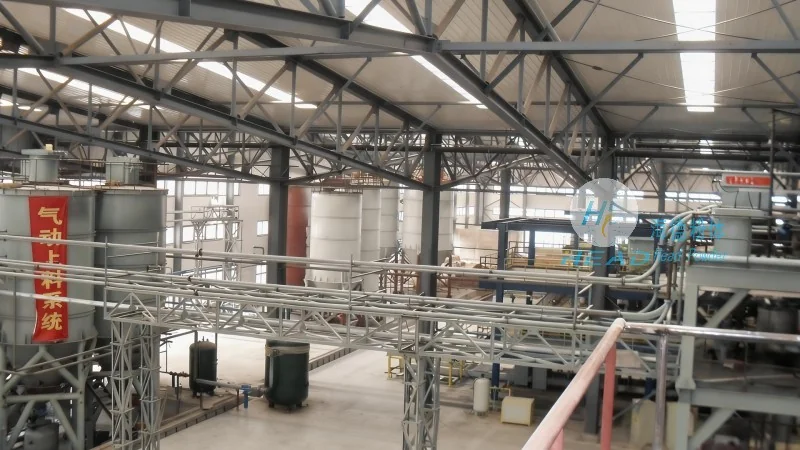
The corn starch material handling system developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in bulk material handling technology. By combining advanced engineering principles with practical application scenarios, the system provides a reliable and efficient solution for industries dealing with corn starch. The system's adaptability, energy efficiency, and low maintenance requirements make it a valuable asset for any industrial operation. As technology continues to evolve, future developments may include even more sophisticated automation features, such as artificial intelligence-driven process optimization and predictive maintenance systems. However, the core principles of the system—efficient material transfer, minimal degradation, and easy maintenance—will remain fundamental to its continued success in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top