Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design and implementation of efficient material handling solutions for sodium bicarbonate. Based in Shandong, China, the company leverages advanced engineering principles to develop systems tailored to the unique requirements of this chemical. This article explores the fundamental principles behind these systems and highlights key working scene characteristics that define their operational effectiveness.
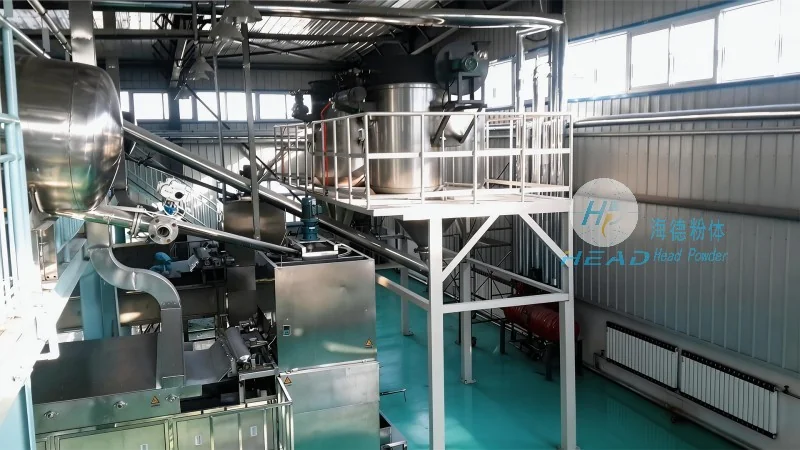
The operation of sodium bicarbonate material handling systems is grounded in several critical principles that ensure safe, efficient, and reliable transport of the material. First, the system must account for the physical properties of sodium bicarbonate, such as its granular structure and potential for dust generation. This requires the use of specialized equipment like screw conveyors, pneumatic conveyors, or belt conveyors, each chosen based on the specific application and environmental conditions. Second, the system must prioritize safety measures to prevent dust explosions, a common concern with powders like sodium bicarbonate. This includes implementing explosion-proof designs, proper ventilation systems, and material grounding to eliminate static electricity. Third, the system is designed for scalability and adaptability, allowing for adjustments in capacity and configuration to meet changing production demands. By integrating these principles, the system ensures consistent performance and minimal downtime.
The working scene characteristics of sodium bicarbonate material handling systems vary significantly based on the application and industrial setting. In industrial manufacturing facilities, these systems are often integrated into larger production lines, where they handle bulk quantities of sodium bicarbonate from storage to processing units. The key characteristics in such scenarios include high throughput rates, precise control over material flow, and integration with other equipment like mixers, reactors, or packaging machines. For example, in food processing or pharmaceutical industries, the system must maintain strict hygiene standards, which is achieved through stainless steel construction, easy-to-clean surfaces, and sealed components to prevent contamination. In contrast, in chemical processing plants, the system may operate in more demanding environments, requiring robust materials and corrosion-resistant components to withstand exposure to moisture or other chemicals. Another important characteristic is the system's ability to handle varying particle sizes and moisture content, ensuring consistent material quality throughout the transport process. This adaptability is crucial for maintaining product integrity and preventing clogging or blockages in the conveyor lines.
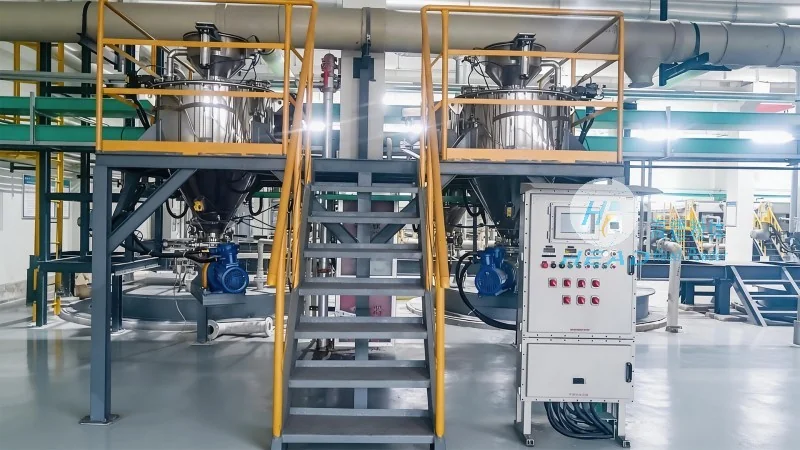
System design plays a crucial role in optimizing the performance of sodium bicarbonate material handling systems. The design process involves careful consideration of factors such as the material's flow characteristics, the required transport distance, and the desired throughput. For instance, screw conveyors are ideal for horizontal or slightly inclined transport, as they can handle a wide range of particle sizes and maintain a consistent flow rate. Pneumatic conveyors are better suited for vertical or long-distance transport, as they can move material quickly and efficiently through a pipeline. The system also incorporates control systems that allow for real-time monitoring and adjustment of the conveyor speed, ensuring that the material is transported at the optimal rate. This not only improves efficiency but also reduces energy consumption and operational costs. Additionally, the system is equipped with sensors and alarms to detect any abnormalities, such as blockages or excessive dust levels, allowing for immediate intervention and preventing potential damage to the equipment or the material.
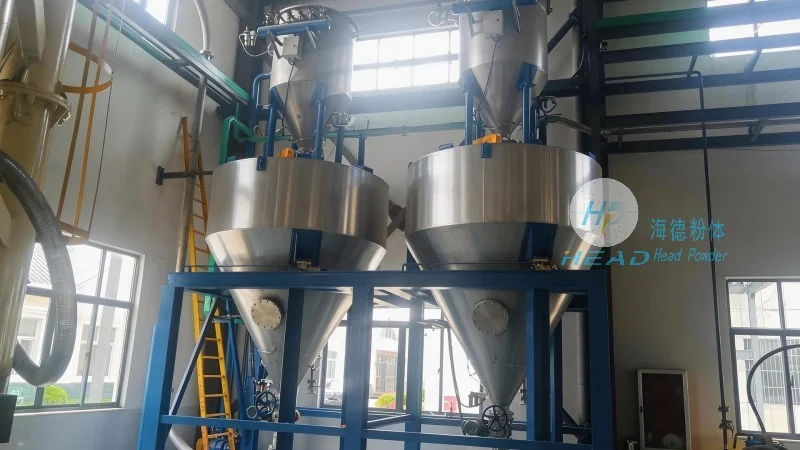
Each application of sodium bicarbonate material handling systems has unique considerations that influence the system's design and operation. In food processing, for example, the system must meet strict regulatory requirements regarding hygiene and product safety. This includes the use of food-grade materials, such as stainless steel and polyethylene, and the implementation of cleaning-in-place (CIP) systems to ensure thorough sanitation. The system is also designed to minimize cross-contamination, with separate conveyor lines for different products or batches. In pharmaceutical manufacturing, the system operates in a controlled environment, requiring additional measures such as HEPA filtration and laminar flow to maintain air quality. The system is also equipped with sterilization capabilities to prevent microbial contamination of the sodium bicarbonate. In chemical processing, the system may need to handle materials with higher moisture content or corrosive properties, which requires the use of specialized materials like Hastelloy or PTFE-coated components. The system's design also considers the need for temperature control, as some applications may require the material to be transported at specific temperatures to maintain its properties.
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive material handling solutions for sodium bicarbonate that are based on sound engineering principles and tailored to the specific needs of each application. The systems are designed to ensure safety, efficiency, and adaptability, making them suitable for a wide range of industrial settings. By understanding the core principles and working scene characteristics, businesses can select the most appropriate material handling system to meet their production requirements and maintain high standards of quality and safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top