HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in the design, development, and supply of advanced pneumatic conveying systems. This article delves into the core principles of the potassium carbonate fertilizer pneumatic conveying equipment and highlights its key working scene characteristics, providing a comprehensive overview for industry professionals seeking efficient and reliable fertilizer handling solutions.
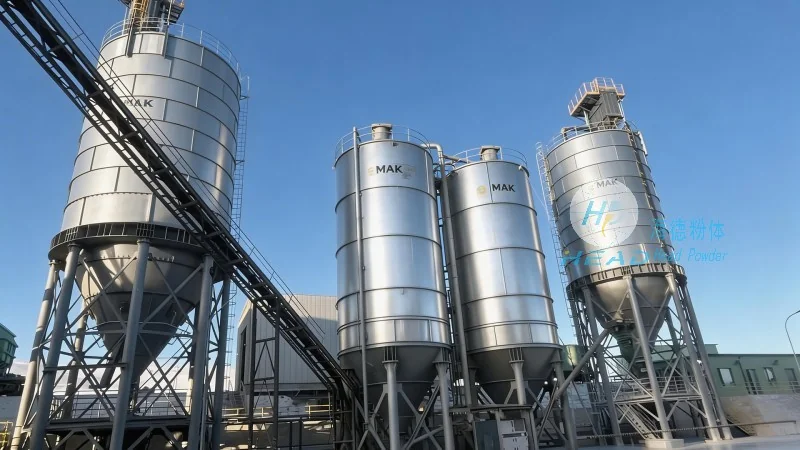
The pneumatic conveying system for potassium carbonate fertilizer operates on the fundamental principle of using compressed air to transport bulk materials through a pipeline network. Unlike traditional mechanical conveying methods, this technology relies on the dynamic interaction between the material and the air flow, enabling the efficient movement of fertilizer from storage silos to processing or packaging units. The system typically consists of several key components, including a hopper, a rotary valve, a venturi or pressure drop device, and a receiver or discharge point. The compressed air, often supplied by a blower or compressor, creates a pressure differential that propels the fertilizer particles through the pipeline. The design of the conveying line, including the pipe diameter, length, and bends, is crucial for maintaining optimal air velocity and preventing material degradation or blockages. The rotary valve at the inlet ensures a controlled and continuous feed of fertilizer into the system, while the venturi or pressure drop device regulates the air flow and pressure, ensuring consistent conveying performance. The receiver at the discharge end collects the fertilizer and may include a silo or storage tank for further processing. This principle allows for a clean, dust-free, and hygienic handling of potassium carbonate fertilizer, which is essential for maintaining product quality and adhering to industry standards.
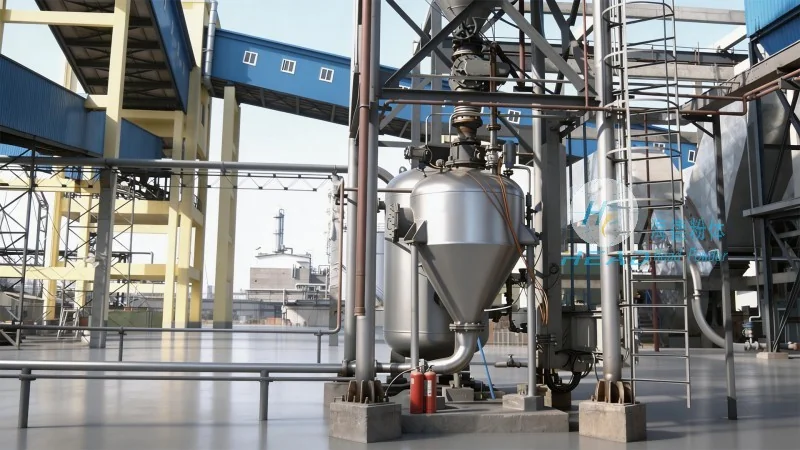
The working scene characteristics of the potassium carbonate fertilizer pneumatic conveying equipment are tailored to meet the specific demands of fertilizer production and distribution environments. These characteristics include high conveying efficiency, which allows for the rapid and continuous movement of large volumes of fertilizer, reducing downtime and increasing overall productivity. The system is also designed for flexibility, enabling the integration with existing production lines and the ability to adapt to varying production rates. Another critical characteristic is its ability to handle abrasive materials, such as potassium carbonate, without causing excessive wear on the conveying components. This is achieved through the use of high-quality materials, such as stainless steel or special alloys, for the pipeline and valves, ensuring long service life and minimal maintenance. The equipment is also equipped with advanced control systems that allow for real-time monitoring of the conveying process, including air pressure, flow rate, and material level. This enables operators to quickly identify and resolve any issues, ensuring smooth and uninterrupted operation. Additionally, the pneumatic conveying system is known for its low maintenance requirements compared to mechanical systems, as there are fewer moving parts and less wear and tear. This translates into lower operational costs and increased reliability over the long term. The working scene characteristics also emphasize the importance of safety and environmental compliance. The system is designed to minimize dust emissions and prevent the release of harmful particles into the environment, which is crucial for maintaining a safe working environment and complying with regulatory requirements. The use of sealed pipelines and proper ventilation systems further enhances safety and reduces the risk of accidents. Overall, the working scene characteristics of the potassium carbonate fertilizer pneumatic conveying equipment make it an ideal solution for modern fertilizer production facilities, offering a combination of efficiency, reliability, and safety.
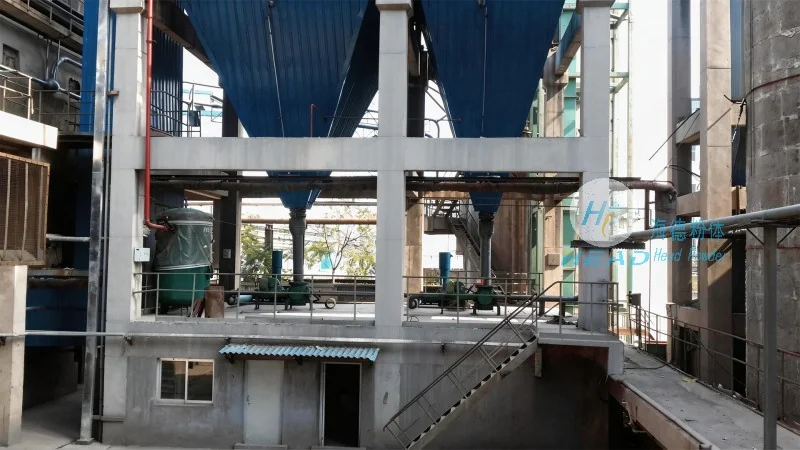
The potassium carbonate fertilizer pneumatic conveying equipment is widely used in various industrial applications, particularly in the fertilizer manufacturing and processing sectors. One of the primary application scenarios is in large-scale fertilizer production plants, where the equipment is used to transport bulk potassium carbonate from storage silos to the mixing and granulation units. This ensures a consistent and controlled feed of raw material, which is essential for maintaining product quality and production efficiency. The system is also utilized in fertilizer blending facilities, where different fertilizer components are combined to create customized formulations. The pneumatic conveying equipment allows for precise and uniform mixing of the components, ensuring that the final product meets the required specifications. Another application scenario is in fertilizer packaging lines, where the equipment is used to transport the fertilizer from the production line to the packaging machines. This enables a seamless and automated packaging process, reducing manual handling and increasing packaging speed. The equipment is also suitable for use in agricultural supply chains, where it can be integrated with bulk storage and distribution systems. This allows for the efficient transport of potassium carbonate fertilizer from the production plant to the distribution centers or directly to the farms. The working scene characteristics of the equipment make it adaptable to various industrial environments, from large-scale manufacturing facilities to smaller processing plants. The flexibility and scalability of the system allow it to be customized to meet the specific needs of different applications, ensuring optimal performance and cost-effectiveness. In summary, the potassium carbonate fertilizer pneumatic conveying equipment is a versatile and essential component in modern fertilizer handling operations, offering a reliable and efficient solution for various industrial applications.
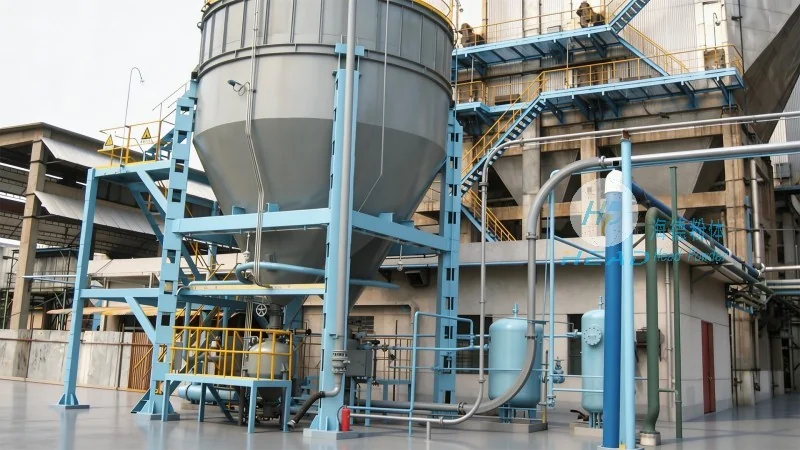
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable company specializing in the design and supply of advanced material handling systems, including pneumatic conveying equipment for potassium carbonate fertilizer. The company's expertise lies in providing customized solutions that meet the specific requirements of fertilizer manufacturers, ensuring high efficiency, reliability, and safety. The principles and working scene characteristics of the potassium carbonate fertilizer pneumatic conveying equipment, as discussed in this article, highlight the advanced technology and engineering capabilities of HeadPowder. The company's commitment to quality and innovation has enabled it to become a trusted partner in the fertilizer industry, offering solutions that enhance productivity and product quality. With a focus on customer satisfaction and long-term partnerships, HeadPowder continues to be at the forefront of material handling technology, providing reliable and efficient solutions for the fertilizer industry and beyond.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top