HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. The Negative Pressure Pneumatic Conveying System for Calcium Powder is a sophisticated piece of equipment engineered to efficiently transport calcium powder and similar fine powders in industrial settings. This system leverages negative pressure technology to create a controlled airflow that draws the powder from the source to the destination, ensuring minimal dust generation and high material recovery rates. The system is built with precision to meet the stringent requirements of calcium powder handling, incorporating high-efficiency dust collectors and flexible hose connections that adapt to various operational conditions. The negative pressure mechanism ensures that the conveying process is gentle on the powder particles, preserving their quality and preventing agglomeration. The design allows for easy integration into existing production lines, with modular components that can be customized to fit specific plant layouts and material flow requirements. Technical specifications include adjustable airflow rates, variable conveying distances, and robust material handling capabilities suitable for both small-scale and large-scale industrial applications.
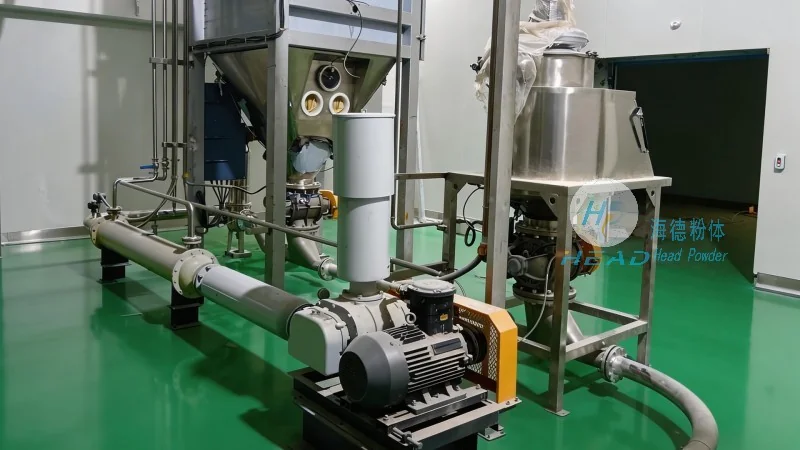
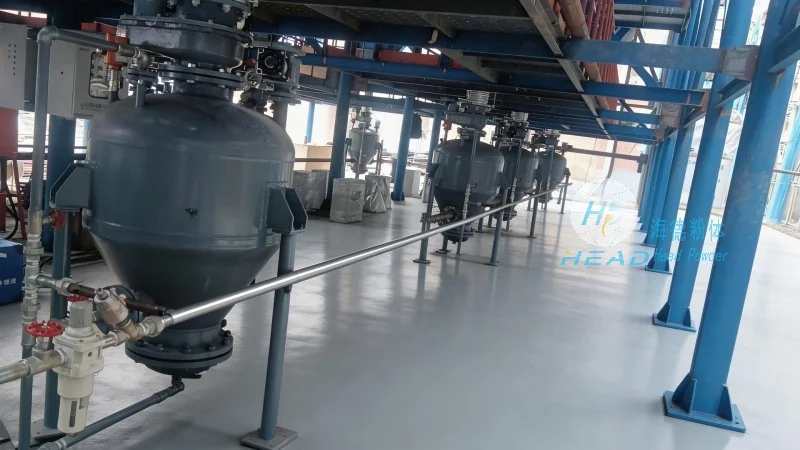
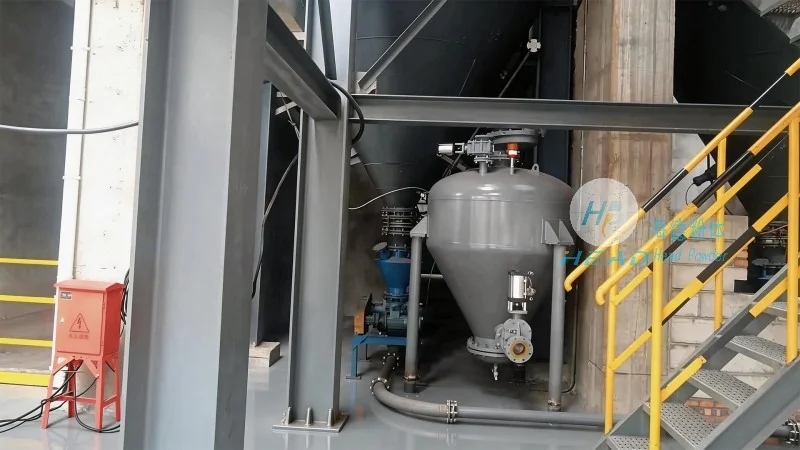
The system’s core features include a high-capacity vacuum pump that generates the necessary negative pressure, ensuring consistent airflow throughout the conveying process. The pump is equipped with a variable frequency drive (VFD) that allows for real-time adjustment of airflow speed, optimizing energy consumption based on the material being conveyed. The system also incorporates a series of filters and cyclones that separate the powder from the air, ensuring that the exhaust air is clean and compliant with environmental regulations. The hose and pipe network is constructed from corrosion-resistant materials, such as stainless steel or PVC, to withstand the chemical properties of calcium powder and prevent degradation over time. The control panel is user-friendly, with digital displays and intuitive controls that enable operators to monitor and adjust system parameters easily. The system’s modular design facilitates maintenance, as individual components can be replaced without disrupting the entire operation. Technical specifications further include a conveying capacity ranging from 0.5 to 10 tons per hour, depending on the system configuration, and a maximum conveying distance of up to 100 meters, with longer distances achievable through additional booster units.
One of the primary advantages of this system is its ability to operate under negative pressure, which significantly reduces the risk of dust contamination and environmental pollution. Unlike positive pressure systems, it does not release fine particles into the air, making it ideal for applications where air quality and worker safety are paramount. The system also offers high material recovery, typically exceeding 99% in most operational scenarios, which minimizes waste and improves overall efficiency. Additionally, the gentle handling of the powder particles helps maintain the product’s physical properties, such as particle size distribution and moisture content, which are critical for downstream processing. The low maintenance requirements and long service life of the components further contribute to the system’s cost-effectiveness, providing a reliable solution for long-term material handling needs. The system’s energy efficiency is another key benefit, as negative pressure operation consumes less power compared to positive pressure systems, resulting in lower operational costs and reduced carbon footprint. This makes it an environmentally friendly choice for industries committed to sustainable practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top