Calcium hydroxide, commonly known as slaked lime, is a widely used chemical in various industrial applications. The efficient and safe transportation of this material is crucial for many processes, and pneumatic conveying systems have emerged as a reliable solution. This article explores the fundamental principles behind calcium hydroxide pneumatic conveying equipment and highlights the key characteristics of its working scenarios.
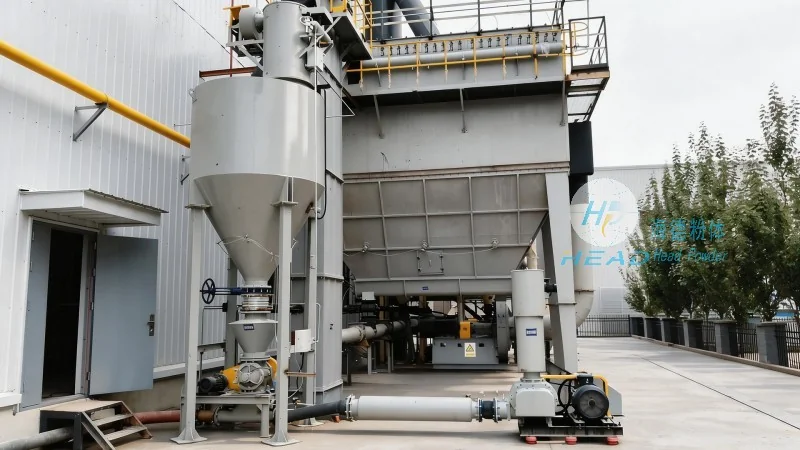
At the core of calcium hydroxide pneumatic conveying is the use of air or gas to transport bulk materials through a pipeline. The system typically consists of a hopper, a rotary valve, a conveyor pipe, and a receiver. The process begins when the material is fed into the hopper. A rotary valve then controls the flow of the material into the conveyor pipe. Compressed air is introduced into the pipe, creating a flow that carries the calcium hydroxide particles along with it. The velocity of the air is carefully managed to ensure that the particles are suspended and transported without causing excessive wear or degradation. The receiver at the end of the pipe collects the conveyed material, completing the cycle.
Several critical components contribute to the effective operation of calcium hydroxide pneumatic conveying equipment. The hopper serves as the storage and feeding unit, ensuring a consistent supply of material. The rotary valve acts as a gate, regulating the flow rate and preventing backflow. The conveyor pipe is designed to withstand the pressure and abrasion from the calcium hydroxide particles, often made from materials like stainless steel or high-density polyethylene. The air compressor provides the necessary pressure and volume of air to drive the conveying process. Finally, the receiver collects the material and may include features such as a dust filter to maintain air quality and prevent contamination.
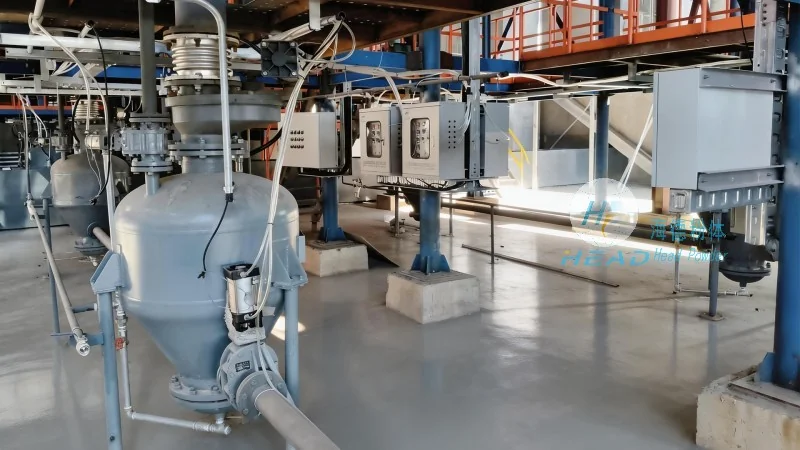
Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages for calcium hydroxide transportation. It is a closed system, which minimizes dust emissions and improves safety in the workplace. The lack of moving parts in the conveying line reduces maintenance requirements and operational downtime. Additionally, pneumatic systems can handle materials with varying particle sizes and moisture content, making them versatile for different applications. The ability to transport materials over long distances without the need for multiple transfer points also enhances efficiency and reduces the risk of material degradation.
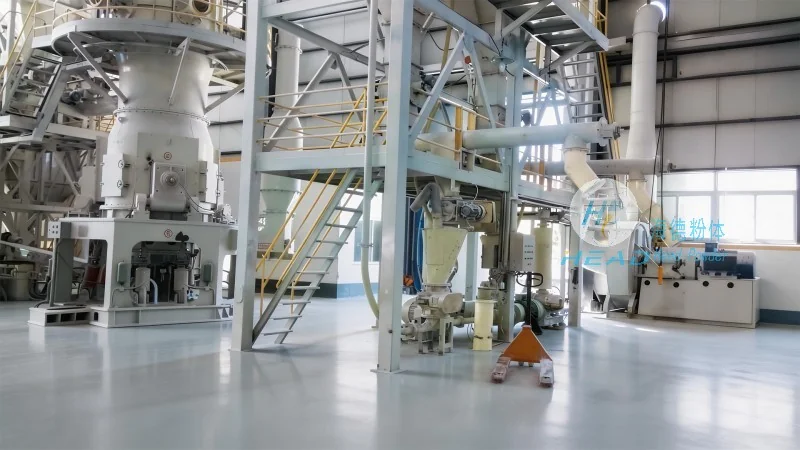
The working scene characteristics of calcium hydroxide pneumatic conveying equipment are tailored to specific industrial needs. In construction sites, for example, the equipment is used to transport slaked lime to mixing stations for concrete production. The closed system helps maintain the material's quality and prevents contamination from environmental factors. In chemical plants, the equipment is integrated into larger production lines, where calcium hydroxide is used as a raw material for various products. The working environment in these plants often involves high temperatures and corrosive substances, requiring the equipment to be durable and resistant to wear. In agricultural applications, the equipment may be used to distribute lime for soil treatment, where the system needs to be portable and easy to operate in outdoor settings. Each of these scenarios demands specific design considerations, such as the material of construction and the air pressure, to ensure optimal performance and safety.
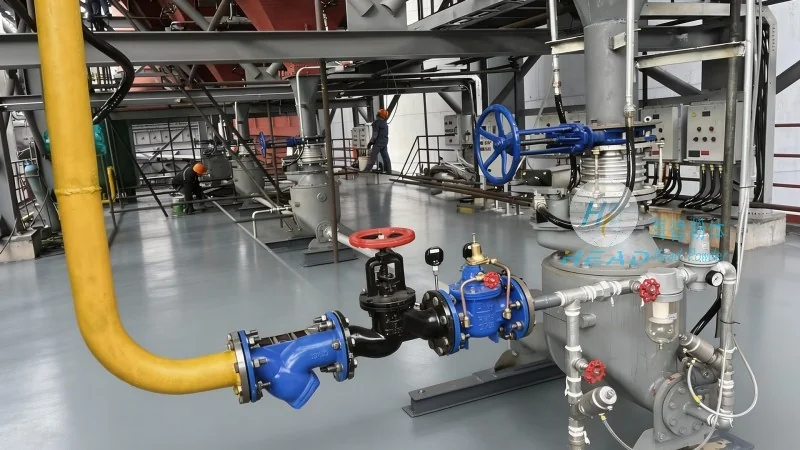
Calcium hydroxide pneumatic conveying equipment is applied in diverse industries, including construction, chemical manufacturing, and agriculture. In the construction industry, the equipment plays a vital role in the production of high-quality concrete, where the uniform distribution of lime is essential for strength and durability. The ability to convey large quantities of material quickly and efficiently supports the high demand for construction materials. In the chemical industry, the equipment is used in the production of lime-based products, such as calcium chloride and calcium carbonate. The consistent supply of calcium hydroxide ensures the quality and consistency of these end products. In agriculture, the equipment helps in the application of lime for soil pH adjustment, which improves soil fertility and crop yields. The efficiency of the pneumatic system allows for large-scale application, making it suitable for both commercial and industrial farming operations.
Calcium hydroxide pneumatic conveying equipment is a sophisticated solution for the efficient and safe transportation of this essential chemical. By understanding the working principles and characteristics of these systems, industries can optimize their processes and enhance productivity. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of such equipment. With a focus on quality and innovation, the company provides tailored solutions that meet the specific needs of various applications. The company's commitment to using durable materials and advanced technology ensures that their pneumatic conveying systems deliver reliable performance and long-term value. For industries requiring efficient calcium hydroxide transportation, Shandong HeadPowder Engineering Co., Ltd. offers a trusted partner in achieving their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top