Calcium carbonate powder, a widely used industrial material, requires efficient and reliable transportation methods to ensure smooth production processes. Pneumatic conveying equipment has emerged as a key solution for handling such powders, offering advantages in terms of hygiene, speed, and flexibility. This article explores the fundamental principles behind calcium carbonate powder pneumatic conveying systems and highlights the specific characteristics of their working scenes, providing insights into how these technologies enhance operational efficiency in industrial settings.
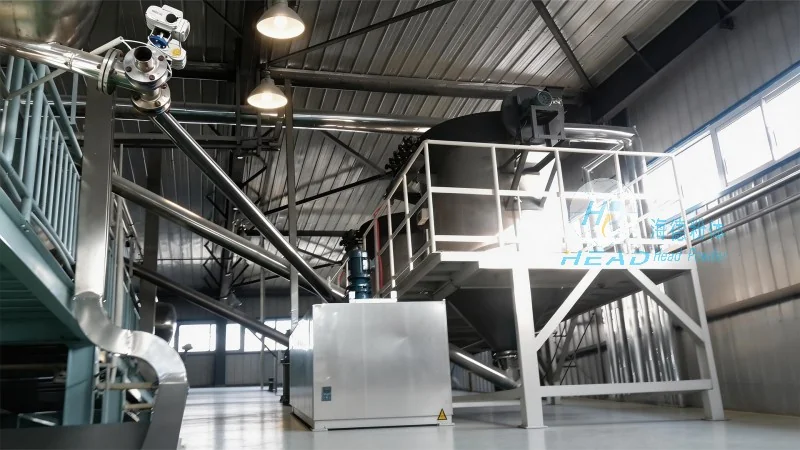
HeadPowder, a leading provider in the field, specializes in engineering and manufacturing advanced pneumatic conveying solutions. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality equipment tailored to the unique needs of industries dealing with calcium carbonate powders. The company's commitment to innovation and customer satisfaction has positioned it as a trusted partner for businesses seeking efficient material handling systems.
Pneumatic conveying systems operate by transporting solid particles, such as calcium carbonate powder, through a pipeline using air or gas. The core principle involves creating a pressure differential that propels the powder along the conveying line. There are two primary types of pneumatic conveying: positive pressure and negative pressure systems. Positive pressure systems use a blower to generate high-pressure air that pushes the powder through the pipeline, while negative pressure systems employ a vacuum to draw the powder from the source into the system. For calcium carbonate powders, positive pressure systems are often preferred due to their ability to handle abrasive materials and maintain consistent flow rates. The equipment typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver to collect the material at the destination. The selection of the appropriate system depends on factors such as the powder's characteristics, the distance to be conveyed, and the required flow rate.
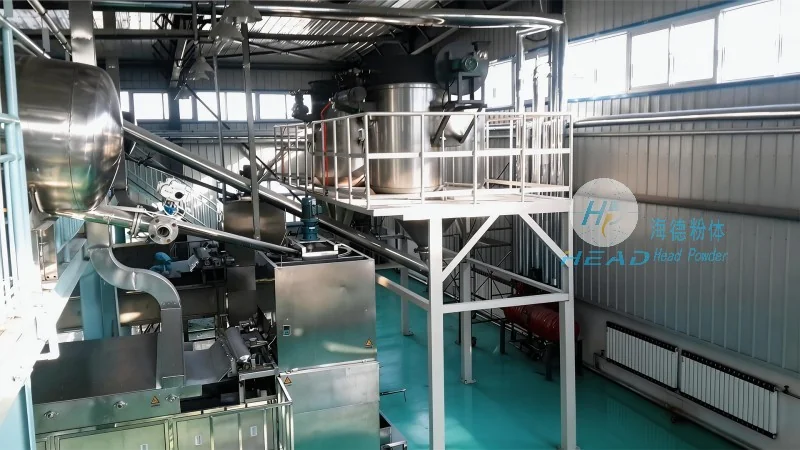
The working scenes where calcium carbonate powder pneumatic conveying equipment is applied vary widely, reflecting the diverse applications of this material in industries like paper, plastics, coatings, and food processing. In the paper industry, for instance, calcium carbonate is used as a filler to improve paper quality and reduce costs. The pneumatic conveying system must be capable of handling large volumes of powder over considerable distances, often from storage silos to the paper mill's processing units. This requires robust equipment that can maintain high flow rates without clogging, as the powder may have a tendency to agglomerate. In the plastics industry, calcium carbonate is added to polymer resins to enhance mechanical properties and reduce material costs. The conveying system must be designed to integrate seamlessly with existing production lines, ensuring minimal downtime and consistent material supply. The working environment may involve high temperatures or exposure to chemicals, necessitating equipment made from corrosion-resistant materials. In the coatings industry, calcium carbonate is used as a pigment or filler to adjust the opacity and texture of coatings. The pneumatic conveying system must maintain the powder's quality, preventing contamination or degradation during transport. This often involves using closed systems to avoid dust exposure and ensure product purity. In the food industry, calcium carbonate is used as a dietary supplement or as a filler in certain food products. The conveying equipment must meet stringent hygiene standards, with components made from food-grade materials and designed for easy cleaning. The system must also be able to handle fine powders without generating excessive dust, which is critical for maintaining product safety and regulatory compliance.
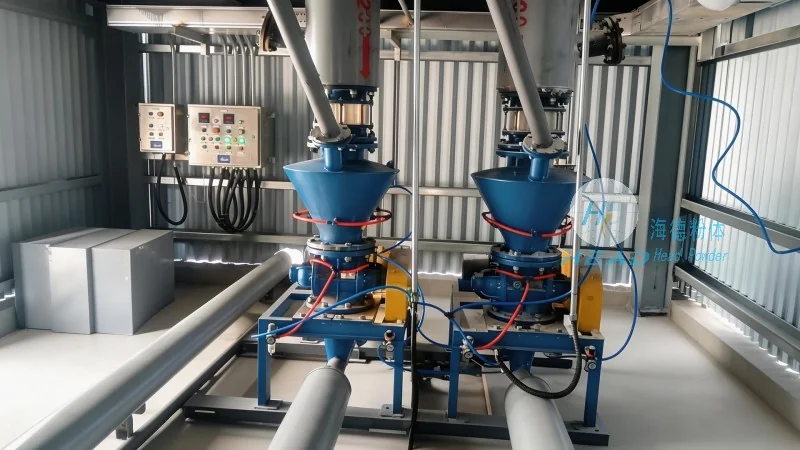
Each working scene presents unique challenges and benefits for calcium carbonate powder pneumatic conveying equipment. The advantages of these systems include improved hygiene, as they eliminate the need for manual handling and reduce dust exposure. This is particularly important in industries where product purity is paramount, such as food and pharmaceuticals. Additionally, pneumatic conveying offers faster material transport compared to traditional methods like trucks or conveyor belts, leading to increased production efficiency. The flexibility of these systems allows for easy integration into existing production lines, enabling businesses to adapt to changing production demands. However, there are also considerations to keep in mind. For example, the cost of equipment and maintenance can be higher compared to other transport methods. The system's performance may be affected by the powder's moisture content or particle size, requiring regular maintenance to prevent clogging or wear. In some cases, the distance to be conveyed or the volume of material may limit the effectiveness of a particular system type. HeadPowder's expertise in customizing solutions helps address these challenges, ensuring that the chosen equipment meets the specific requirements of each working scene.
In conclusion, calcium carbonate powder pneumatic conveying equipment plays a vital role in enhancing the efficiency and safety of industrial processes. The principles behind these systems, combined with the specific characteristics of their working scenes, provide a comprehensive solution for handling calcium carbonate powders. HeadPowder's commitment to quality and innovation ensures that businesses can rely on these systems to meet their material handling needs. By understanding the principles and working scene characteristics, industries can make informed decisions when selecting pneumatic conveying equipment, ultimately improving their operational performance and competitiveness.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top