Barley pellet pneumatic conveying technology represents a sophisticated method for transporting barley pellets, a key ingredient in the brewing industry. This technology utilizes air as the conveying medium to move the pellets from one location to another, offering advantages such as reduced contamination risk, improved hygiene, and enhanced operational efficiency. The core principle involves creating a pressure differential that propels the pellets through a pipeline using compressed air or vacuum systems. This approach is particularly beneficial in environments where maintaining product purity and preventing cross-contamination is critical, such as in modern breweries and malting facilities.
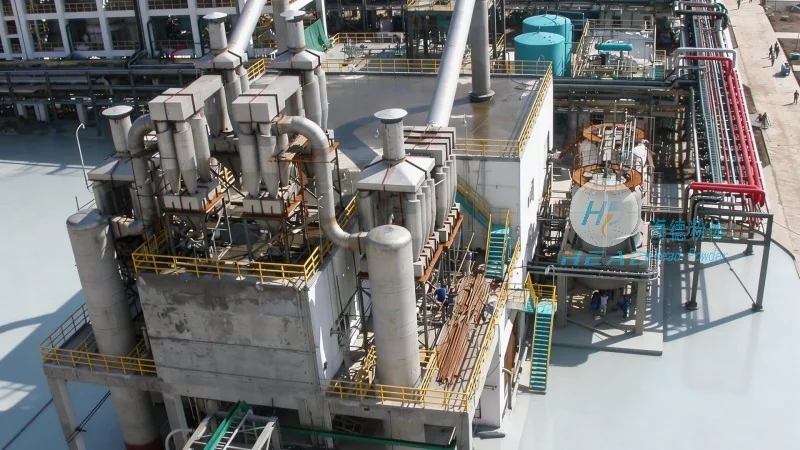
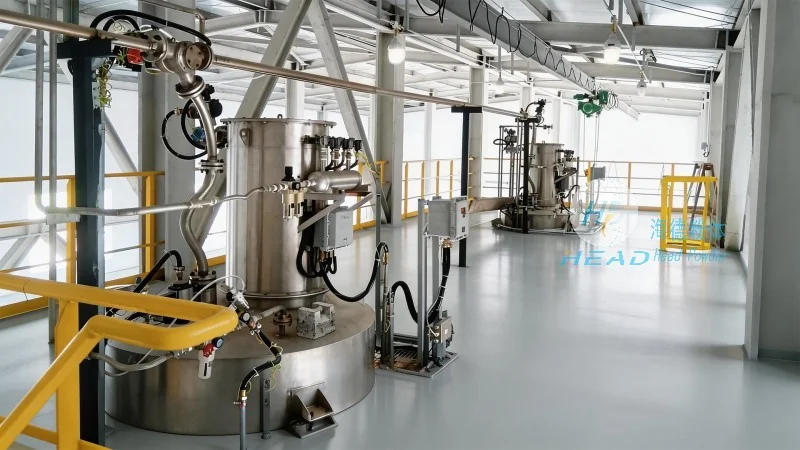
The fundamental principles of pneumatic conveying for barley pellets revolve around the interaction between the pellets and the air stream. There are two primary modes: dilute-phase and dense-phase conveying. Dilute-phase systems operate at higher air velocities, typically moving pellets in a dispersed state, while dense-phase systems use lower velocities to transport pellets in a more compact, plug-like flow. The choice between these modes depends on factors like pellet size, moisture content, and the distance to be covered. For barley pellets, which are relatively uniform in size and have moderate moisture levels, dilute-phase systems are often preferred for longer distances due to their efficiency and lower energy consumption. The conveying process begins with the pellets being fed into a hopper or feeder, where they are then introduced into the pipeline. The air is introduced at the inlet, creating a flow that carries the pellets forward. The system may include components like cyclones or filters to separate the pellets from the air at the discharge point, ensuring that the product is collected cleanly and efficiently.
HeadPowder, a leading provider of engineering solutions for the food and beverage sector, utilizes pneumatic conveying technology in various applications within the malting and brewing industry. One primary application is the transfer of barley pellets from storage silos to the mashing tanks in breweries. This process ensures that the barley is moved hygienically and without the need for manual handling, reducing the risk of contamination and improving overall operational safety. Another key application is the conveying of malted barley from the malting floor to processing equipment, such as grinders or mixers. The technology also supports the transport of barley pellets between different stages of the production line, such as from the drying and cooling sections to the packaging area. In addition, pneumatic conveying is used in quality control processes, where pellets are sampled and analyzed for moisture content, particle size, and other critical parameters. The technology's ability to handle bulk materials with minimal human intervention makes it an essential component in modern, high-throughput malting and brewing operations.
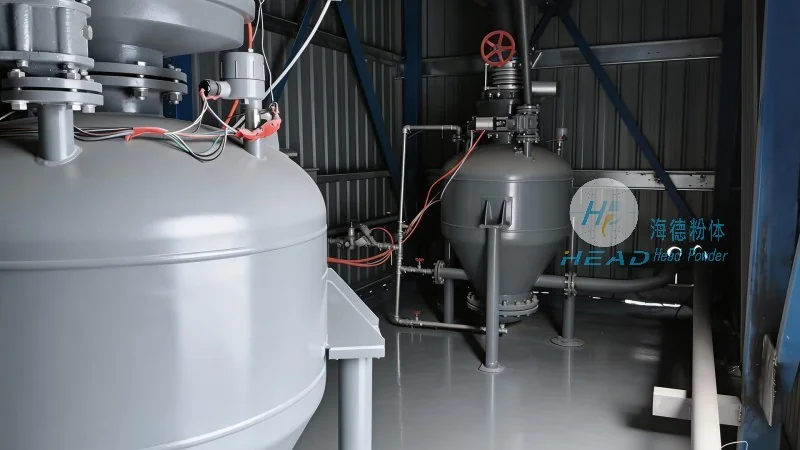
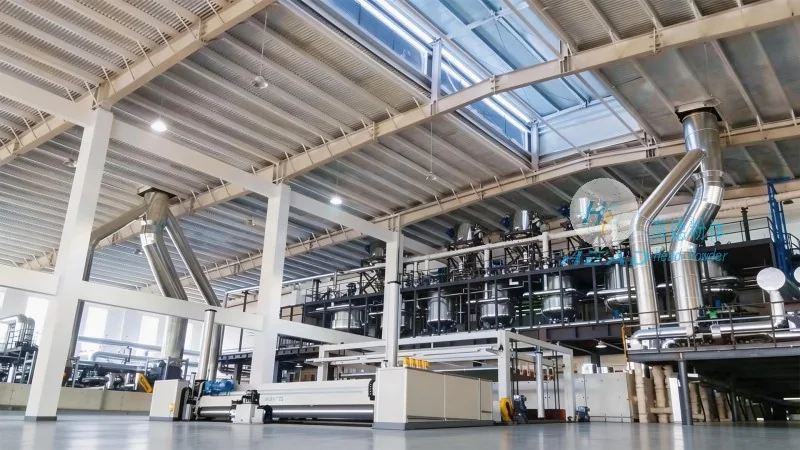
Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveying offers several distinct advantages for handling barley pellets. First, it provides a closed system that prevents dust and contaminants from entering the environment, which is crucial for maintaining product quality and compliance with food safety regulations. The enclosed pipeline also reduces the risk of product degradation due to exposure to air or moisture. Second, the technology allows for flexible and scalable system designs, enabling the integration of conveying lines into existing production facilities without major structural modifications. This adaptability is particularly valuable in breweries and malting plants that may need to expand or reconfigure their operations over time. Third, pneumatic conveying systems can be automated with minimal human intervention, improving labor efficiency and reducing the risk of operational errors. The use of sensors and control systems ensures that the conveying process is optimized for speed and energy consumption, leading to cost savings over time. Additionally, the technology is suitable for handling a wide range of barley pellet sizes and moisture contents, making it a versatile solution for various production requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top