HeadPowder Engineering, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying systems tailored for various bulk materials, including coke pellets. This article provides a detailed comparison of positive pressure and negative pressure conveying methods, focusing on their applications, operational principles, and key performance characteristics to help industries make informed decisions when selecting the most suitable conveying technology for their operations.
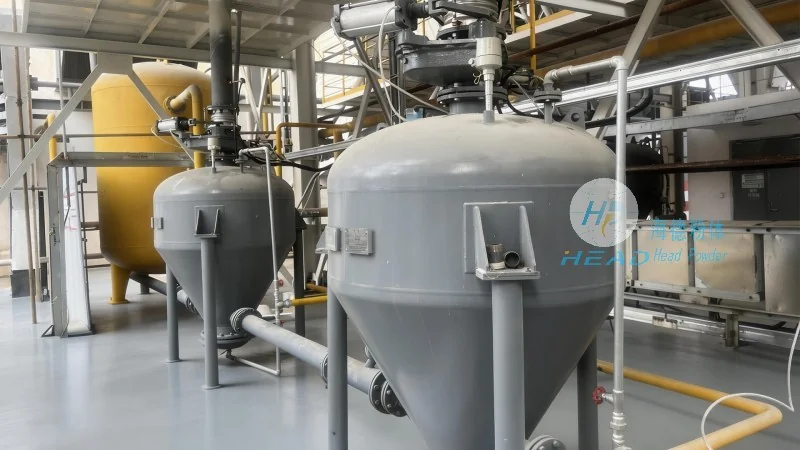
Pneumatic conveying is a widely used technique for transporting bulk solids like coke pellets over short to medium distances. It offers advantages such as reduced mechanical wear, lower maintenance costs compared to traditional belt or screw conveyors, and the ability to handle materials in a dust-free environment. The two primary methods of pneumatic conveying are positive pressure and negative pressure systems, each with distinct operational principles and suitability for different industrial scenarios.
Positive pressure conveying operates by blowing air or a gas mixture into the conveying line, creating a pressure higher than the ambient air pressure. This method propels the coke pellets through the pipeline using a positive pressure source, typically a blower or a positive displacement pump. The system is designed to move material from a source to a destination, with the air flow direction being from the pressure source towards the discharge point.
Key features of positive pressure systems include high conveying capacity, the ability to handle abrasive or corrosive materials, and the flexibility to operate over longer distances. These systems are often preferred in applications where the material is to be delivered to a specific location, such as a storage silo or a processing unit. The positive pressure approach ensures that the material is continuously pushed through the pipeline, minimizing the risk of blockages and ensuring consistent flow rates.
However, positive pressure conveying also has limitations. It may require more robust equipment to handle high pressures, and the system can be more complex to install and maintain, especially in environments with strict air quality regulations. Additionally, the higher air velocity and pressure can lead to increased energy consumption, making it less economical for certain low-volume or short-distance applications.
Negative pressure conveying, also known as vacuum conveying, works by creating a vacuum in the conveying line, which draws the coke pellets from the source into the system. The vacuum is generated by a vacuum pump or a fan, and the material is pulled through the pipeline towards the vacuum source. This method is particularly effective for handling fine or dusty materials and for conveying materials from multiple points to a central collection point.
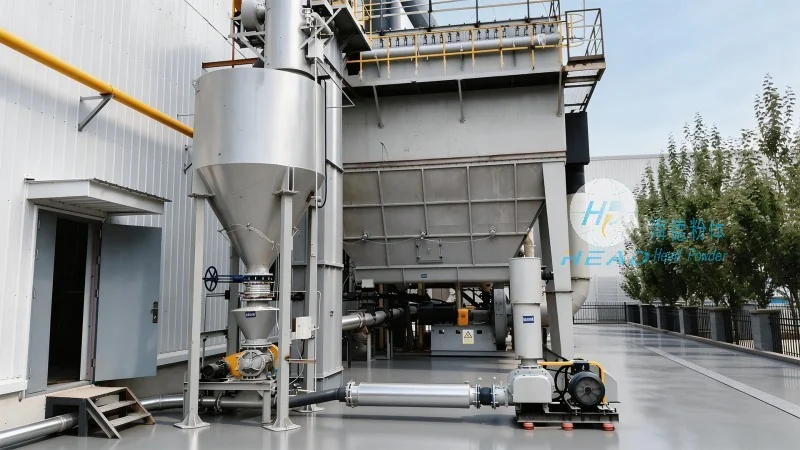
One of the main advantages of negative pressure systems is their ability to handle materials with high moisture content or those that are prone to dust generation. The vacuum environment helps to minimize dust emissions and maintain a cleaner working environment. Negative pressure conveying is also suitable for applications where the material needs to be collected from a dispersed source, such as a stockpile or a hopper, and transported to a processing facility.
Despite these benefits, negative pressure systems have their drawbacks. They are generally less efficient for high-volume or long-distance conveying, as the vacuum can lead to lower material flow rates and increased energy consumption. The system is also more susceptible to blockages if the material contains large particles or is prone to agglomeration. Furthermore, the vacuum pump requires regular maintenance to ensure optimal performance and to prevent dust accumulation, which can affect the overall efficiency of the system.
When comparing positive and negative pressure conveying for coke pellets, several factors must be considered, including the distance of the conveying line, the volume of material to be transported, the characteristics of the material (e.g., particle size, moisture content, abrasiveness), and the environmental regulations in the operating area. Positive pressure systems are typically more suitable for longer distances and higher material volumes, while negative pressure systems excel in applications requiring dust control and material collection from multiple points.
From an operational perspective, positive pressure systems offer higher conveying rates and are less prone to blockages, making them ideal for continuous production lines. Negative pressure systems, on the other hand, provide better dust control and are more flexible in handling materials with high moisture content or fine particles. The choice between the two methods often depends on the specific requirements of the industrial process and the cost-effectiveness of each approach.
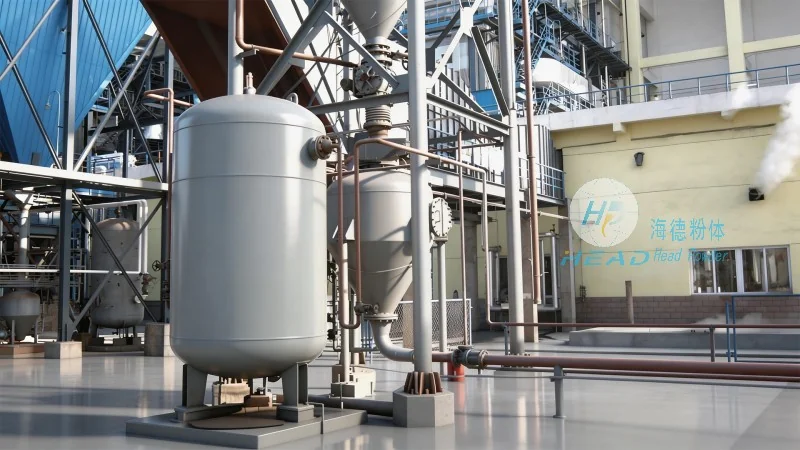
For industries dealing with coke pellets, the selection of a pneumatic conveying system depends on the operational environment and the specific handling requirements. Positive pressure systems are commonly used in steel plants and coke production facilities where large volumes of coke need to be transported from the production line to storage silos or processing units. These systems are designed to handle the high abrasiveness of coke pellets and ensure reliable operation over extended periods.
Negative pressure systems are often employed in applications where dust control is a critical factor, such as in facilities that require a clean working environment or where the material is to be collected from a stockpile and transported to a processing plant. The vacuum nature of the system helps to minimize dust emissions, making it suitable for environments with strict air quality standards.
Another important consideration is the maintenance and operational costs associated with each system. Positive pressure systems may require more frequent maintenance of the blower and pipeline components due to the higher pressure and air flow, while negative pressure systems may need more attention to the vacuum pump and filtration systems to prevent dust buildup. The initial investment and long-term operational costs should be evaluated carefully when choosing between the two methods.
In conclusion, both positive pressure and negative pressure pneumatic conveying methods offer viable solutions for transporting coke pellets, each with its own set of advantages and limitations. Positive pressure systems are generally more efficient for high-volume and long-distance conveying, while negative pressure systems excel in dust control and material collection from multiple sources. The optimal choice depends on the specific application requirements, material characteristics, and operational constraints of the industrial facility.
HeadPowder Engineering provides customized pneumatic conveying solutions tailored to the unique needs of each client, ensuring that the selected system meets the performance, efficiency, and environmental standards required for coke pellet handling. By understanding the operational principles and comparative analysis of these two methods, industries can make informed decisions to enhance their material handling processes and improve overall operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top