Alumina hydroxide, a key chemical compound widely used in various industrial applications such as ceramics, refractory materials, and pharmaceuticals, often requires efficient and reliable material handling solutions. The Alumina Hydroxide Powder Pneumatic Conveying System is a specialized equipment designed to transport this fine powder from one location to another within industrial facilities. This system leverages the principles of pneumatic conveying, where air or gas is used to move the powder through a pipeline network, ensuring safe and effective material transfer without the need for mechanical components that might cause contamination or wear.
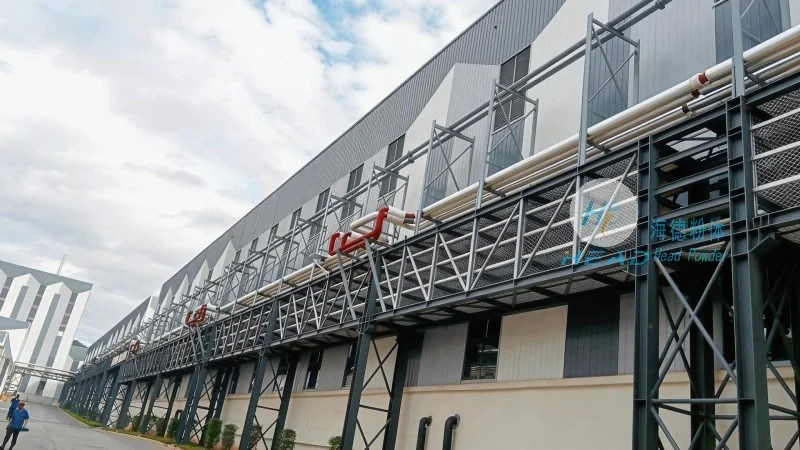
The primary purpose of this system is to facilitate the transport of alumina hydroxide powder in a controlled manner. Unlike traditional bulk material handling methods like belt conveyors or screw conveyors, pneumatic conveying offers advantages such as reduced risk of product contamination, lower maintenance requirements, and the ability to handle materials that are sensitive to moisture or air exposure. The system typically consists of a feeding hopper, a blower or compressor to generate the conveying air, a pipeline network, and a discharge unit. The feeding hopper ensures a consistent supply of powder, while the blower provides the necessary air pressure to move the particles through the pipeline. The pipeline network is designed to minimize pressure drop and ensure smooth flow, often incorporating bends, valves, and filters to maintain system efficiency and prevent blockages.
The design of an alumina hydroxide powder pneumatic conveying system is governed by several critical principles that ensure optimal performance and reliability. One of the fundamental design considerations is the selection of the appropriate air velocity and pressure. The air velocity must be high enough to overcome the gravitational forces acting on the powder particles and to prevent settling or clogging in the pipeline. However, excessive air velocity can lead to increased energy consumption and potential damage to the system components. Therefore, a balance is struck between air velocity and pressure to achieve efficient conveying while minimizing operational costs. Another crucial design principle is the sizing and configuration of the pipeline. The diameter and length of the pipeline are determined based on the material's properties, such as particle size, density, and flowability. For fine powders like alumina hydroxide, smaller pipeline diameters are often used to maintain a high air-to-solid ratio, which enhances conveying efficiency. Additionally, the system may incorporate features like pulse-jet or rotary airlock valves to regulate the flow and prevent material buildup at critical points.
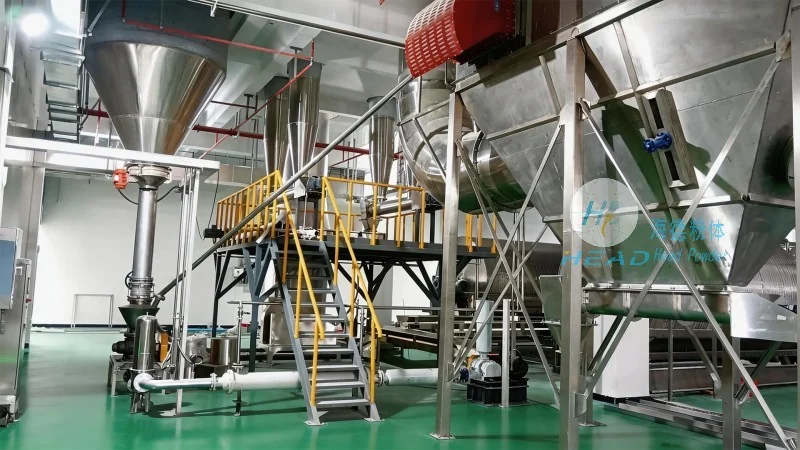
Each component of the Alumina Hydroxide Powder Pneumatic Conveying System plays a vital role in ensuring its smooth operation. The feeding hopper is responsible for storing and feeding the powder into the system, often equipped with a rotary valve or a screw feeder to control the flow rate. The blower or compressor generates the necessary air pressure, with options ranging from positive displacement blowers to centrifugal compressors, depending on the system's requirements. The pipeline network connects the feeding and discharge points, and its design must account for the material's behavior under pressure and flow. The discharge unit, which may include a rotary valve or a venturi, controls the release of the powder at the destination, preventing backflow and ensuring a clean discharge. Filters and cyclones are also integral components, as they help remove any dust or particles from the conveying air, protecting downstream equipment and maintaining air quality.
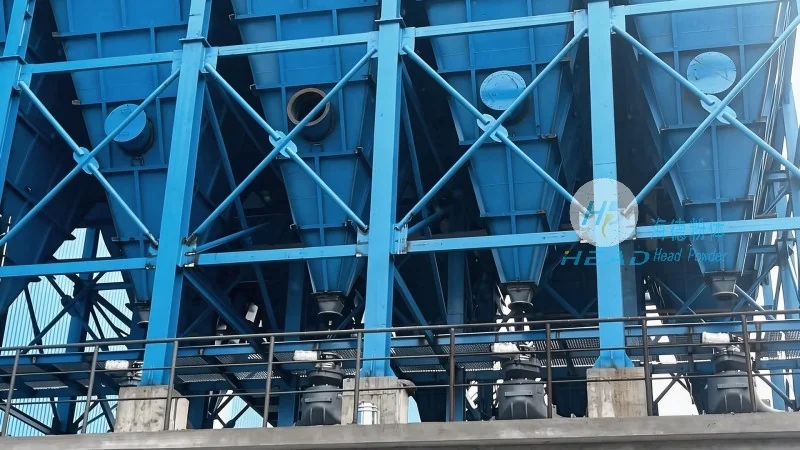
The Alumina Hydroxide Powder Pneumatic Conveying System is widely utilized in industries where the handling of fine powders is essential. In the ceramics industry, for example, it is used to transport alumina hydroxide to production lines, ensuring consistent quality and reducing downtime. In the pharmaceutical sector, the system's ability to maintain product purity and prevent contamination makes it suitable for handling active pharmaceutical ingredients (APIs) that require stringent handling protocols. The benefits of this system extend beyond material handling; it also contributes to improved safety in industrial environments by eliminating the need for manual handling of powders, which can pose health risks such as respiratory issues. Furthermore, the system's compact design allows for integration into existing facilities, minimizing space requirements and reducing installation costs.
Headpowder, the manufacturer of the Alumina Hydroxide Powder Pneumatic Conveying System, is a leading company in the field of powder handling solutions. With its headquarters in Shandong, China, Headpowder has established itself as a trusted provider of industrial equipment tailored to meet the specific needs of various industries. The company specializes in designing and manufacturing customized pneumatic conveying systems that are optimized for different powder types, including alumina hydroxide. Its team of engineers and technicians works closely with clients to understand their operational requirements and develop solutions that enhance efficiency, reduce costs, and improve product quality. Headpowder's commitment to quality and innovation has made it a preferred choice for businesses seeking reliable and efficient material handling systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top