HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design and production of industrial pneumatic conveying systems. This article will explore the concept of a nitrile rubber pneumatic conveying system and delve into its fundamental design principles, providing a comprehensive overview for those interested in this technology.
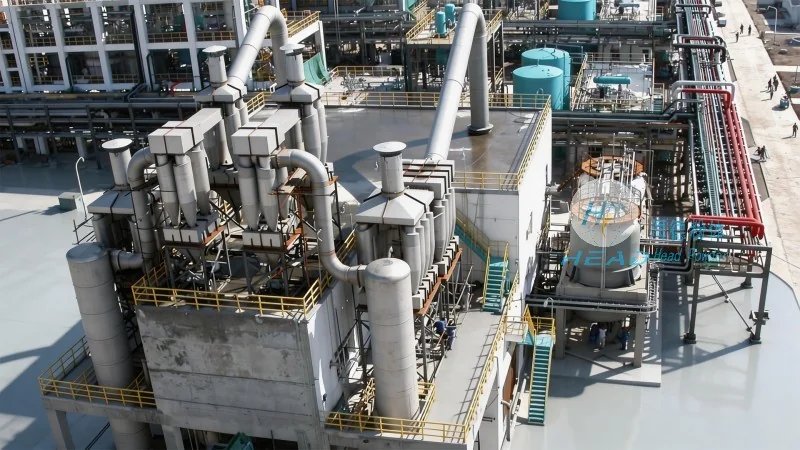
A nitrile rubber pneumatic conveying system is a type of equipment used to transport bulk materials through a pipeline using compressed air or other gases. The system typically consists of a hopper, a rotary valve, a conveying line, and a receiver. The key component that differentiates this system from others is the use of nitrile rubber, which offers excellent resistance to oil, fuel, and other chemicals, making it ideal for handling materials that are corrosive or abrasive.
The design of a nitrile rubber pneumatic conveying system is based on several critical principles to ensure efficient and reliable material transport. First, the system must be designed to handle the specific properties of the material being conveyed, such as its density, particle size, and moisture content. The choice of nitrile rubber for the pipeline and components is crucial as it provides durability and resistance to the chemicals present in the material. Second, the system must maintain a consistent air pressure and flow rate to prevent blockages and ensure smooth material movement. This is achieved through the use of appropriate air compressors and control valves. Third, the system should incorporate safety features, such as pressure relief valves and explosion-proof components, to protect against potential hazards. Additionally, the design must consider the overall system layout, including the length and number of bends in the pipeline, to minimize pressure drop and energy consumption.
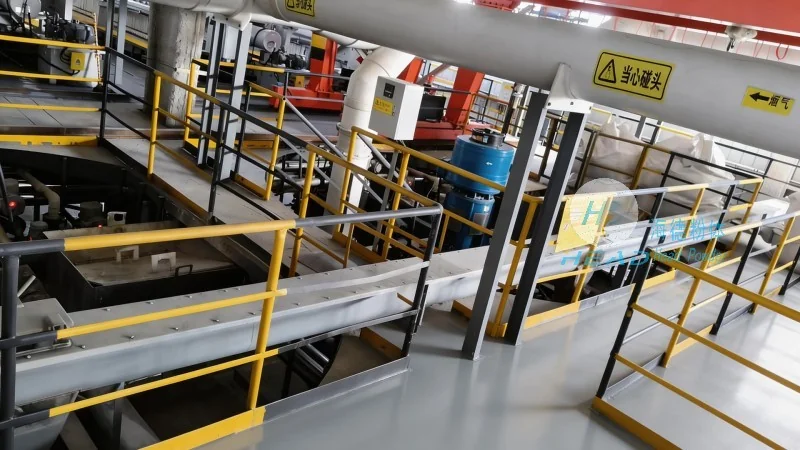
Several key components make up a nitrile rubber pneumatic conveying system, each playing a vital role in the overall operation. The hopper is the initial storage container where the bulk material is loaded. It is equipped with a feeding device, such as a rotary valve, which controls the flow of material into the conveying line. The rotary valve acts as a gate, allowing material to enter the system at a controlled rate, preventing overloading and ensuring smooth operation. The conveying line, made from nitrile rubber, is the main pathway for the material and air mixture. The material is carried by the air stream, which is generated by the air compressor. The receiver is the final storage container where the material is deposited after being conveyed through the pipeline. The system may also include additional components, such as filters and cyclones, to separate the material from the air and prevent contamination.
There are several advantages to using a nitrile rubber pneumatic conveying system for material transport. One of the primary benefits is the ability to handle a wide range of materials, including those that are corrosive, abrasive, or sensitive to moisture. The nitrile rubber material is highly resistant to these conditions, ensuring the longevity of the system. Another advantage is the system's ability to transport materials over long distances and through multiple bends without significant loss of material or air pressure. This makes it suitable for applications where traditional conveying methods, such as belt conveyors or bucket elevators, are not feasible. Additionally, the system is relatively compact and can be installed in tight spaces, making it ideal for industrial settings with limited floor space. Finally, the system operates with minimal maintenance, as the nitrile rubber components are durable and resistant to wear and tear.
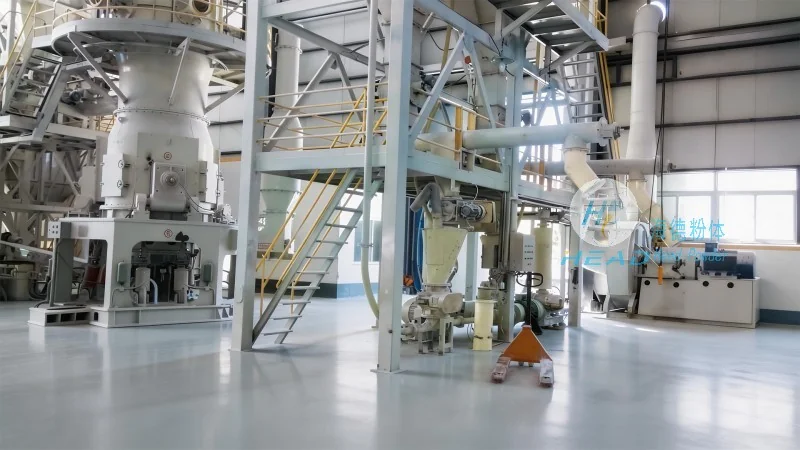
Nitrile rubber pneumatic conveying systems are widely used in various industries, including chemical, pharmaceutical, food, and manufacturing. In the chemical industry, the system is used to transport chemicals that are corrosive or flammable, where the nitrile rubber components provide the necessary resistance. In the pharmaceutical industry, the system is used to transport powders and granules that require a sterile and clean environment, as the nitrile rubber is easy to clean and maintain. In the food industry, the system is used to transport food products that are sensitive to moisture or temperature changes, as the nitrile rubber is non-toxic and hygienic. In manufacturing, the system is used to transport raw materials and finished products, improving efficiency and reducing labor costs.
In conclusion, a nitrile rubber pneumatic conveying system is a versatile and efficient method for transporting bulk materials. The design principles, which focus on material compatibility, air pressure control, and safety features, ensure the system operates reliably and effectively. The use of nitrile rubber components provides durability and resistance to various chemicals, making the system suitable for a wide range of applications. As a professional manufacturer based in Shandong, China, HeadPowder Engineering Co., Ltd. offers high-quality nitrile rubber pneumatic conveying systems that meet the needs of various industries. Whether you are in the chemical, pharmaceutical, food, or manufacturing sector, a nitrile rubber pneumatic conveying system from HeadPowder can help improve your material handling processes and increase productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top