Introduction to Malt Powder Conveying Systems: Structure and Working Principles
Release time:2026-09-22 04:01:32
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., specializes in the design and manufacturing of advanced malt powder conveying systems. Based in Shandong, China, the company has established itself as a key player in providing efficient and reliable solutions for the malt processing industry. This article provides an overview of the malt powder conveying system, detailing its structural components and operational principles.
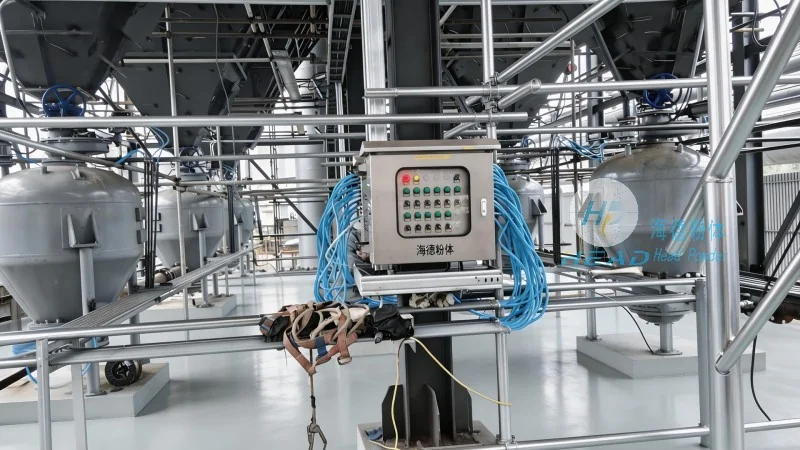
Overview of Malt Powder Conveying Systems
Malt powder conveying systems are essential equipment in the malt production and processing sector. These systems are engineered to handle malt powder efficiently, ensuring minimal loss, contamination, and energy consumption. The primary goal is to transport malt powder from storage silos or processing units to various stages of the production line, such as milling, mixing, or packaging. HeadPowder's systems are designed to meet the specific needs of malt producers, offering customizable solutions that enhance productivity and maintain product quality.
Key Structural Components of the Malt Powder Conveying System
The malt powder conveying system consists of several critical components that work in tandem to ensure smooth operation. These components include:
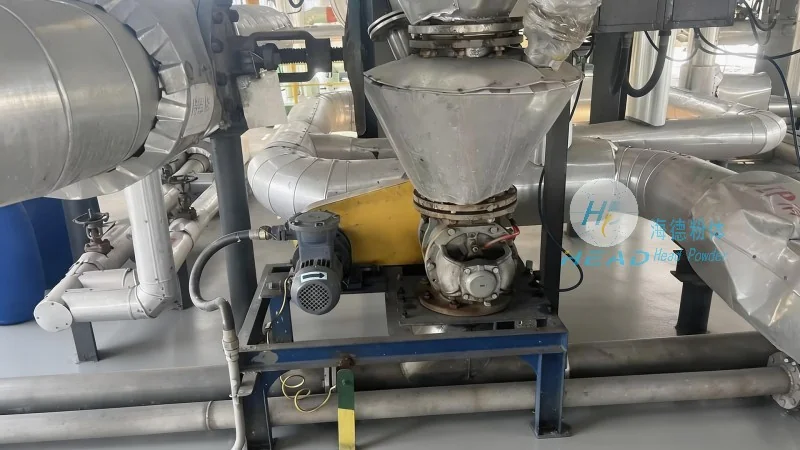
- Feeding Hopper: The feeding hopper is the initial component that receives malt powder from storage. It is designed with a sloped bottom to facilitate the flow of powder into the conveyor system. The hopper is typically made of stainless steel to prevent contamination and ensure durability.
- Pneumatic Conveying Lines: Pneumatic conveying is a core technology used in HeadPowder's systems. This method uses compressed air to transport malt powder through a network of pipes. The system includes air locks, which are crucial for maintaining pressure and preventing backflow. The design of the conveying lines is optimized to minimize particle degradation and ensure consistent flow rates.
- Rotary Valves: Rotary valves are used at the inlet and outlet of the conveying system to control the flow of malt powder. These valves are equipped with sealing mechanisms to prevent air leakage and maintain the integrity of the powder. They are designed to handle high volumes of powder while maintaining low maintenance requirements.
- Control Panel: The control panel is the central hub for operating the conveying system. It allows operators to monitor and adjust parameters such as air pressure, flow rate, and system speed. The panel is equipped with safety features to prevent accidents and ensure compliance with industry standards.
Working Principles of the Malt Powder Conveying System
The operation of the malt powder conveying system is based on the principles of pneumatic transport. When the system is activated, compressed air is introduced into the feeding hopper, creating a low-pressure zone. This pressure differential causes the malt powder to be drawn into the conveying lines. The powder is then transported through the pipes to the destination point, such as a mixing tank or packaging unit. The system uses a combination of positive and negative pressure to control the flow and ensure efficient transport.
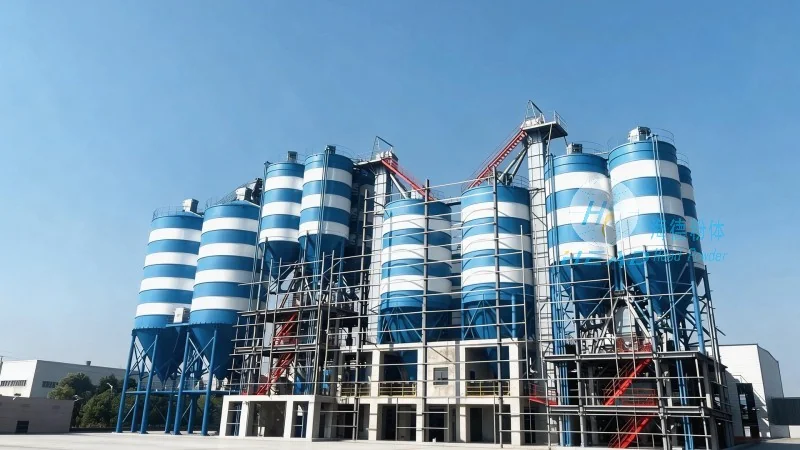
Advantages of HeadPowder's Malt Powder Conveying Systems
HeadPowder's malt powder conveying systems offer several advantages over traditional conveying methods. These include:
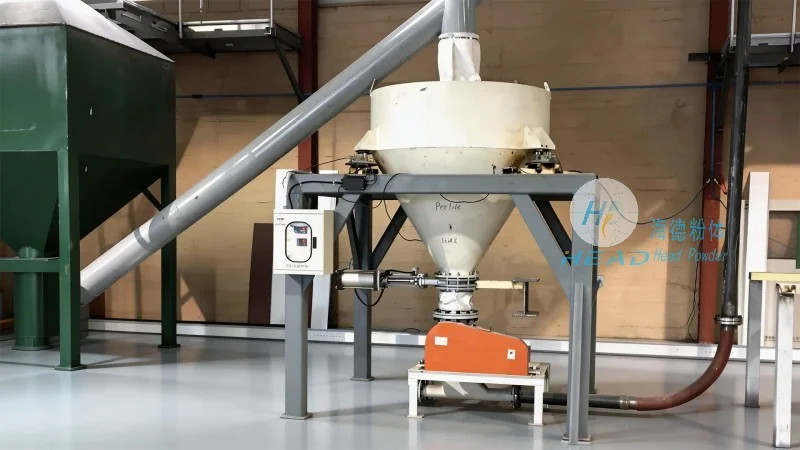
- High Efficiency: The systems are designed to handle high volumes of malt powder with minimal energy consumption. The use of pneumatic conveying reduces the need for mechanical components, leading to lower maintenance costs.
- Low Product Loss: The system's design minimizes product loss during transport. The use of air locks and rotary valves ensures that only the intended amount of powder is transferred, reducing waste.
- Improved Product Quality: The gentle handling of malt powder by the system prevents particle degradation and maintains the quality of the final product. This is crucial for malt producers who need to ensure consistent product quality.
- Customizable Solutions: HeadPowder offers customized solutions tailored to the specific needs of each client. The systems can be adjusted to handle different types of malt powder and accommodate varying production volumes.
Applications in the Malt Industry
Malt powder conveying systems are widely used in various stages of the malt production process. Some common applications include:
- From Storage to Milling: The system transports malt powder from storage silos to the milling equipment, ensuring a steady supply of raw material.
- Between Processing Stages: The system moves malt powder between different processing units, such as from milling to mixing or from mixing to packaging.
- Packaging: The system delivers malt powder to packaging machines, ensuring accurate and consistent filling of bags or containers.
Conclusion
HeadPowder's malt powder conveying systems are a reliable and efficient solution for the malt processing industry. By understanding the structural components and working principles of these systems, malt producers can make informed decisions about their equipment choices. The company's commitment to quality and customization ensures that clients receive systems that meet their specific needs and enhance their overall production efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
