HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced fertilizer pneumatic conveying equipment. This article delves into the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern agricultural and industrial applications.
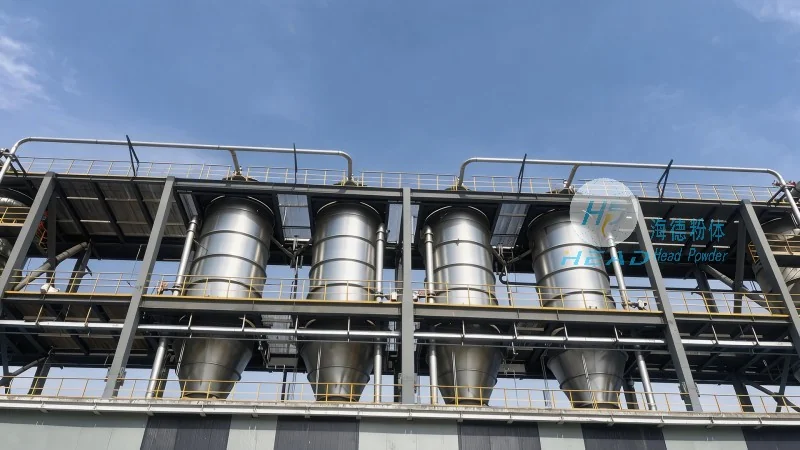
The core principle of fertilizer pneumatic conveying systems revolves around the use of air as the primary medium to transport bulk materials, such as granular or powdered fertilizers, from one location to another. Unlike traditional mechanical conveyors that rely on physical components like belts or screws, pneumatic systems utilize pressure differentials and air flow to move materials efficiently. This method offers several advantages, including reduced equipment wear, lower maintenance costs, and the ability to handle materials with varying particle sizes and moisture content.
At the heart of a pneumatic conveying system is the air compressor, which generates the necessary pressure to move the material. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a pipeline network to transport the material, and a receiver for the final discharge. The air is introduced into the pipeline, creating a flow that entrains the fertilizer particles and propels them through the system. The design of the pipeline, including bends, elbows, and expansion joints, is critical to ensure smooth material transport and prevent blockages or material degradation.
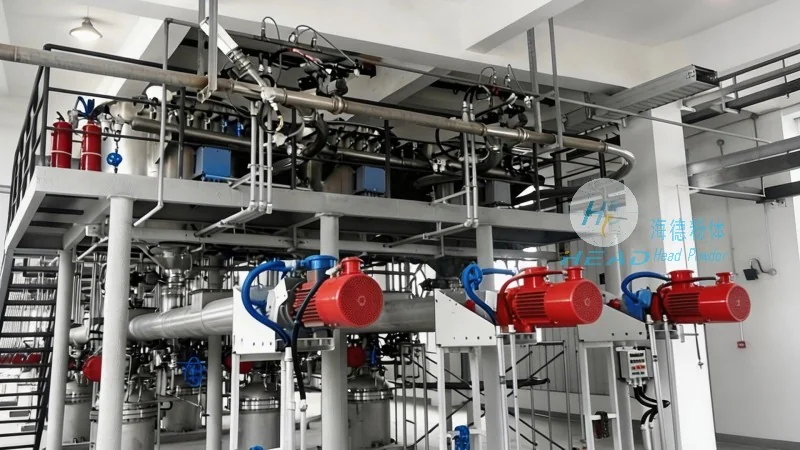
One of the most significant characteristics of fertilizer pneumatic conveying equipment is its adaptability to diverse operational environments. These systems are widely used in agricultural settings, where they facilitate the efficient transfer of fertilizers from storage silos to application machinery on farms. The ability to handle large volumes of material quickly and reliably is crucial for meeting the demands of modern farming, which often requires precise and timely nutrient delivery.
In industrial settings, such as fertilizer production plants and processing facilities, pneumatic conveying systems play a vital role in integrating different stages of the production process. For instance, they can transport raw materials from storage areas to mixing and granulation units, or move finished products from packaging lines to storage silos. The flexibility of these systems allows them to be integrated into existing production lines with minimal disruption, enhancing overall operational efficiency.
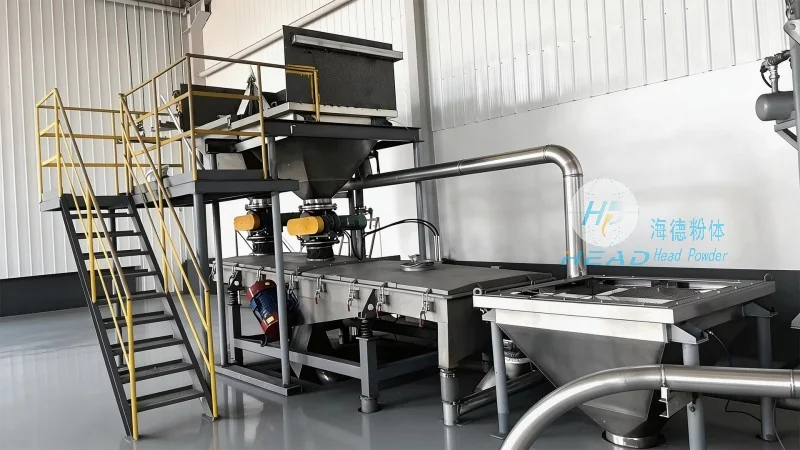
Another key characteristic is the system's ability to handle materials with varying properties. Fertilizers can range from fine powders to coarse granules, and pneumatic conveying systems are designed to accommodate these variations. The use of appropriate air velocities and pressure levels ensures that the material is transported without excessive wear or degradation. This adaptability makes the equipment suitable for a wide range of fertilizer types, including nitrogen, phosphorus, and potassium (NPK) blends, as well as specialty fertilizers.
When considering the working scene characteristics, several advantages of fertilizer pneumatic conveying equipment become apparent. Firstly, the system offers a high degree of automation, reducing the need for manual handling and minimizing the risk of human error. This is particularly important in industrial settings where safety and consistency are paramount. Secondly, the equipment is highly efficient in terms of energy consumption, as the air compressor can be optimized to operate at peak performance, reducing operational costs over time.
In agricultural applications, the system's ability to deliver fertilizers to specific areas with precision is a major advantage. This allows farmers to apply the right amount of nutrients to their fields, improving crop yields while minimizing environmental impact. The system can be integrated with GPS and other precision farming technologies to ensure accurate placement of fertilizers, further enhancing its effectiveness.
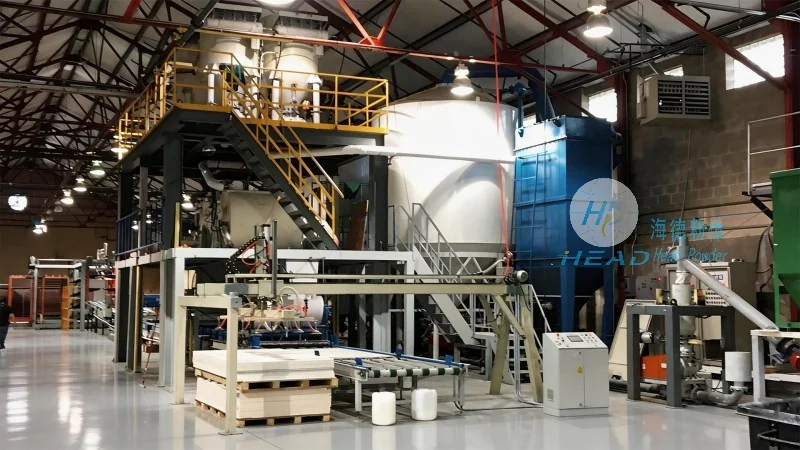
Furthermore, the flexibility of the system allows for easy expansion or modification as operational needs change. Whether a farm expands its land or a fertilizer plant increases its production capacity, the pneumatic conveying system can be scaled up or adjusted to meet the new requirements. This adaptability ensures that the equipment remains a valuable asset for years to come.
HeadPowder's fertilizer pneumatic conveying equipment exemplifies the advanced technology and engineering expertise of Shandong-based manufacturers. By understanding the core principles and working scene characteristics of these systems, users can leverage their benefits to enhance operational efficiency, reduce costs, and improve the quality of fertilizer handling in both agricultural and industrial settings. With a focus on innovation and customer satisfaction, HeadPowder continues to provide reliable solutions that meet the evolving needs of the fertilizer industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top