For industries dealing with magnesium sulfate powder, efficient and reliable material handling is crucial. The magnesium sulfate powder conveying system is designed to address the challenges of transporting this fine powder while maintaining quality and safety standards. This article provides an overview of the system's structure and operational principles, highlighting key components and their functions.
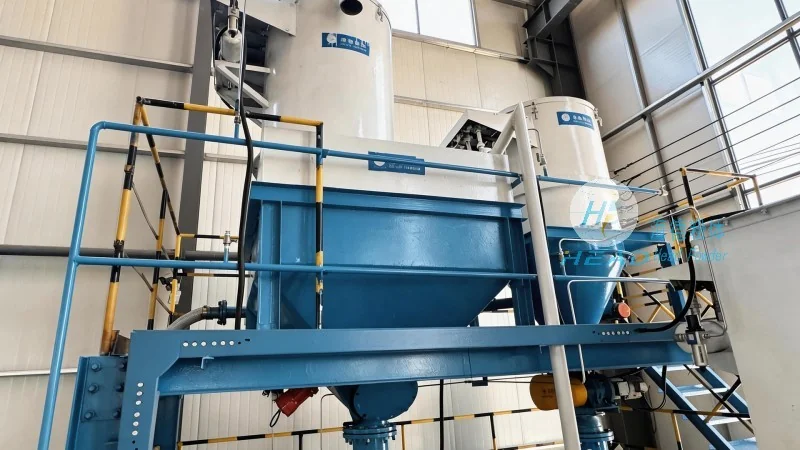
The magnesium sulfate powder conveying system typically consists of several core components that work in tandem to ensure smooth material flow. The primary components include a hopper for material storage, a feeder to control the discharge rate, a conveyor mechanism (such as a screw or pneumatic conveyor), and a dust collection system to maintain air quality. Each component plays a critical role in the overall efficiency of the system.
The system operates by first loading magnesium sulfate powder into the hopper. The feeder then regulates the flow of powder from the hopper to the conveyor. Depending on the system design, the conveyor may use mechanical force (e.g., a screw conveyor) or pneumatic pressure to move the powder through the system. The dust collection system is integrated to capture any airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment.
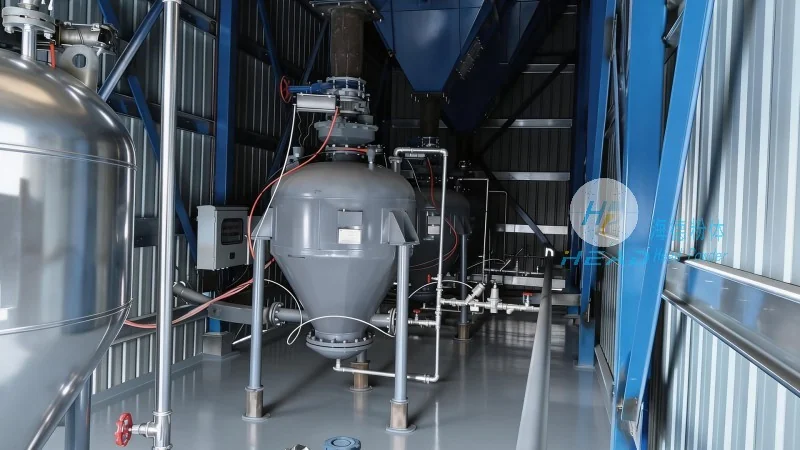
Implementing a specialized conveying system for magnesium sulfate offers several advantages. It minimizes material degradation by reducing friction and impact during transport, which is particularly important for fine powders that are prone to caking or agglomeration. The system also enhances operational safety by controlling dust emissions and preventing blockages that could lead to system downtime. Additionally, the controlled feeding mechanism allows for precise dosing, which is essential for applications requiring consistent powder quality.
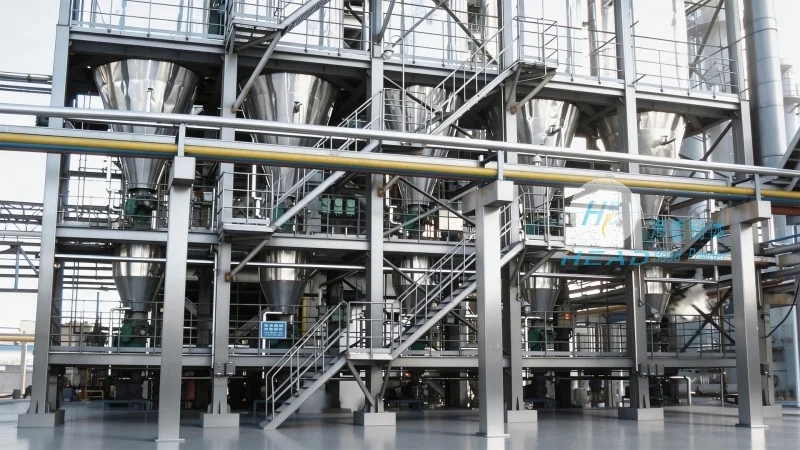
The magnesium sulfate powder conveying system is widely used in various industries, including pharmaceuticals, food processing, and chemical manufacturing. In the pharmaceutical sector, it ensures that raw materials are handled hygienically and efficiently, meeting stringent quality control standards. In food processing, the system maintains the purity of the powder, which is critical for consumer safety. In chemical manufacturing, it supports the production of magnesium sulfate-based products by providing a reliable supply chain for raw materials.
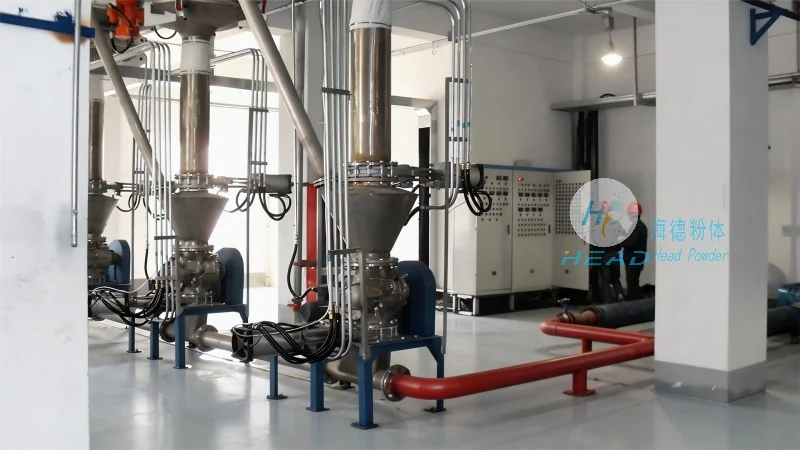
Shandong HeadPowder Engineering Co., Ltd. offers customized solutions tailored to the specific needs of each client. The company’s expertise in powder handling technology allows for the design of systems that can accommodate varying powder characteristics, such as moisture content or particle size. Regular maintenance is essential to ensure the longevity and efficiency of the system. HeadPowder provides comprehensive maintenance services, including routine inspections, component replacement, and troubleshooting to minimize downtime and maximize performance.
The magnesium sulfate powder conveying system is a vital piece of equipment for industries that rely on efficient material handling. By understanding its structure and working principles, businesses can optimize their operations, improve product quality, and enhance safety standards. With the support of companies like Shandong HeadPowder Engineering Co., Ltd., industries can implement effective conveying solutions that meet their specific requirements and contribute to overall operational success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top