Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier based in Shandong, China. The company specializes in the design, development, and production of pneumatic conveying equipment for mineral particle transport. This article provides an overview of the mineral particle pneumatic conveying equipment, detailing its structural components and operational principles.
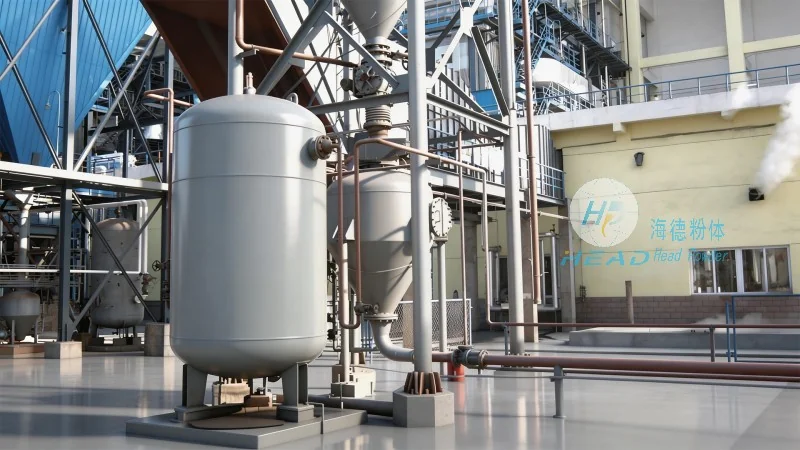
Pneumatic conveying equipment is a critical technology in the mineral processing and material handling industries. It enables the efficient and safe transport of bulk solid materials, such as minerals, powders, and granules, over long distances or within complex processing systems. The equipment operates by using a pressurized or vacuum air stream to move particles through a pipeline network. This method offers advantages over traditional mechanical conveying systems, including reduced maintenance, lower risk of material contamination, and the ability to handle a wide range of particle sizes and shapes.
The mineral particle pneumatic conveying system typically consists of several key components that work in concert to achieve effective material transport. These components include the feed hopper, air supply system, conveying pipeline, separation and collection unit, and control system. Each component plays a vital role in the overall operation of the equipment.
The feed hopper is the initial component where the mineral particles are introduced into the system. It is designed to store and meter the material before it is fed into the conveying pipeline. The hopper may include features such as a rotary valve or a screw feeder to regulate the flow rate of the material. This ensures a consistent and controlled supply of particles to the system, preventing blockages and maintaining optimal conveying efficiency.
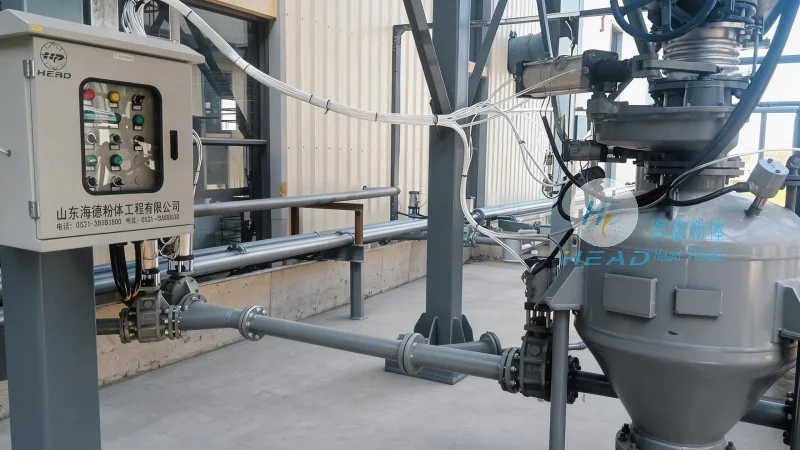
The air supply system is responsible for generating the necessary airflow to move the particles through the pipeline. This system typically includes a blower or a vacuum pump, depending on the conveying method (positive pressure or negative pressure). The blower provides compressed air to push the particles forward, while the vacuum pump creates a suction force to draw the particles into the pipeline. The air supply system is equipped with pressure regulators and filters to maintain stable and clean air conditions, ensuring the longevity of the equipment and the quality of the conveyed material.
The conveying pipeline is the main channel through which the mineral particles are transported. It is usually made of durable materials such as stainless steel or plastic, which are resistant to corrosion and wear from the abrasive particles. The pipeline may include bends, elbows, and straight sections, with appropriate fittings to connect the components. The design of the pipeline is crucial for minimizing pressure losses and ensuring smooth particle flow. The diameter and length of the pipeline are determined based on the particle size, flow rate, and required conveying distance.
The separation and collection unit is the final component of the pneumatic conveying system. Its primary function is to separate the conveyed particles from the air stream and collect them in a designated container. This unit typically consists of a cyclone separator or a bag filter, which uses centrifugal force or filtration to separate the particles from the air. The separated particles are then discharged into a collection bin or hopper, while the clean air is either vented to the atmosphere or recirculated back to the system. The efficiency of the separation unit is critical for maintaining the purity of the conveyed material and preventing dust emissions.
The control system is responsible for monitoring and regulating the operation of the entire pneumatic conveying equipment. It includes sensors and control panels that track parameters such as air pressure, flow rate, and material level. The system can be programmed to adjust the operation based on real-time conditions, ensuring optimal performance and preventing system failures. The control system may also include safety features, such as pressure relief valves and emergency shut-off mechanisms, to protect the equipment and personnel from potential hazards.
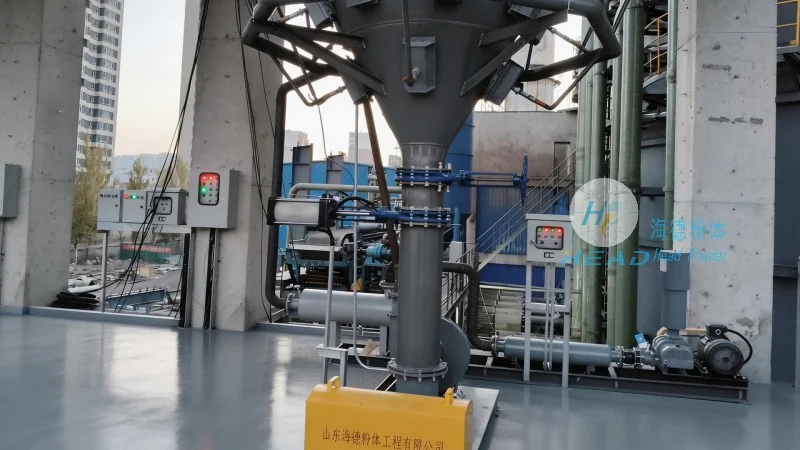
The operation of the mineral particle pneumatic conveying equipment follows a systematic process that involves the sequential activation of each component. The process begins with the material being fed into the hopper, where it is metered and prepared for transport. The air supply system then generates the necessary airflow, which is introduced into the conveying pipeline. The particles are then entrained by the air stream and carried through the pipeline to the separation unit. In the separation unit, the particles are separated from the air and collected. The clean air is either vented or recirculated, completing the cycle. The control system continuously monitors and adjusts the operation to maintain the desired conveying conditions.
Mineral particle pneumatic conveying equipment is widely used in various industries, including mining, chemical processing, food processing, and pharmaceuticals. The equipment is particularly suitable for transporting abrasive, dusty, or hazardous materials that are difficult to handle with traditional mechanical systems. The benefits of using pneumatic conveying include improved safety, reduced labor costs, increased production efficiency, and lower maintenance requirements. The equipment can handle a wide range of particle sizes, from fine powders to coarse granules, and can transport materials over long distances with minimal loss or degradation.
Shandong HeadPowder Engineering Co., Ltd. provides high-quality mineral particle pneumatic conveying equipment that is designed to meet the specific needs of various industrial applications. The equipment's robust structure and efficient operational principles ensure reliable and consistent material transport. By understanding the structural components and working principles of the equipment, users can make informed decisions about its application and maintenance, maximizing its performance and longevity. The company's commitment to quality and innovation ensures that its products remain at the forefront of pneumatic conveying technology.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top