Calcium phosphate is a widely used chemical compound in various industrial applications, and efficient handling and transportation of this material are crucial for industrial operations. Pneumatic conveying systems offer a reliable and effective solution for moving calcium phosphate powder, ensuring minimal dust generation and maintaining product quality. This article provides an overview of calcium phosphate pneumatic conveying equipment, detailing its structure and working principles to help users understand its functionality and benefits. The equipment is engineered by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in industrial material handling solutions.
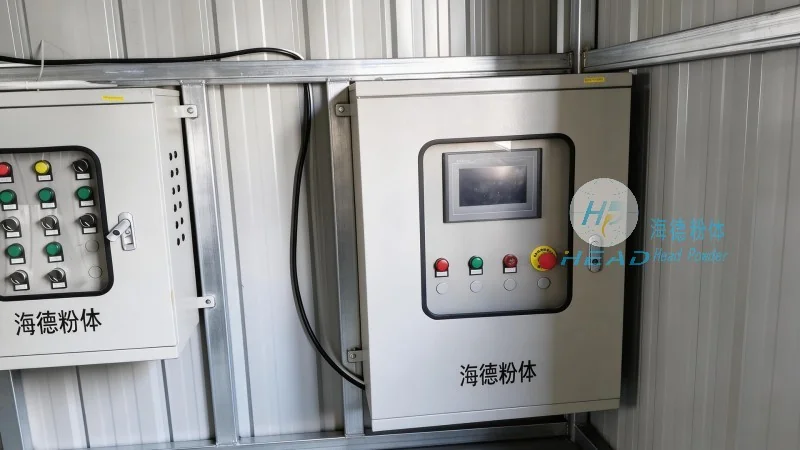
Calcium phosphate pneumatic conveying equipment is designed to transport calcium phosphate powder through a system of pipes using air or other gas as the conveying medium. This technology is particularly suitable for handling fine powders like calcium phosphate, which can be challenging to transport using traditional methods such as belt conveyors or bucket elevators. The equipment is engineered to minimize product degradation, prevent contamination, and ensure consistent flow rates, making it an ideal choice for industries that require precise material handling.
The calcium phosphate pneumatic conveying system typically consists of several key components, each playing a vital role in the overall operation. The main components include a hopper for material storage, a feeder to control the flow of powder into the system, a conveying line (usually made of stainless steel or other corrosion-resistant materials to handle the chemical properties of calcium phosphate), a venturi or other air induction device to create the necessary airflow, and a receiver or collection tank to store the conveyed material. The system may also include a filter or cyclone to separate the powder from the air stream, ensuring clean air is released back into the environment. The entire structure is designed to be compact and efficient, with components arranged to minimize space requirements while maximizing conveying efficiency.
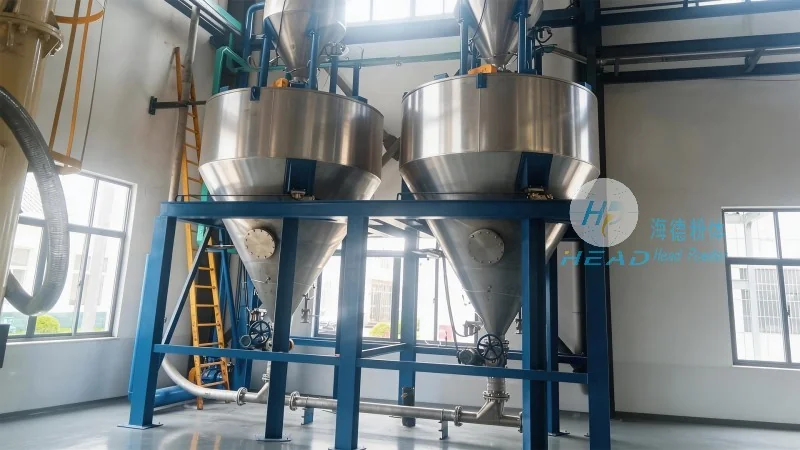
The operation of the calcium phosphate pneumatic conveying equipment follows a simple yet effective principle: creating a pressure differential to move the powder through the system. The process begins with the material being fed from the hopper into the conveying line. Simultaneously, a fan or blower generates a high-velocity airflow through the venturi or induction device. As the air flows through the conveying line, it picks up the calcium phosphate powder particles, forming a slurry or "pneumatic stream." The mixture of air and powder is then transported through the pipeline to the receiver, where the air is separated from the powder using a filter or cyclone. The purified air is discharged, while the calcium phosphate powder is collected in the receiver for further processing or storage. The system operates continuously, with the feeder adjusting the material flow rate to maintain a stable conveying rate, ensuring consistent performance and preventing system overload.
There are several advantages to using pneumatic conveying equipment for calcium phosphate transportation. Firstly, it eliminates the need for mechanical contact with the material, reducing the risk of contamination and product degradation. The enclosed system also minimizes dust emissions, improving workplace safety and environmental compliance. Additionally, pneumatic conveying allows for flexible and scalable systems, with the ability to adjust the conveying capacity by modifying the airflow or pipe diameter. This adaptability makes it suitable for various production scales, from small-scale laboratory applications to large industrial plants. Furthermore, the system can be integrated with other processing equipment, such as mixers or reactors, to create a seamless material handling workflow, enhancing overall operational efficiency.
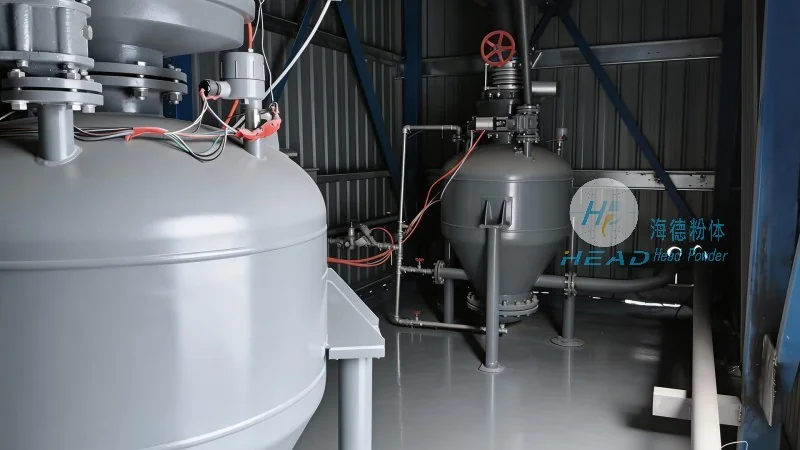
Calcium phosphate pneumatic conveying equipment is widely used in several industrial sectors that rely on calcium phosphate as a raw material. In the food and beverage industry, it is used to transport calcium phosphate as an additive in dairy products, beverages, and nutritional supplements. In the pharmaceutical industry, the equipment is employed to handle calcium phosphate as an excipient or active ingredient in drug formulations, ensuring precise dosing and quality control. The chemical industry also utilizes this technology for transporting calcium phosphate in the production of fertilizers, ceramics, and other chemical products. Each application benefits from the consistent and reliable material handling provided by the pneumatic conveying system, which helps maintain product quality and operational efficiency.
Proper maintenance and operational practices are essential to ensure the long-term performance and reliability of calcium phosphate pneumatic conveying equipment. Regular cleaning of the hopper, feeder, and conveying line is necessary to prevent powder buildup and blockages, which can reduce conveying efficiency and increase maintenance costs. The air filter or cyclone should be checked and replaced as needed to maintain air quality and prevent dust accumulation in the system. Additionally, the fan or blower should be inspected for proper operation, as any issues with airflow can impact the conveying rate. It is also important to monitor the system for signs of wear and tear, such as pipe corrosion or component failure, and address them promptly to avoid system downtime. By following these maintenance guidelines, users can maximize the lifespan of the equipment and ensure consistent performance over time.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top