Pneumatic conveying equipment plays a crucial role in the efficient handling and transportation of rice grain within processing facilities. As a key component in the rice industry, these systems ensure the safe and reliable movement of raw materials from storage to processing stages. The design and operation of rice grain pneumatic conveyors are tailored to address the unique characteristics of rice, such as its size, density, and susceptibility to breakage during transport. By understanding the structural principles and operational mechanisms of these systems, stakeholders in the rice processing sector can optimize their material handling processes and enhance overall productivity.
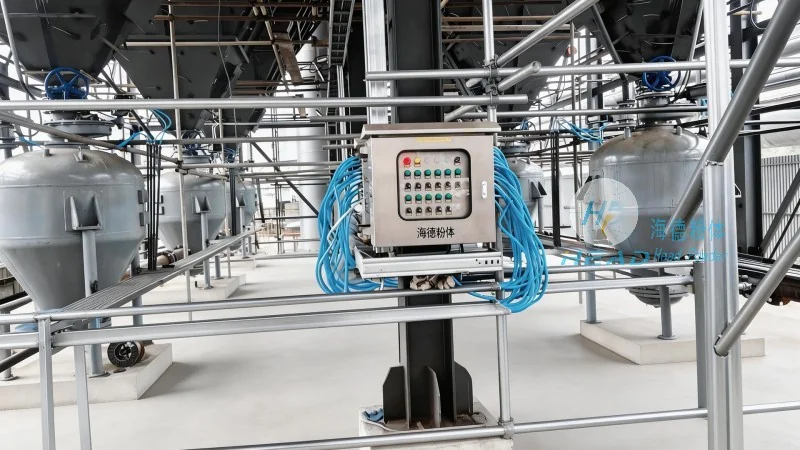
The core components of a rice grain pneumatic conveying system include the feed hopper, air compressor, conveying pipeline, separation unit, and discharge hopper. The feed hopper is responsible for storing and regulating the flow of rice grain into the system. It is typically equipped with a rotary valve or feeder to control the material feed rate, preventing overloading and ensuring consistent air-material ratios. The air compressor generates the necessary pressure to move the rice grain through the pipeline. The conveying pipeline, often made of stainless steel or plastic, is designed to withstand the pressure and friction of the material flow. The separation unit, such as a cyclone or filter, removes excess air and fine particles from the conveying stream, ensuring the rice grain remains clean and free from contamination. The discharge hopper collects the transported rice grain and directs it to the next processing stage. The working principle involves the creation of a low-pressure zone in the pipeline, which draws the rice grain into the air stream. As the mixture travels through the pipeline, the air and grain are separated at the discharge point, with the rice grain falling into the collection hopper and the air being filtered or recirculated.
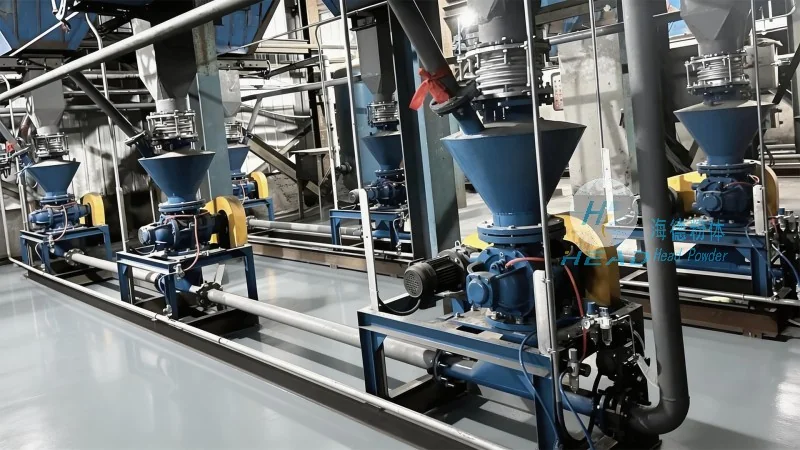
HeadPowder, a leading manufacturer of pneumatic conveying systems, offers specialized equipment designed to meet the specific needs of rice grain processing. The company's products are engineered with features that enhance efficiency, durability, and safety. For instance, the equipment incorporates advanced materials and construction techniques to minimize wear and tear from the abrasive nature of rice grain. This results in longer service life and reduced maintenance costs. Additionally, the systems are equipped with intelligent control panels that allow for real-time monitoring and adjustment of operational parameters, such as air pressure and feed rate. This ensures optimal performance and prevents equipment damage. The pneumatic conveying process also offers advantages over traditional mechanical conveyors, including reduced risk of product contamination, lower energy consumption, and the ability to handle a wide range of grain sizes and moisture content. These benefits make rice grain pneumatic conveyors an ideal choice for modern rice processing facilities seeking to improve their operational efficiency and product quality.
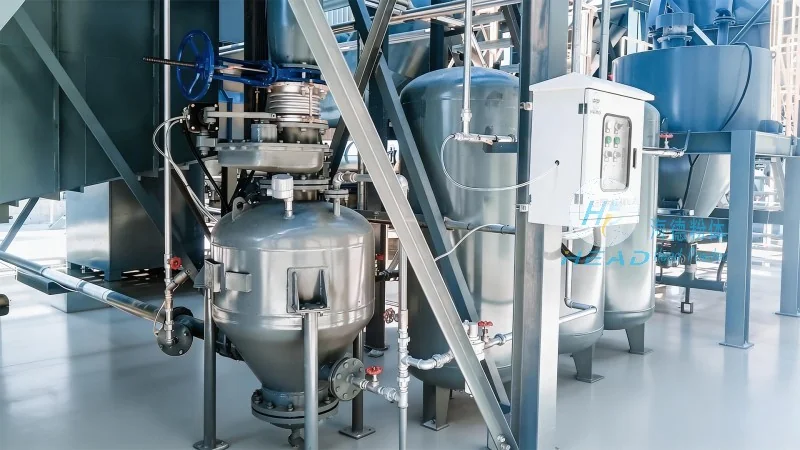
Rice grain pneumatic conveying equipment is widely used in various stages of rice processing, from raw material handling to finished product packaging. In the raw material stage, the equipment efficiently transports rice from storage silos to processing lines, ensuring a continuous supply of material. During the processing stage, it can be used to move rice between different processing units, such as cleaning, milling, and polishing. In the final packaging stage, the equipment delivers the finished rice products to packaging machines, maintaining product integrity and preventing cross-contamination. Operational considerations for these systems include proper air pressure regulation, regular maintenance of components like filters and rotary valves, and monitoring of material flow rates. Proper training of operators on the safe and efficient operation of the equipment is also essential to prevent accidents and ensure optimal performance. By adhering to these considerations, rice processing facilities can maximize the benefits of pneumatic conveying systems and achieve consistent, high-quality production.
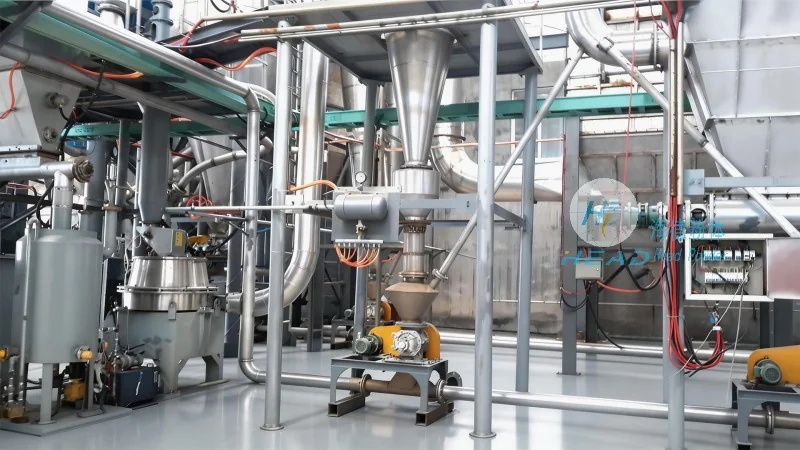
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable manufacturer specializing in the design, development, and production of pneumatic conveying equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the rice and grain processing industry. HeadPowder's team of engineers and technicians leverages advanced technology and industry expertise to create customized solutions that meet the unique requirements of each client. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales service, including installation, training, and maintenance support. HeadPowder's facilities are equipped with state-of-the-art manufacturing equipment and quality control systems, ensuring that every product meets or exceeds industry standards. The company's dedication to excellence has earned it a strong reputation among clients in China and internationally, making it a preferred choice for those seeking reliable and efficient pneumatic conveying solutions for rice grain processing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top