For coffee processing facilities, efficient material handling is crucial to maintaining product quality and operational efficiency. Coffee pneumatic conveying systems represent a sophisticated solution that addresses these needs by transporting coffee beans, grounds, and other related materials through an air-driven process. This article provides an overview of coffee pneumatic conveying systems, detailing their structural design and working principles, as well as the technical advantages they offer to the coffee industry.
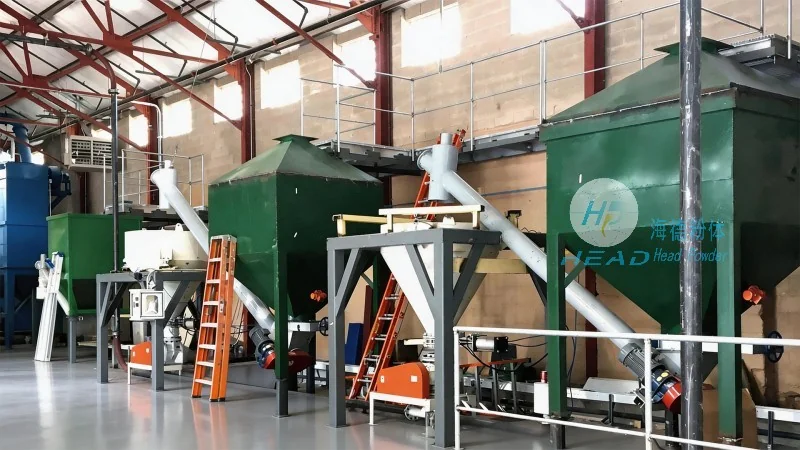
HeadPowder, a leading manufacturer based in Shandong, China, specializes in designing and manufacturing advanced coffee pneumatic conveying systems. The company's commitment to quality and innovation has positioned it as a trusted partner for coffee producers worldwide, with a focus on solutions that enhance the efficiency and quality of coffee processing operations.
Coffee pneumatic conveying systems typically consist of several key components, each engineered to work in harmony to ensure reliable material transport. The primary components include a hopper for material storage, a feeder to control the flow of coffee, a conveying line (often made of stainless steel or other corrosion-resistant materials), and a receiver for the discharged material. The system may also incorporate additional elements like filters, cyclones, or vacuum pumps, depending on the specific requirements of the coffee processing line. The design emphasizes durability and hygiene, as coffee products require equipment that can withstand the demands of continuous operation while maintaining food safety standards.
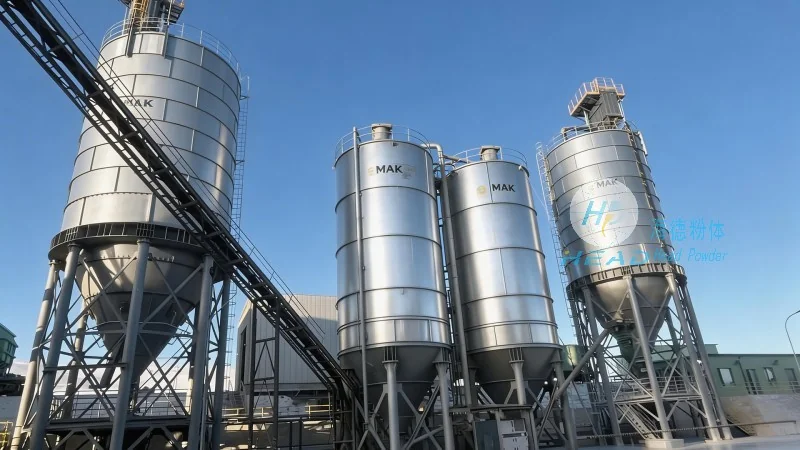
The core of a coffee pneumatic conveying system is the air-driven mechanism that propels material through the conveying line. There are two main types of pneumatic conveying systems: pressure and vacuum. In pressure systems, compressed air is used to push coffee from the hopper to the receiver, while vacuum systems use a vacuum to draw material from the source. For coffee applications, pressure systems are often preferred as they provide more consistent and reliable material flow, especially when handling fine particles like coffee grounds. The system operates by introducing air into the conveying line at a controlled pressure, creating a flow that lifts and transports the coffee particles. The air velocity is carefully managed to prevent material degradation and ensure efficient transport, with the design optimized to maintain the integrity of the coffee beans throughout the process.
Coffee pneumatic conveying systems are widely used in various stages of coffee processing, from raw bean handling to final product packaging. They are commonly employed in: (1) transporting raw coffee beans from storage silos to roasting equipment, (2) conveying roasted beans to packaging lines, (3) moving ground coffee from grinding machines to storage tanks, and (4) transferring coffee extracts or concentrates in liquid form. The flexibility of these systems allows them to adapt to different processing stages, ensuring a seamless workflow from raw material to finished product. HeadPowder's systems are tailored to meet the specific needs of each client, with customizable configurations that optimize performance for individual coffee processing lines.
HeadPowder Engineering Co., Ltd. places a strong emphasis on quality control throughout the design and manufacturing process. The company uses high-grade materials, such as stainless steel and food-grade plastics, to ensure that the conveying systems meet the stringent hygiene standards required in the coffee industry. Each system is rigorously tested for performance, durability, and compliance with industry regulations. This commitment to quality has earned HeadPowder a reputation for reliability and longevity, with many of their systems operating for over a decade without major maintenance. The company's team of engineers and technicians provides ongoing support to ensure that clients receive the best possible service and performance from their equipment.
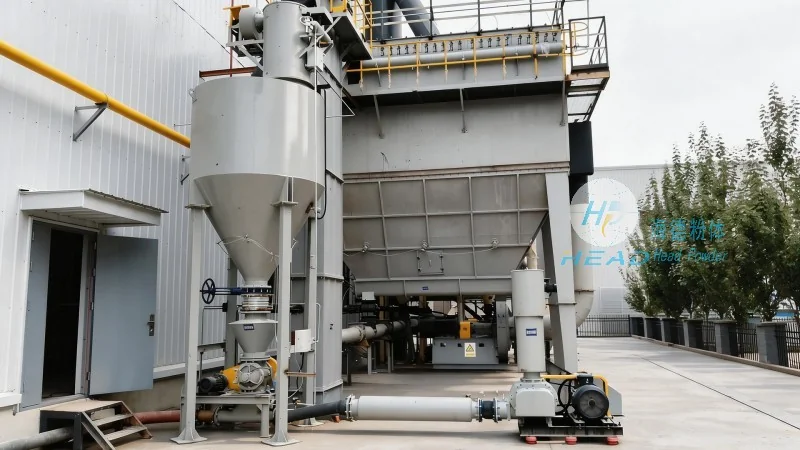
Compared to traditional mechanical conveying methods, coffee pneumatic conveying systems offer several advantages. These include reduced labor costs, as the systems can operate automatically with minimal human intervention. They also minimize material damage, preserving the flavor and aroma of coffee beans, which is critical for maintaining product quality. Additionally, pneumatic systems are more energy-efficient than other methods, as they use compressed air to transport material rather than mechanical components like belts or chains. The compact design of these systems also saves space in processing facilities, making them ideal for both large-scale and small-scale coffee operations. HeadPowder's systems are designed to maximize efficiency while reducing operational costs, providing a competitive edge for coffee producers.
HeadPowder's coffee pneumatic conveying systems have been adopted by numerous coffee producers and roasters across China and internationally. Customers consistently praise the systems for their efficiency, reliability, and ease of maintenance. For example, a leading coffee roaster in Shandong reported a 20% increase in production capacity after implementing a HeadPowder system, while also reducing material waste by 15%. These positive outcomes reflect the effectiveness of the company's solutions in addressing the specific needs of the coffee industry. HeadPowder has received recognition from industry associations for its contributions to the advancement of coffee processing technology, further solidifying its position as a leader in the field.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top