The Ammonium Sulfate Pneumatic Conveying System is a specialized industrial solution designed for the efficient and safe transportation of ammonium sulfate, a common fertilizer and chemical raw material. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, this system integrates advanced pneumatic conveying technology to meet the demanding requirements of modern chemical and agricultural processing industries. The system is engineered to handle the unique properties of ammonium sulfate, ensuring minimal product degradation, high transfer efficiency, and compliance with safety standards.
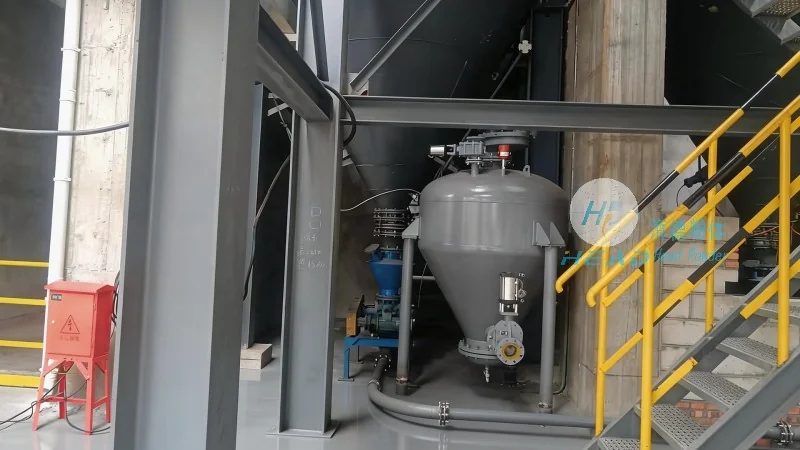
The pneumatic conveying system for ammonium sulfate consists of several key components, each playing a critical role in the overall operation. The primary components include a material hopper, a rotary airlock feeder, a conveying pipeline system, a pressure vessel or receiver, and a dust collection unit. The material hopper is designed to store the ammonium sulfate, providing a consistent feed source. The rotary airlock feeder ensures a controlled and continuous discharge of the material into the conveying pipeline, preventing backflow and maintaining system pressure. The conveying pipeline, typically made of corrosion-resistant materials such as stainless steel or special plastic, is configured to handle the abrasive nature of ammonium sulfate particles. The pressure vessel or receiver collects the conveyed material at the destination point, while the dust collection unit ensures that any airborne particles are captured and returned to the system, maintaining environmental compliance and product purity.
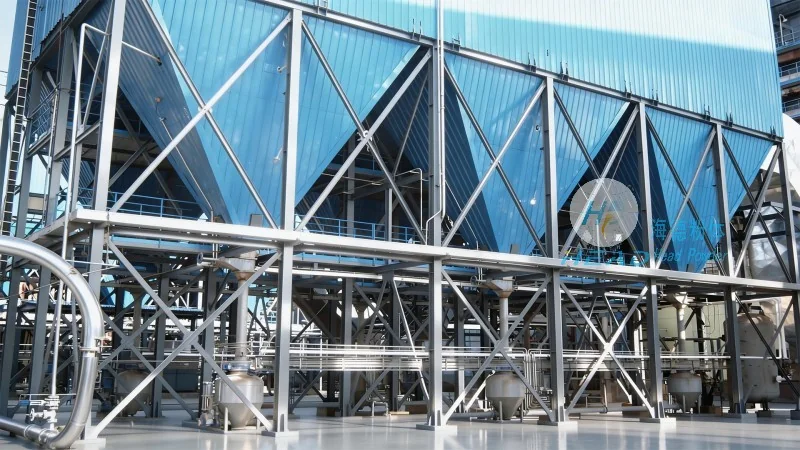
The operation of the ammonium sulfate pneumatic conveying system is based on the principle of pneumatic transport, where material is moved through a pipeline using a stream of air or gas. The process begins with the material being fed from the hopper into the rotary airlock feeder. The feeder then releases the material into the conveying pipeline under controlled conditions. Simultaneously, a fan or blower generates a high-velocity air stream that propels the ammonium sulfate particles through the pipeline. The air velocity is carefully regulated to ensure that the particles are carried efficiently without causing excessive wear on the system components. The conveying pipeline is typically arranged in a loop or straight line, depending on the layout of the facility. At the receiving end, the material is deposited into the pressure vessel or receiver. The air stream then passes through a filter or cyclone separator, where the remaining particles are captured and returned to the system, while the clean air is discharged or recirculated. This closed-loop system minimizes product loss and maintains a consistent material flow, enhancing overall operational efficiency.
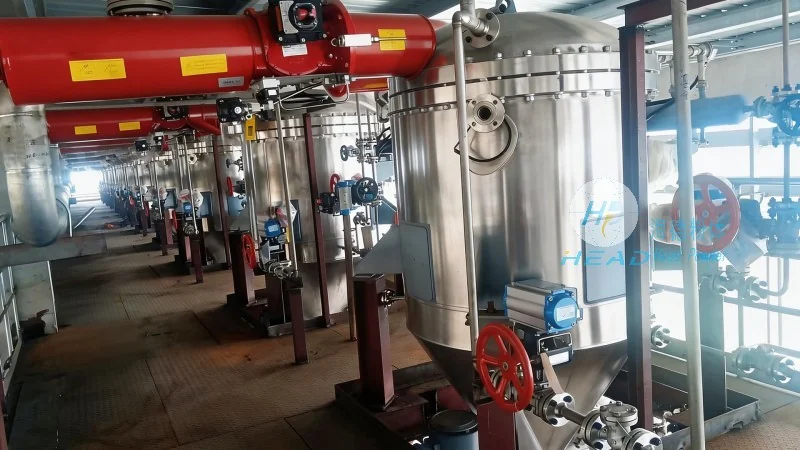
Implementing the ammonium sulfate pneumatic conveying system offers several significant advantages for industrial applications. Firstly, it provides a dust-free and hygienic method of material handling, which is crucial for maintaining product quality and adhering to regulatory standards. Unlike traditional belt or bucket elevators, pneumatic conveying eliminates the risk of product contamination and reduces the need for extensive cleaning operations. Secondly, the system offers high transfer efficiency, with minimal material degradation due to the gentle handling of particles. This is particularly important for ammonium sulfate, which can be sensitive to moisture and mechanical stress. Thirdly, the system is highly flexible and can be easily integrated into existing production lines or expanded to accommodate increased production capacity. The modular design allows for customization based on specific process requirements, such as varying material flow rates or pipeline lengths. Additionally, the system operates with low maintenance requirements, as the components are designed for durability and resistance to corrosion from ammonium sulfate and other chemicals. This reduces downtime and operational costs over the long term.
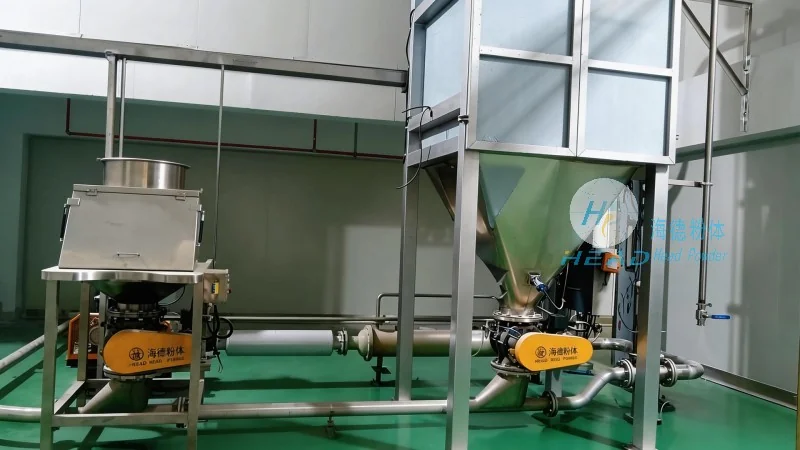
The ammonium sulfate pneumatic conveying system is widely used in various industrial sectors, including chemical manufacturing, fertilizer production, and food processing. In chemical plants, it facilitates the transport of ammonium sulfate between reactors, storage tanks, and packaging lines, ensuring a smooth and continuous production process. In fertilizer production facilities, the system is essential for moving ammonium sulfate from storage silos to blending and packaging equipment, supporting high-volume agricultural operations. The system's ability to handle large quantities of material efficiently makes it ideal for bulk material handling applications, where traditional methods may be impractical or inefficient. By improving material flow and reducing handling time, the system enhances overall productivity and reduces labor costs. Furthermore, the system's compliance with environmental regulations, such as the capture of airborne particles, contributes to a more sustainable and environmentally friendly operation, aligning with the growing emphasis on green manufacturing practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top