Distillers grains are a byproduct of the ethanol production process, and efficient handling of these powders is crucial for the smooth operation of biorefineries. The powder conveying system equipment designed by Shandong HeadPowder Engineering Co., Ltd. addresses this need with advanced technology tailored to the unique characteristics of distillers grains. This article explores the working principle and key features of this specialized equipment, providing insights into how it enhances material handling in industrial settings.
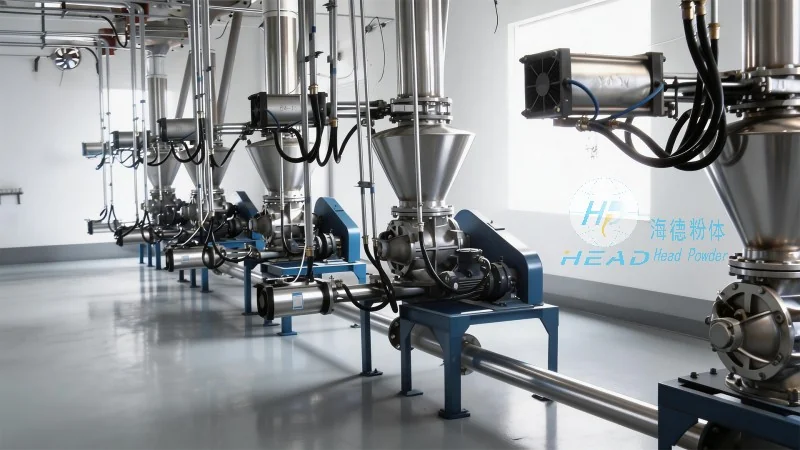
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of industrial conveying solutions based in China. With a focus on innovation and reliability, the company has developed a range of equipment suitable for various bulk material handling applications. The distillers grains powder conveying system is specifically engineered to handle the challenges posed by distillers grains, a fine powder that requires gentle yet efficient transport from storage to processing units. The system combines proven technologies to ensure consistent performance and minimal product degradation.
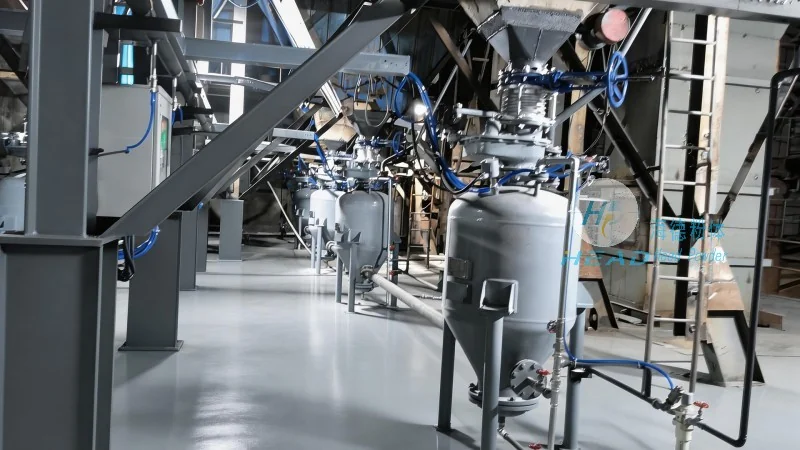
The distillers grains powder conveying system operates on a combination of air and mechanical forces to transport the material. At its core, the system utilizes a positive displacement blower or a high-pressure air source to create a flow of air within the conveying line. This air flow draws the distillers grains powder from the source, such as a silo or storage bin, and propels it through the pipeline to the destination point. The design incorporates a series of components, including a hopper, a rotary valve for material feeding, and a filter or separator to prevent dust from escaping into the environment. The blower maintains a consistent air pressure, ensuring that the powder moves smoothly without clogging or loss. The system is equipped with sensors and controls that monitor the flow rate and pressure, allowing for real-time adjustments to maintain optimal performance. This integrated approach ensures that the material is conveyed safely and efficiently, minimizing the risk of product degradation or environmental contamination.
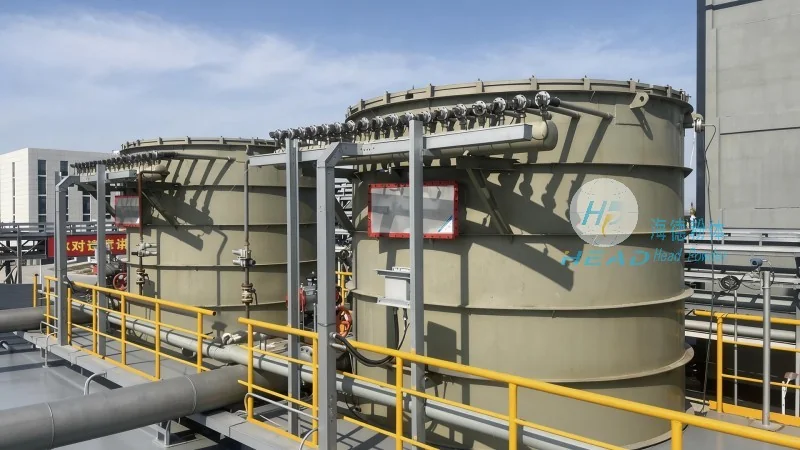
The distillers grains powder conveying system from HeadPowder is distinguished by several key features that make it suitable for industrial applications. Firstly, the system is designed for gentle handling of the material, which is critical for preserving the nutritional value and quality of distillers grains. The use of air-based conveying reduces mechanical stress compared to traditional belt or screw conveyors, preventing the breakdown of the powder particles. Secondly, the system offers high efficiency and capacity, capable of handling large volumes of material at a consistent rate. This is achieved through the use of high-performance blowers and optimized pipeline designs that minimize pressure drop and energy consumption. Thirdly, the equipment is highly adaptable, with options for different material feed rates and destination configurations. This flexibility allows the system to be customized to meet the specific needs of each biorefinery, whether it's for short or long-distance transport. Additionally, the system incorporates dust control measures, such as filters and enclosed hoppers, to comply with environmental regulations and maintain a clean working environment. The use of durable materials, such as stainless steel and corrosion-resistant components, ensures long-term reliability and low maintenance costs. Finally, the system is equipped with user-friendly controls and monitoring systems, allowing operators to easily adjust settings and troubleshoot issues, reducing downtime and increasing overall productivity.
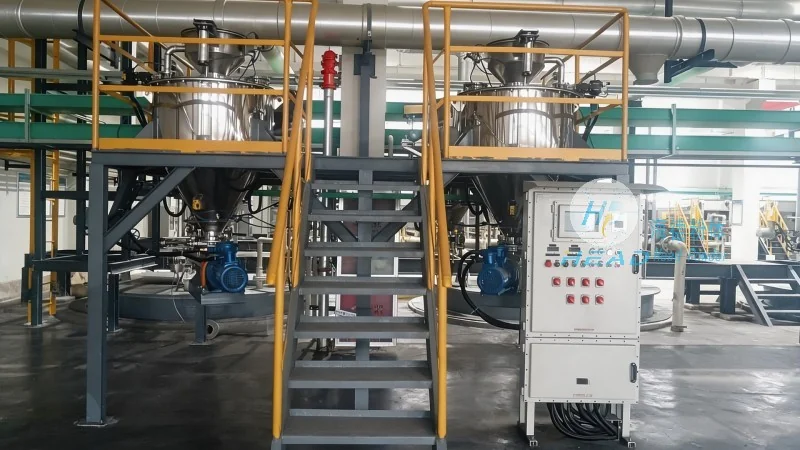
Shandong HeadPowder Engineering Co., Ltd. has developed a sophisticated distillers grains powder conveying system that addresses the unique challenges of handling this fine material. By combining advanced air conveying technology with robust mechanical components, the system ensures efficient, gentle, and reliable transport of distillers grains. The key features, including low product degradation, high capacity, adaptability, and environmental compliance, make it an ideal solution for biorefineries seeking to optimize their material handling processes. With its headquarters in China, HeadPowder continues to innovate and provide tailored solutions to meet the evolving needs of the industrial sector, ensuring that distillers grains are handled safely and effectively in modern processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top