Phenolic powder, also known as Bakelite powder, is a widely used industrial material in manufacturing processes. The pneumatic conveying system for phenolic powder is a specialized equipment designed to transport this material efficiently and safely. This article provides an overview of the phenolic powder pneumatic conveying system, focusing on its structure and working principle.
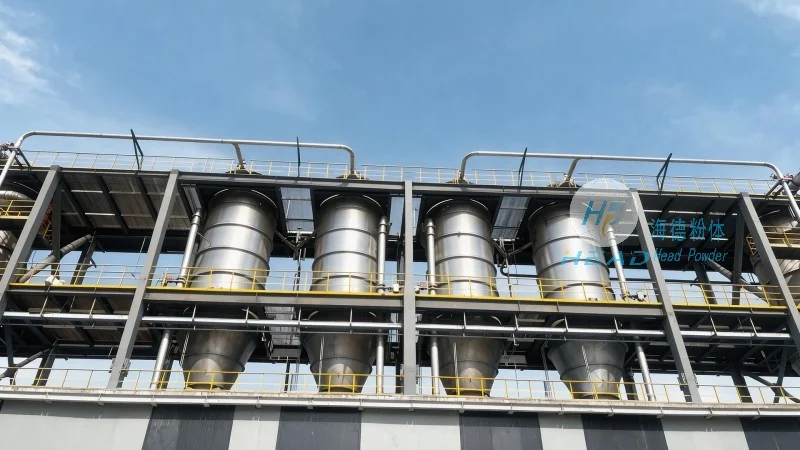
HeadPowder, a leading manufacturer in the field, specializes in the design, production, and installation of pneumatic conveying systems. With years of experience, the company has developed advanced solutions tailored to the unique characteristics of phenolic powder. HeadPowder's systems are engineered to ensure reliable operation, minimal material loss, and compliance with industrial safety standards. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art facility dedicated to research and development, manufacturing, and customer support.
The phenolic powder pneumatic conveying system is a closed-loop system that uses compressed air to transport dry powder materials. This method is particularly suitable for phenolic powder due to its fine particle size and potential for dust generation. The system is designed to handle the material from storage to processing equipment without exposing it to the environment, thus maintaining product quality and preventing contamination.
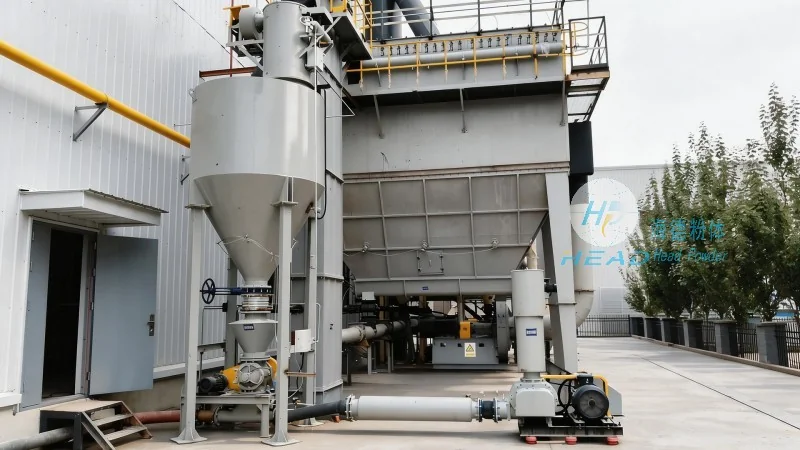
The phenolic powder pneumatic conveying system consists of several key components, each playing a crucial role in the overall operation. The main components include the hopper, feeder, air compressor, conveying line, and receiver. The hopper is used to store the phenolic powder, providing a consistent supply to the feeder. The feeder, typically a rotary valve or a screw feeder, controls the flow rate of the powder into the conveying line. The air compressor generates the necessary pressure to move the powder through the system. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the powder and air mixture. The receiver collects the powder at the destination point, separating it from the air using a cyclone or other separation equipment.
The working principle of the phenolic powder pneumatic conveying system is based on the principle of fluidization and pneumatic transport. When compressed air is introduced into the conveying line, it creates a low-pressure zone that draws the phenolic powder from the hopper into the line. The air and powder mixture travels through the line at a high velocity, ensuring that the powder particles are suspended and transported efficiently. The system operates in either positive or negative pressure mode, depending on the application requirements. In positive pressure mode, the air is forced into the conveying line, while in negative pressure mode, the air is drawn out of the line. The choice of mode depends on factors such as the distance of transport, the material characteristics, and the need to prevent dust leakage.
There are several advantages of using a pneumatic conveying system for phenolic powder. First, it provides a dust-free and clean operation, which is essential for maintaining product quality and ensuring workplace safety. Second, the system is highly efficient, with minimal material loss and low maintenance requirements. Third, it offers flexibility in terms of system layout, allowing for easy integration with existing production lines. Fourth, the system can handle a wide range of powder characteristics, including different particle sizes, densities, and moisture contents. Finally, the system is energy-efficient, with the compressed air being reused in the process, reducing operational costs.
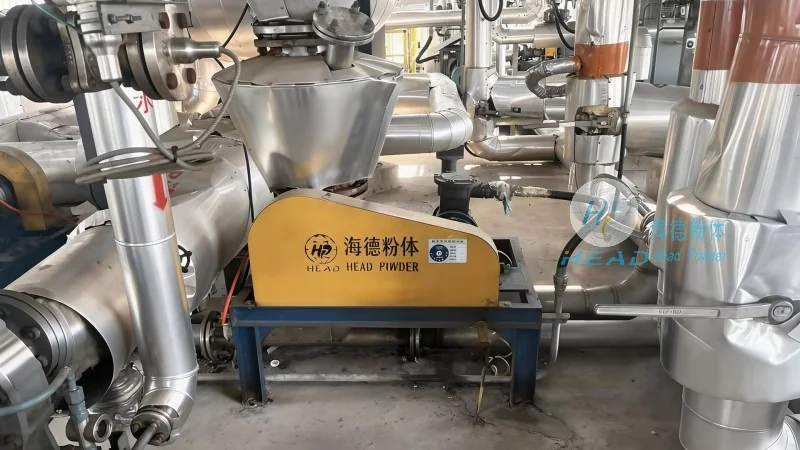
The phenolic powder pneumatic conveying system is widely used in various industries, including the manufacturing of phenolic resins, adhesives, and composites. In these applications, the system is used to transport the powder from storage silos to processing equipment such as mixers, extruders, and injection molding machines. The system ensures that the powder is delivered in a consistent and controlled manner, which is crucial for maintaining product quality and reducing downtime. Additionally, the system is used in the food and pharmaceutical industries, where the need for a clean and hygienic environment is paramount.
In conclusion, the phenolic powder pneumatic conveying system is an essential equipment for the efficient and safe transportation of phenolic powder. The system's design and working principle are tailored to the unique characteristics of the material, ensuring reliable operation and minimal environmental impact. With the expertise of companies like HeadPowder, the system has become a standard solution in various industrial applications. As the demand for phenolic powder continues to grow, the importance of efficient and reliable conveying systems will only increase, making it a critical component in the manufacturing process.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top