HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the food industry. This article provides an overview of food pneumatic conveying systems, detailing their structural components and operational principles to help industry professionals understand their functionality and benefits.
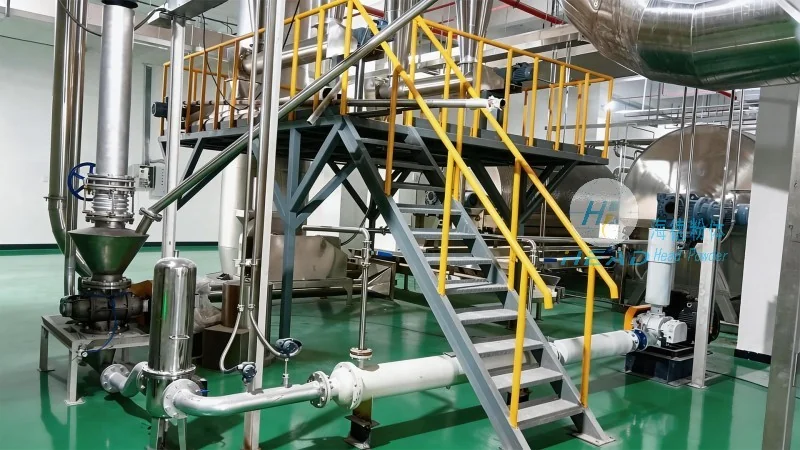
Company Profile: HeadPowder Engineering
HeadPowder Engineering Co., Ltd. is a reputable enterprise dedicated to providing high-quality solutions for material handling in the food sector. With a strong commitment to innovation and adherence to industry standards, the company has established itself as a trusted partner for businesses seeking efficient and hygienic conveying systems. HeadPowder’s expertise lies in developing customized pneumatic conveying solutions that meet the stringent requirements of food processing, ensuring product safety, quality, and compliance with regulatory standards.
Understanding Food Pneumatic Conveying Systems
Pneumatic conveying systems utilize air or gas to transport bulk materials, such as powders, granules, and other food products, from one location to another within a processing facility. These systems are widely adopted in the food industry due to their ability to handle sensitive materials without causing contamination or degradation. The core principle involves creating a pressure differential to move materials through a pipeline network, making them ideal for applications where traditional mechanical conveyors may not be suitable.
Key Structural Components of Food Pneumatic Conveying Systems
Food pneumatic conveying systems consist of several critical components that work in tandem to ensure efficient material transport. The main elements include:
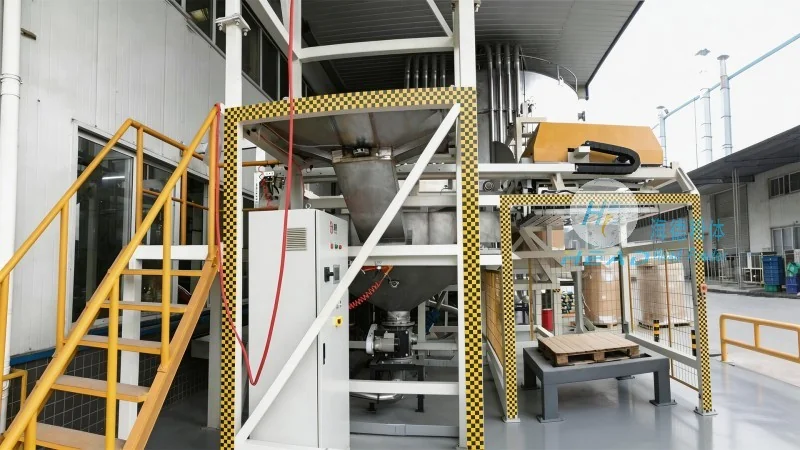
- Feeder: The feeder is responsible for feeding the material into the conveying system. For food applications, it must be designed to handle hygienic conditions, often featuring stainless steel construction and easy cleaning mechanisms. The feeder ensures a consistent flow of material into the pipeline, preventing blockages and maintaining system efficiency.
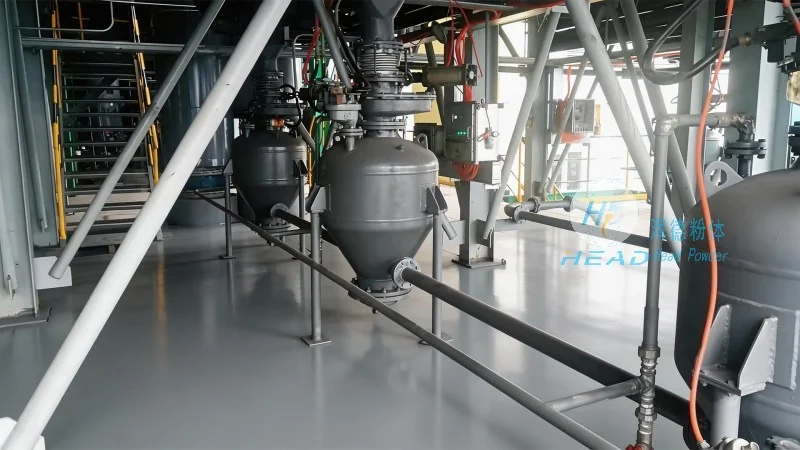
- Pneumatic Conveying Pipeline: The pipeline network is the backbone of the system, transporting materials through a series of pipes. In food applications, these pipelines are typically made from food-grade materials like stainless steel or food-grade plastic, ensuring that they do not contaminate the product. The design of the pipeline, including bends, elbows, and straight sections, is crucial for maintaining material flow and preventing material buildup or degradation.
- Air Supply System: The air supply system provides the necessary pressure and airflow to move materials through the pipeline. It includes components such as blowers, compressors, and air filters. For food applications, the air must be filtered to remove contaminants and ensure that it does not introduce any foreign particles into the product. The air supply system is designed to operate at pressures suitable for the specific material being conveyed, ensuring optimal performance.
- Control System: The control system manages the operation of the pneumatic conveying system, including the feeder, air supply, and other components. It allows for precise control over the material flow rate, pressure, and other parameters. The control system is typically equipped with sensors and monitoring devices to ensure that the system operates within safe and efficient parameters. For food applications, the control system must be easy to operate and maintain, with clear indicators for system status and any potential issues.
- Collection and Discharge Equipment: The collection and discharge equipment is used to receive the material at the end of the conveying line and discharge it into the desired destination. For food applications, this equipment is designed to be hygienic and easy to clean, often featuring stainless steel construction and smooth surfaces. The equipment may include hoppers, silos, or other containers that are suitable for the specific material being conveyed.
Working Principles of Food Pneumatic Conveying Systems
The operation of a food pneumatic conveying system involves several steps, each designed to ensure efficient and safe material transport. The process typically begins with the material being fed into the system by the feeder. The feeder then delivers the material into the pipeline, where it is mixed with the air supplied by the air system. The air and material mixture is then transported through the pipeline network to the collection point.
As the mixture travels through the pipeline, the air pressure and velocity are carefully controlled to maintain a consistent flow of material. The system may use different types of conveying, such as pressure or vacuum systems, depending on the application and the material being conveyed. Pressure systems use positive pressure to move materials, while vacuum systems use negative pressure to draw materials from a source.
Once the material reaches the collection point, the air is separated from the material, and the material is discharged into the desired container. The air is then filtered and returned to the system or released to the atmosphere, depending on the system design. The control system monitors the entire process, ensuring that the system operates efficiently and safely.
Benefits of Using Food Pneumatic Conveying Systems
Food pneumatic conveying systems offer several advantages over traditional mechanical conveyors. These include:
- Hygienic and Clean Operation: Pneumatic conveying systems are designed to be hygienic and easy to clean, making them ideal for food processing applications. The absence of moving parts in the pipeline reduces the risk of contamination, and the system can be easily disassembled and cleaned to meet regulatory standards.
- Flexibility and Versatility: Pneumatic conveying systems can handle a wide range of materials, including powders, granules, and other food products. The system can be easily adapted to different applications by adjusting the feeder, pipeline, and air supply components.
- Space Efficiency: Pneumatic conveying systems can be installed in tight spaces, as the pipeline network can be routed around obstacles and other equipment. This makes them ideal for facilities with limited space.
- Reduced Maintenance: The absence of moving parts in the pipeline reduces the need for maintenance, as there are fewer components that can wear out or break. This results in lower maintenance costs and increased system reliability.
- Energy Efficiency: Pneumatic conveying systems can be designed to operate efficiently, using less energy than traditional mechanical conveyors. This results in lower operating costs and reduced environmental impact.
Applications in the Food Industry
Food pneumatic conveying systems are used in a variety of applications within the food industry. These include:
- Transporting Raw Materials: Pneumatic conveying systems are used to transport raw materials, such as powders and granules, from storage to processing equipment. This includes ingredients like flour, sugar, and other food additives.
- Processing and Packaging: The systems are used to transport processed food products, such as baked goods, snacks, and other packaged items, from processing lines to packaging equipment. This ensures that the products are handled hygienically and efficiently.
- Waste Management: Pneumatic conveying systems can be used to transport waste materials from processing lines to waste disposal facilities. This helps to maintain a clean and hygienic environment in the facility.
- Quality Control: The systems can be used to transport samples from quality control stations to testing laboratories. This allows for efficient and hygienic sample collection and analysis.
Conclusion
Food pneumatic conveying systems are an essential component of modern food processing facilities. They offer a hygienic, efficient, and flexible solution for transporting bulk materials, ensuring product safety and quality. HeadPowder Engineering, with its expertise in designing and manufacturing these systems, provides reliable solutions for businesses in the food industry. By understanding the structural components and working principles of these systems, industry professionals can make informed decisions about implementing pneumatic conveying solutions in their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
