Dry pebble air-flow conveying is a specialized technology used in material handling and processing industries. This method involves transporting dry pebbles or similar granular materials through a pipeline using air as the conveying medium. The process is efficient, dust-free, and suitable for various applications where traditional mechanical conveyors may not be ideal. Understanding the basics of this technology, including its structural components and operational principles, is crucial for optimizing material transport in industrial settings.
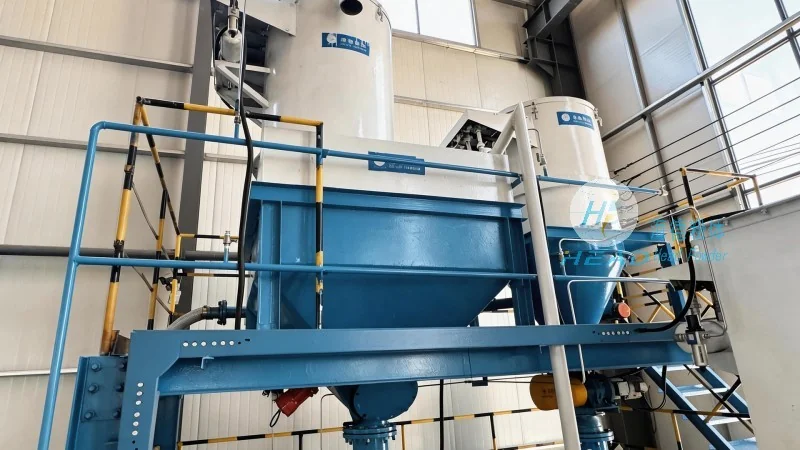
At the core of a dry pebble air-flow conveying system are several critical components that work in tandem to ensure effective material transport. The primary components include the material feed hopper, the air compressor or blower, the conveying pipeline, and the discharge unit. Each component plays a vital role in the overall functionality of the system.
The material feed hopper is responsible for storing and feeding the dry pebbles into the system. It is typically designed with a hopper or bin that can hold a sufficient quantity of material to maintain a steady flow. The hopper is equipped with a feed mechanism, such as a rotary valve or a screw feeder, which controls the rate at which the pebbles are introduced into the pipeline. This control is essential to prevent overloading and ensure consistent air flow.
The air compressor or blower generates the necessary air pressure to move the pebbles through the pipeline. Depending on the system's requirements, different types of compressors can be used, including positive displacement blowers or centrifugal fans. The air pressure must be sufficient to overcome the resistance in the pipeline and lift the pebbles, ensuring they are transported to the desired destination. The compressor is often equipped with controls to adjust the air flow rate, allowing for flexibility in handling different material loads.
The conveying pipeline is the main channel through which the pebbles and air travel. It is typically made of durable materials like stainless steel or plastic, which can withstand the abrasive nature of the pebbles and the pressure of the air. The pipeline is designed with smooth bends and transitions to minimize friction and pressure loss. The length and diameter of the pipeline are carefully selected based on the material's characteristics and the required conveying distance. Proper pipeline design is crucial to maintain the efficiency and reliability of the system.
The discharge unit is where the conveyed pebbles are collected and discharged from the system. This unit can be a hopper, a bin, or a conveyor system, depending on the downstream application. The discharge unit is equipped with a valve or a gate to control the release of the material. In some cases, the discharge unit may also include a dust collection system to prevent air leakage and maintain a clean working environment.
The operational principle of dry pebble air-flow conveying is based on the use of air to create a low-pressure zone within the pipeline, which draws the pebbles into the flow. As the air moves through the pipeline, it carries the pebbles along with it, forming a dense phase flow. The velocity of the air must be sufficient to lift the pebbles and keep them suspended in the air stream. The system operates by creating a continuous flow of air and material, which is maintained by the feed mechanism and the compressor.
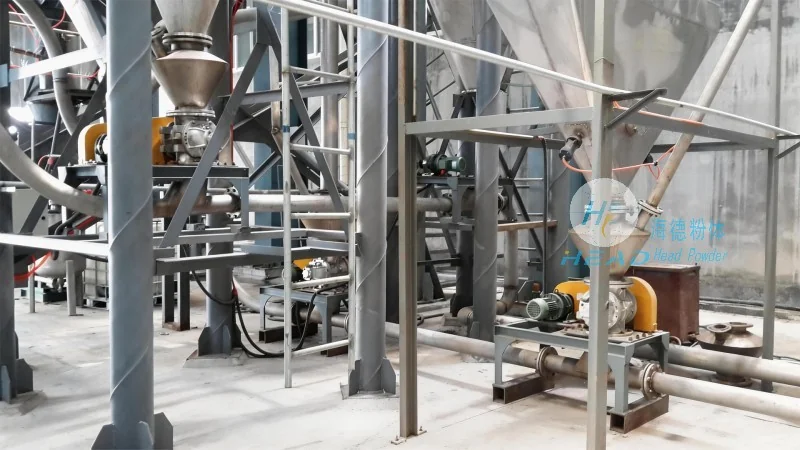
The process begins with the material being fed from the hopper into the pipeline. The air compressor then supplies the necessary air pressure, which creates a pressure differential between the inlet and the outlet of the pipeline. This pressure differential causes the air to flow through the pipeline, carrying the pebbles along. The pebbles are transported in a dense phase, meaning that they are in close contact with the air, which helps to maintain their suspension and prevent clogging.
The conveying speed and distance are determined by the air velocity and the pipeline characteristics. Higher air velocities can transport materials over longer distances, but they also increase energy consumption. Therefore, the system is designed to balance the conveying speed with energy efficiency. The material's density, size, and shape also affect the conveying performance, as these factors influence the air resistance and the required air pressure.
The system is typically operated in a closed loop, where the air is recirculated after the material is discharged. This helps to maintain a consistent air pressure and temperature, reducing energy waste and improving overall efficiency. The closed-loop system also helps to minimize dust emissions, as the air is filtered before being returned to the compressor.
Dry pebble air-flow conveying is widely used in various industries due to its advantages over traditional mechanical conveyors. The technology is particularly suitable for transporting abrasive materials, such as pebbles, gravel, or crushed stone, which can cause wear and tear on mechanical components. The air-flow system eliminates the need for moving parts in contact with the material, reducing maintenance costs and increasing the system's lifespan.
Another significant benefit of this technology is its ability to handle materials with varying sizes and shapes. The system can transport a mix of different pebbles without the risk of clogging or blockages, which is common in mechanical conveyors. This makes it ideal for applications where the material composition changes frequently, such as in mining or construction sites.
The dust-free operation of the dry pebble air-flow conveying system is another key advantage. Unlike mechanical conveyors, which can generate significant dust and particulate matter, the air-flow system keeps the material enclosed within the pipeline, preventing dust from escaping into the environment. This not only improves workplace safety but also reduces the need for dust control measures, such as filtration systems.
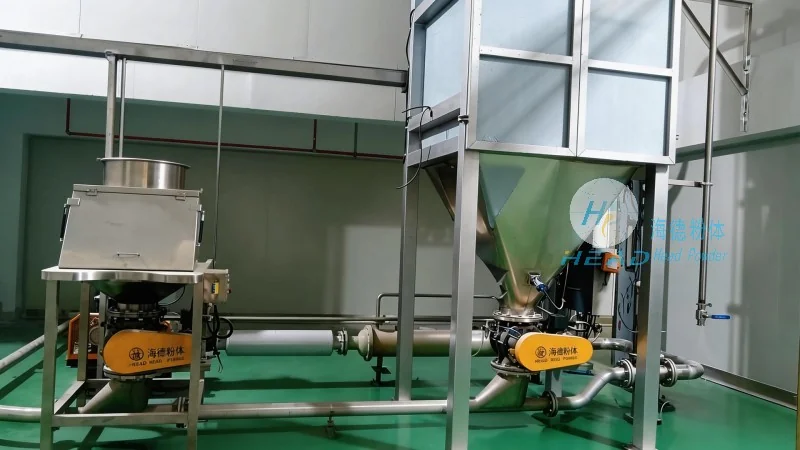
Energy efficiency is also a major benefit of this technology. By using air as the conveying medium, the system can achieve high material throughput with lower energy consumption compared to mechanical conveyors. The closed-loop design further enhances energy efficiency by recirculating the air, reducing the need for constant air intake from the environment.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of dry pebble air-flow conveying systems. The company specializes in designing, manufacturing, and installing customized conveying solutions for various industrial applications. With years of experience in the material handling industry, headpowder has developed a reputation for quality, reliability, and innovation.
Headpowder's team of engineers and technicians is dedicated to providing comprehensive solutions that meet the specific needs of their clients. The company's products are designed to be durable, efficient, and easy to maintain, ensuring long-term performance and low operational costs. Headpowder's commitment to customer satisfaction is reflected in their after-sales support services, which include installation, training, and technical assistance.
Headpowder's headquarters is located in Shandong, China, where the company has a state-of-the-art manufacturing facility. The facility is equipped with advanced machinery and equipment, allowing the company to produce high-quality conveying systems that meet international standards. The company also maintains a strong focus on research and development, continuously improving their products to stay ahead of industry trends and customer demands.
Headpowder's products are used in a wide range of industries, including mining, construction, and manufacturing. The company's solutions are tailored to the unique requirements of each industry, ensuring optimal performance and efficiency. Whether it's a small-scale conveying system for a local business or a large-scale system for an industrial plant, headpowder has the expertise and resources to deliver the right solution.
Dry pebble air-flow conveying is a highly effective and efficient technology for transporting dry pebbles and similar materials. The system's structural components and operational principles work together to provide a reliable and durable solution for various industrial applications. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., this technology continues to evolve, offering improved performance and energy efficiency. As the demand for efficient material handling solutions grows, dry pebble air-flow conveying remains a valuable option for industries seeking to optimize their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top