Chocolate pneumatic conveying systems are essential equipment in the chocolate manufacturing industry, designed to efficiently transport chocolate powders and other related materials from one location to another within a production facility. This technology offers a hygienic, dust-free, and energy-efficient method for handling chocolate, which is crucial for maintaining product quality and ensuring a clean working environment. The following sections will provide an overview of the basic structure and working principles of these systems, highlighting key components and their functions.
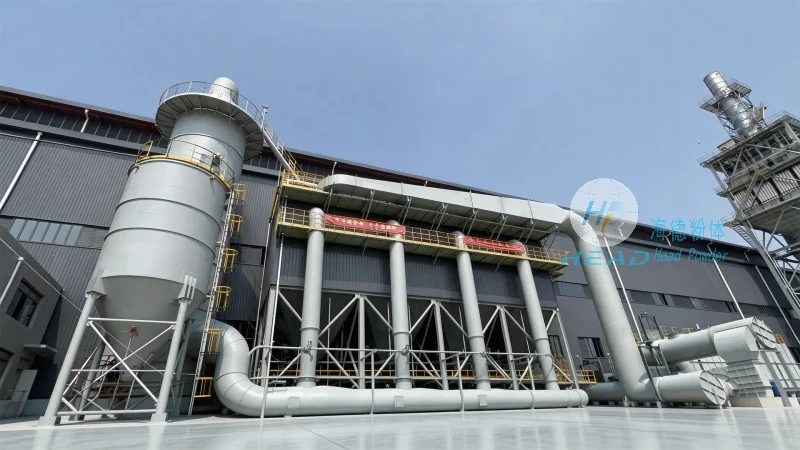
The core components of a chocolate pneumatic conveying system typically include a hopper for material storage, a conveyor line (either positive or negative pressure), a filter system to capture fine particles, and a receiver for the discharged material. The hopper is designed to hold the chocolate powder, ensuring a consistent feed into the system. It often features a discharge valve to control the flow rate of the material. The conveyor line can operate under positive pressure, where air is forced through the system to draw material into the line, or under negative pressure, where air is extracted to pull material from the source. The filter system is critical for maintaining air quality and preventing dust contamination, which is vital in food processing environments. The receiver collects the conveyed material and may include a discharge mechanism to transfer it to the next stage of production.
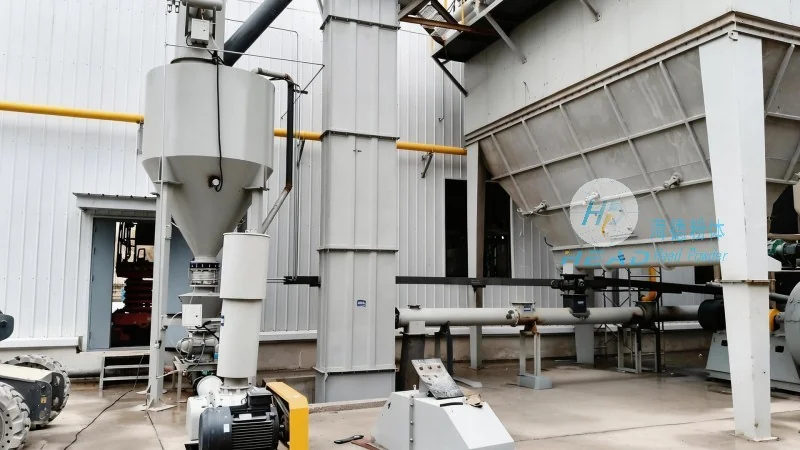
The operation of a chocolate pneumatic conveying system involves several steps. First, the chocolate powder is fed into the hopper from a storage silo or batch mixer. The material is then drawn or pushed into the conveyor line by the air flow. In positive pressure systems, a blower or fan generates the necessary air pressure to move the material through the pipeline. The air and material mixture travels through the conveying line, which may include bends, expansions, and restrictions to control the flow velocity and pressure. The material is separated from the air at the receiver, where the air is filtered and the chocolate powder is collected. The filter system ensures that any fine particles are captured, preventing them from being released into the environment. The system is designed to handle the specific characteristics of chocolate powder, such as its density, flowability, and hygroscopic properties, to ensure efficient and reliable operation.
Implementing chocolate pneumatic conveying systems in production facilities offers several advantages. Firstly, it provides a hygienic and dust-free method of material handling, which is essential for maintaining food safety standards. The enclosed system prevents contamination from external sources and reduces the risk of product spoilage. Secondly, it improves operational efficiency by reducing the need for manual handling and minimizing downtime due to material blockages. The system can handle large volumes of chocolate powder quickly and consistently, supporting high production throughput. Additionally, the energy efficiency of pneumatic conveying systems makes them a cost-effective solution compared to traditional mechanical conveyors. The ability to control the flow rate and pressure allows for precise material transfer, ensuring that the chocolate powder reaches the desired destination without degradation or loss.
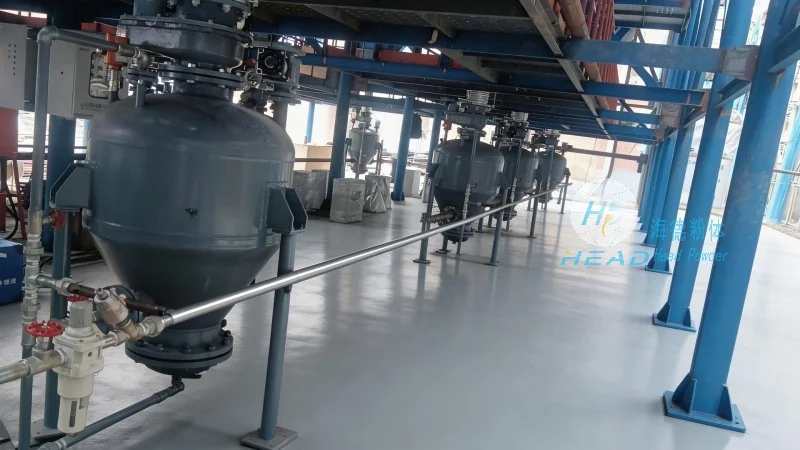
Chocolate pneumatic conveying systems are widely used in various stages of chocolate production. They are commonly employed to transport chocolate powder from storage silos to mixing tanks, from mixing to refining processes, and from refining to packaging lines. The systems can also be used to transfer ingredients such as cocoa solids, sugar, and milk powder into the production line. In each application, the system ensures that the material is handled gently to preserve its quality and texture. For example, during the mixing stage, the consistent flow of chocolate powder into the mixer helps achieve a uniform blend, which is critical for the final product's taste and appearance. In the refining stage, the precise control of material transfer ensures that the chocolate particles are processed evenly, resulting in a smooth and creamy texture. The versatility of these systems makes them suitable for different production scales, from small-scale artisanal chocolate makers to large industrial manufacturers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top