HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced dust and powder conveying systems. These systems are crucial for industries dealing with bulk materials, ensuring efficient and safe transportation of powders and fine particles. The following content provides a detailed overview of the operational process and working principles of such equipment, highlighting the technical aspects and practical applications.
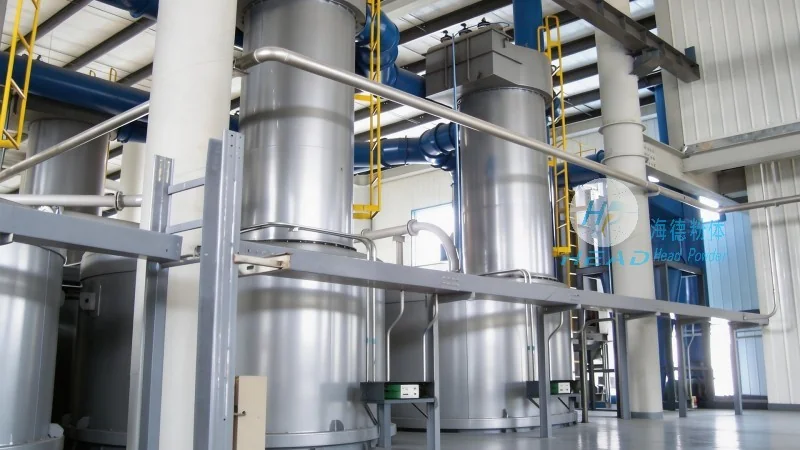
Dust and powder conveying systems are engineered to handle the movement of dry, granular, or fine materials from one location to another within industrial settings. These systems are essential in sectors like pharmaceuticals, food processing, chemical manufacturing, and mining, where precise and reliable material handling is critical. The primary goal of these systems is to transport materials with minimal loss, maintain product integrity, and ensure operational safety. HeadPowder's expertise lies in developing customized solutions that meet the specific requirements of various industries, optimizing both performance and cost-effectiveness.
The dust powder conveying system typically consists of several core components that work in tandem to achieve efficient material transport. These components include a feeding device, a conveying mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), a control system, and a discharge unit. Each component plays a vital role in the overall operation, ensuring smooth and continuous material flow. The feeding device, often a hopper or a rotary valve, regulates the input of material into the system, preventing overloading and maintaining consistent flow rates. The conveying mechanism is the heart of the system, responsible for moving the material through the pipeline or conveyor path. Control systems, equipped with sensors and automation technology, monitor and adjust the operation parameters to maintain optimal performance. Finally, the discharge unit collects the material at the end of the conveying process, ensuring it is delivered to the intended destination without spillage or contamination.
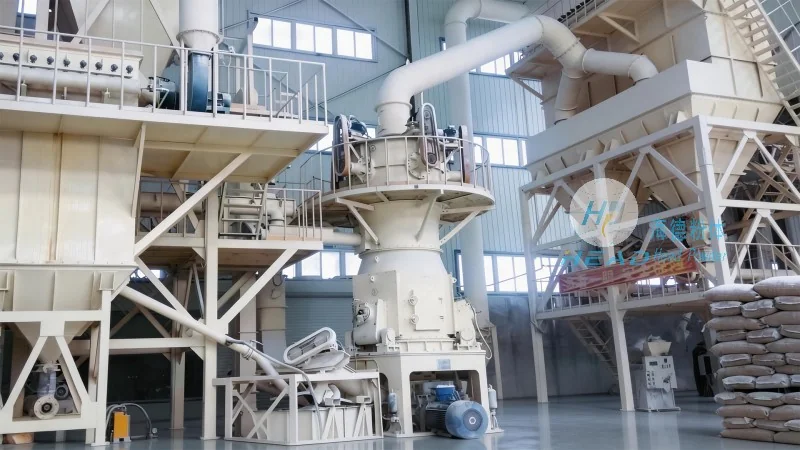
The operation of a dust powder conveying system follows a systematic sequence that ensures efficient material handling. The process begins with the material being fed into the system through the feeding device. The material then enters the conveying mechanism, where it is propelled forward by mechanical or pneumatic forces. In a screw conveyor, for example, a rotating screw pushes the material along the trough, while in a pneumatic system, compressed air or vacuum creates a flow that carries the particles through the pipeline. The control system continuously monitors the pressure, flow rate, and temperature to maintain stable operation. As the material moves through the system, it may pass through various processing stages, such as mixing, drying, or screening, depending on the application. The discharge unit then collects the material and delivers it to the next stage of production or storage. The entire process is designed to be continuous and automated, minimizing human intervention and maximizing productivity.
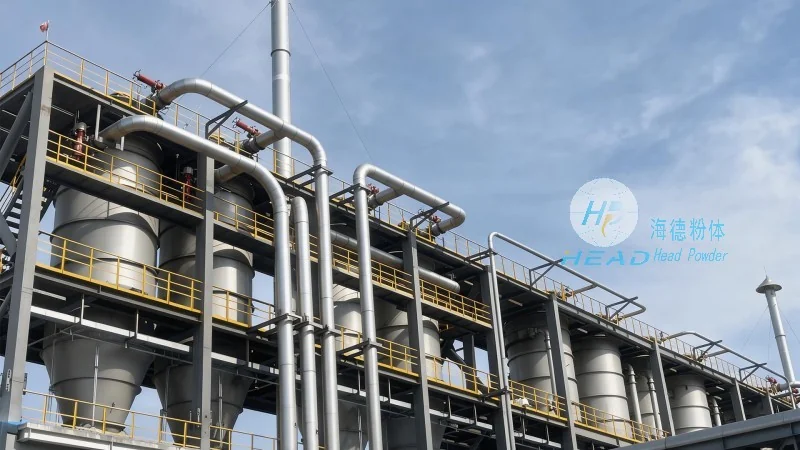
The working principle of a dust powder conveying system is based on the principles of fluid dynamics and mechanical motion. For pneumatic conveying systems, the system relies on the creation of a pressure differential to move the material. In positive pressure systems, compressed air is introduced into the pipeline, pushing the material forward. In negative pressure systems, a vacuum is created at the discharge end, pulling the material through the pipeline. The choice between positive and negative pressure depends on the material properties, such as particle size, density, and moisture content. Mechanical conveying systems, like screw or belt conveyors, utilize mechanical forces to move the material. In a screw conveyor, the rotating screw rotates and pushes the material along the trough, while in a belt conveyor, the material is carried by a moving belt. The efficiency of the system depends on the design of the conveying mechanism, the speed of operation, and the material characteristics. HeadPowder's systems are engineered to optimize these principles, ensuring high efficiency and minimal energy consumption.
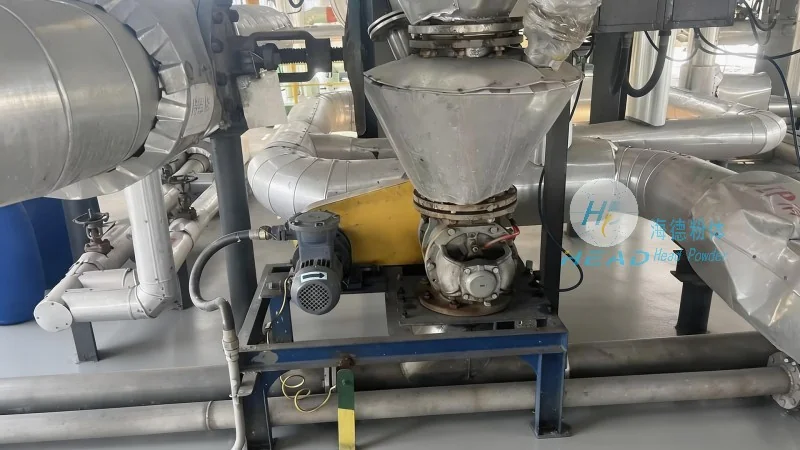
HeadPowder's dust and powder conveying systems offer several advantages that make them ideal for industrial applications. These systems are designed to handle a wide range of materials, from fine powders to bulk granules, with minimal degradation or contamination. The systems are also highly efficient, with low energy consumption and high throughput rates. Additionally, the equipment is easy to maintain and clean, ensuring long service life and reduced downtime. The use of advanced materials and manufacturing techniques ensures durability and resistance to corrosion and wear. HeadPowder's customized solutions are tailored to meet the specific needs of each client, providing optimal performance and cost savings. The company's commitment to quality and innovation has made it a trusted partner for industries worldwide.
In conclusion, dust and powder conveying systems are essential equipment for industries dealing with bulk materials. The operation process and working principles of these systems are critical to ensuring efficient and safe material handling. HeadPowder, with its expertise and advanced technology, provides high-quality solutions that meet the diverse needs of various industries. By understanding the key components, operation process, and working principles of these systems, users can make informed decisions when selecting and implementing dust powder conveying equipment. HeadPowder's commitment to excellence ensures that its systems deliver reliable performance and contribute to the overall success of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top