Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier of calcined limestone powder conveying systems. The company is based in Shandong, China, and specializes in providing efficient and reliable equipment for the transportation of calcined limestone powder. This article will detail the operation process and working principle of such systems, highlighting the key components and their functions.
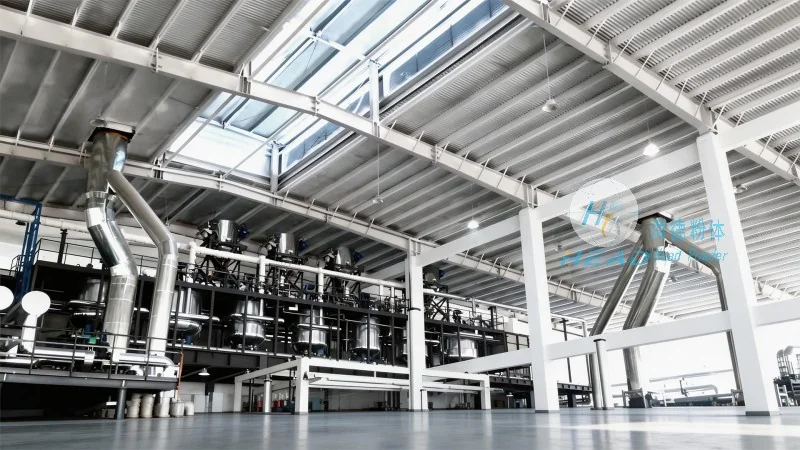
The calcined limestone powder conveying system is designed to handle the transportation of calcined limestone powder from storage silos or production lines to processing facilities. The system typically consists of several key components, including feeders, conveyors, dust collectors, and control systems. Each component plays a crucial role in ensuring the smooth and safe operation of the entire system.
1. Feeder: The feeder is responsible for controlling the flow rate of calcined limestone powder from the storage silo. It ensures a consistent and uniform feed to the conveyor, preventing blockages and maintaining system efficiency. The feeder may be a rotary valve or a screw feeder, depending on the system design.
2. Conveyor: The conveyor is the core component of the system, responsible for transporting the calcined limestone powder from the feeder to the destination. There are different types of conveyors used in such systems, including pneumatic conveyors (air-swept) and mechanical conveyors (e.g., belt conveyors). Pneumatic conveyors are commonly used for calcined limestone powder due to their ability to handle fine powders and provide a dust-free environment.
3. Dust Collector: The dust collector is essential for maintaining a clean and safe working environment. It captures any airborne dust particles generated during the conveying process and filters them before releasing the air back into the environment. This helps to comply with environmental regulations and protect the health of workers.
4. Control System: The control system monitors and regulates the operation of all components in the conveying system. It includes sensors, controllers, and indicators that allow operators to adjust the flow rate, pressure, and other parameters as needed. The control system ensures that the system operates within safe and efficient limits.
The operation process of the calcined limestone powder conveying system typically involves the following steps:
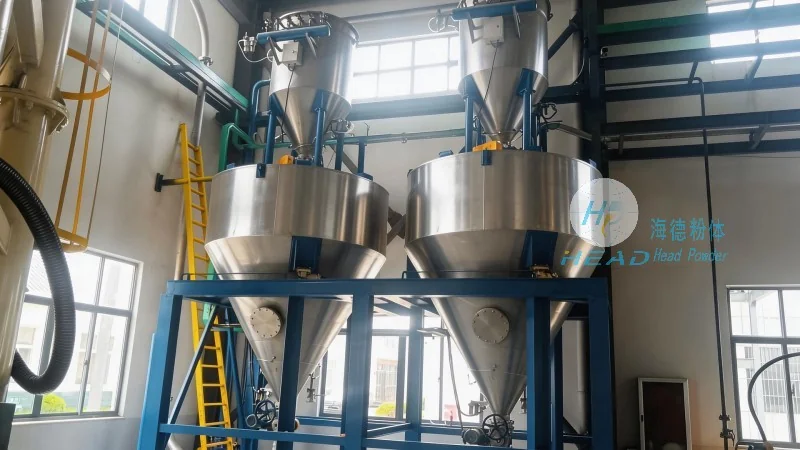
1. Raw Material Preparation: Calcined limestone powder is stored in a silo. The feeder then takes the powder from the silo and feeds it into the conveyor system.
2. Powder Conveying: The conveyor transports the calcined limestone powder from the feeder to the processing facility. In a pneumatic conveyor system, the powder is mixed with air and transported through a pipeline. The air flow is controlled to maintain the proper velocity and pressure, ensuring the powder moves smoothly without clogging.
3. Destination Delivery: The calcined limestone powder is delivered to the processing facility, where it is used in various applications such as cement production, construction materials, and chemical manufacturing.
4. Dust Control: The dust collector continuously captures any dust particles generated during the conveying process. The collected dust is then disposed of or recycled, depending on the system design.
The working principle of the calcined limestone powder conveying system is based on the principles of fluidization and pneumatic transport. In a pneumatic conveyor system, the calcined limestone powder is suspended in a stream of air and transported through a pipeline. The air flow is generated by a blower or fan, which creates a pressure difference between the inlet and outlet of the pipeline. The pressure difference causes the powder to move along the pipeline, while the air carries the powder to the destination.
The system operates by maintaining a consistent air flow rate and pressure. The feeder controls the flow rate of the powder, while the control system monitors the pressure and flow rate to ensure the system operates efficiently. The dust collector removes any dust particles from the air stream, preventing them from being released into the environment.
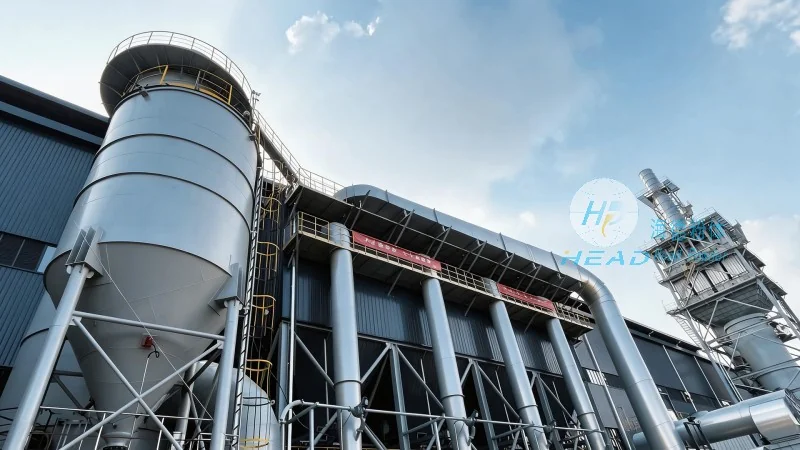
The calcined limestone powder conveying system offers several advantages over traditional methods of powder transportation. These include:
1. Efficiency: The system can transport large quantities of calcined limestone powder over long distances with minimal energy consumption.
2. Reliability: The system is designed to operate continuously without interruption, ensuring a steady supply of powder to the processing facility.
3. Dust Control: The system includes a dust collector that captures and filters dust particles, maintaining a clean and safe working environment.
4. Flexibility: The system can be customized to meet the specific requirements of different applications, such as varying flow rates or pipeline lengths.
Shandong HeadPowder Engineering Co., Ltd. provides high-quality calcined limestone powder conveying systems that are designed to meet the needs of various industries. The systems are efficient, reliable, and safe, making them an ideal choice for transporting calcined limestone powder. By understanding the operation process and working principle of such systems, users can ensure optimal performance and maintenance of the equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top