Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a prominent manufacturer of industrial dust collection and material handling systems. Headquartered in Shandong, China, the company has built a strong presence in the market by delivering high-quality, reliable equipment tailored to various industrial needs. This article delves into the operation process and working principle of material conveying systems integrated with pulse dust collectors, offering insights into how these systems function to enhance efficiency in dust removal and material transport.
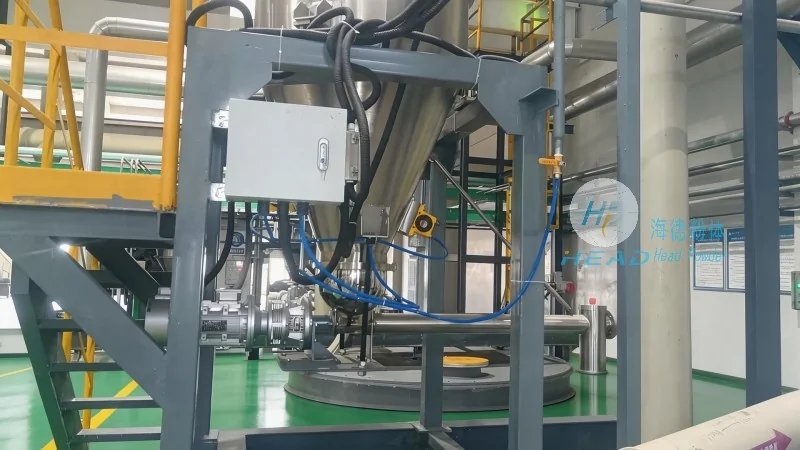
HeadPowder specializes in the design, manufacturing, and installation of advanced dust collection solutions, with a particular focus on pulse jet dust collectors. The company’s team of engineers and technicians brings extensive experience in optimizing material handling processes, ensuring that their equipment meets the stringent requirements of modern industrial applications. By combining cutting-edge technology with rigorous quality control, HeadPowder delivers systems that are not only efficient but also durable and low-maintenance. The company’s commitment to innovation has positioned it as a trusted partner for businesses seeking to improve their operational performance and reduce environmental impact.
The material conveying system within a pulse dust collector operates on the principle of integrating dust filtration with material transport. The system comprises several key components: a hopper for material storage, a conveyor (such as a screw or pneumatic conveyor) for transporting material, and a dust collection unit equipped with pulse jet cleaning technology. The process begins when raw materials are fed into the hopper. As the material flows through the conveyor, it is transported to the discharge point, where it may be transferred to a storage silo or directly fed into the next stage of the production line. Simultaneously, air is drawn into the dust collector, where particulate matter is captured by the filter media. The pulse jet mechanism then periodically cleans the filter bags by injecting high-pressure air, dislodging accumulated dust and allowing it to fall back into the hopper. This integrated approach ensures that both dust removal and material transport are optimized, minimizing downtime and maximizing productivity.
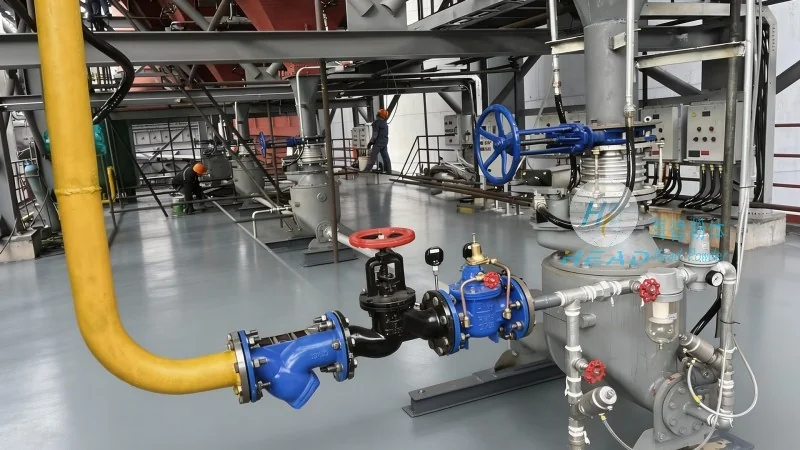
The operation process of the material conveying system in a pulse dust collector involves a series of sequential steps designed to ensure smooth and continuous operation. First, the raw material is loaded into the hopper, which acts as the initial feeding point. The material then moves through the conveyor, which can be either a mechanical screw conveyor or a pneumatic system, depending on the specific application. The conveyor transports the material to the discharge point, where it is either stored or forwarded to subsequent processing units. Meanwhile, the dust collector operates by drawing air from the material handling system, capturing dust particles on the filter bags. The pulse jet system cleans the filter bags at regular intervals, releasing collected dust back into the hopper. This cleaning cycle is controlled by a timer or pressure sensor, ensuring that the filter remains efficient and the material transport continues without interruption. The entire process is automated, reducing the need for manual intervention and enhancing operational efficiency.
Several critical components contribute to the effective operation of the pulse dust collector material conveying system. The hopper serves as the primary storage and feeding unit, providing a stable supply of material to the conveyor. The conveyor itself is responsible for transporting the material, with options including screw conveyors for solid materials and pneumatic conveyors for powders or fine particles. The dust collection unit, equipped with pulse jet cleaning technology, filters the air drawn from the system, capturing dust particles on the filter bags. The pulse jet mechanism, which uses high-pressure air to clean the filters, is a key feature that ensures the system maintains high efficiency over time. Additionally, control systems monitor the pressure and cleaning cycles, adjusting the operation to optimize performance and prevent filter clogging.
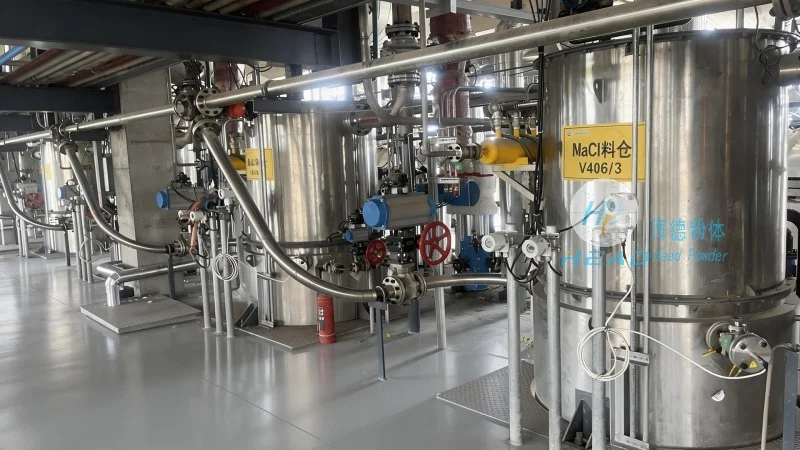
Integrating material conveying with pulse dust collection offers several advantages for industrial operations. First, it minimizes the need for separate dust collection and material handling systems, reducing equipment costs and space requirements. Second, the combined system enhances overall efficiency by ensuring that dust is removed as the material is being transported, preventing dust accumulation and improving air quality. Third, the automated cleaning process reduces maintenance time and labor costs, as the system can operate continuously with minimal intervention. Finally, the system’s reliability and durability contribute to longer operational life and lower total cost of ownership, making it an attractive solution for businesses in various industries, including manufacturing, mining, and construction.
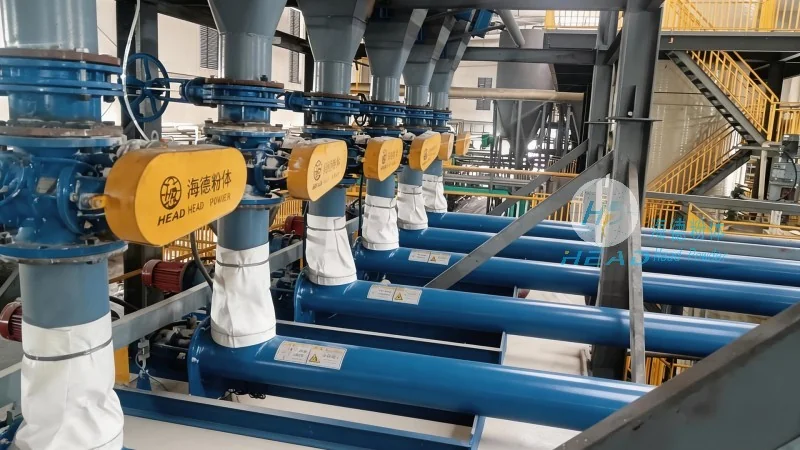
The pulse dust collector material conveying system is widely used in various industrial applications where dust and material handling are critical. For example, in cement plants, the system is used to transport raw materials and remove dust from the production process. In mining operations, it helps in handling bulk materials while controlling airborne dust, improving worker safety and environmental compliance. In food processing facilities, the system ensures that dust is effectively removed from the material handling process, maintaining hygiene standards. These applications demonstrate the versatility and effectiveness of the system in different industrial settings, highlighting its importance in modern manufacturing and processing operations.
Shandong HeadPowder Engineering Co., Ltd. provides advanced pulse dust collector material conveying systems that combine efficient dust removal with reliable material transport. By integrating key components such as hoppers, conveyors, and pulse jet cleaning mechanisms, the company’s solutions enhance operational efficiency, reduce maintenance costs, and improve overall productivity. The company’s expertise and commitment to quality ensure that its systems meet the demanding requirements of modern industrial applications, making it a trusted partner for businesses seeking to optimize their material handling and dust control processes. With its headquarters in Shandong, China, HeadPowder continues to innovate and deliver solutions that drive success in various industrial sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top