Gas-pneumatic conveying equipment is a critical component in industrial material handling systems, particularly for the efficient transport of dust and fine particulate materials. This technology offers a reliable and flexible solution for moving materials over short to medium distances, often in environments where traditional mechanical conveying methods may be less suitable. The equipment operates by utilizing compressed air to create a flow that propels the material through a pipeline network, ensuring minimal contamination and reduced maintenance compared to other conveying systems.
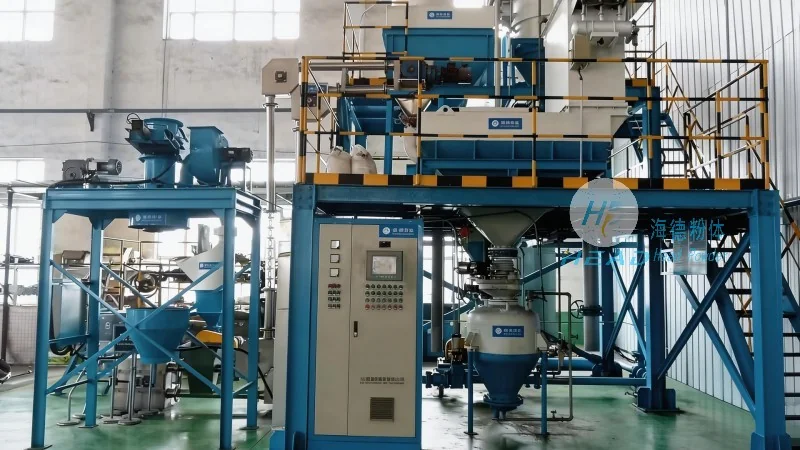
The core components of a typical dust gas-pneumatic conveying system include the material hopper, air compressor, conveying pipeline, and control valves. The material hopper serves as the storage and feeding unit, where the dust or fine particles are loaded and prepared for transport. The air compressor generates the necessary pressure to create the pneumatic flow, which is then directed into the conveying pipeline. Control valves are used to regulate the air flow and material discharge, ensuring precise control over the conveying process. Each component plays a vital role in maintaining the efficiency and safety of the system.
The operation of dust gas-pneumatic conveying equipment is based on the principle of fluidization and pneumatic transport. When compressed air is introduced into the material hopper, it creates a low-pressure zone that draws the material into the pipeline. The air flow then carries the material particles through the conveying line, maintaining a consistent velocity to prevent material settling or blockages. The system typically operates in either positive or negative pressure modes. In positive pressure systems, the air pressure is higher than the ambient air pressure, pushing the material through the pipeline. In negative pressure systems, the air pressure is lower than ambient, creating a vacuum that pulls the material. The choice between these modes depends on the material characteristics, distance to be conveyed, and system design requirements.
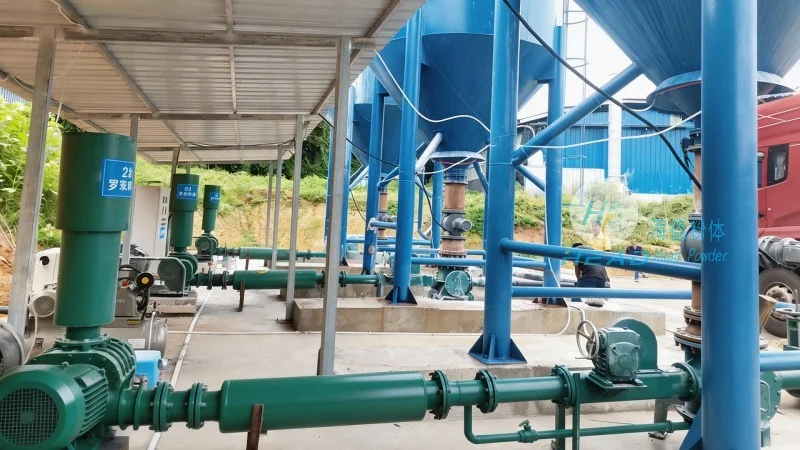
The operation process of the dust gas-pneumatic conveying equipment involves several key steps. First, the material is loaded into the hopper, ensuring a consistent feed rate. The air compressor is then activated, providing the necessary pressure to initiate the conveying process. As the compressed air enters the hopper, it fluidizes the material, allowing it to be drawn into the pipeline. The material is then transported through the conveying line, with the air flow maintaining the material in suspension. At the receiving end, the material is discharged into a collection bin or storage area. Control valves are used to regulate the air flow and material discharge, ensuring that the system operates smoothly and efficiently. The entire process is automated and can be controlled remotely, enhancing operational efficiency and reducing the need for manual intervention.
There are several advantages to implementing dust gas-pneumatic conveying equipment in industrial applications. One of the primary benefits is the ability to transport fine and dusty materials without the risk of contamination or degradation. The enclosed pipeline system prevents exposure to the environment, maintaining the quality of the material. Additionally, this technology offers flexibility in system design, allowing for multiple inlets and outlets, which is ideal for complex material handling scenarios. The equipment also requires less maintenance compared to traditional mechanical conveyors, as there are fewer moving parts and less wear and tear. Furthermore, the system can be easily scaled to accommodate varying material volumes and conveying distances, making it a versatile solution for various industrial needs.
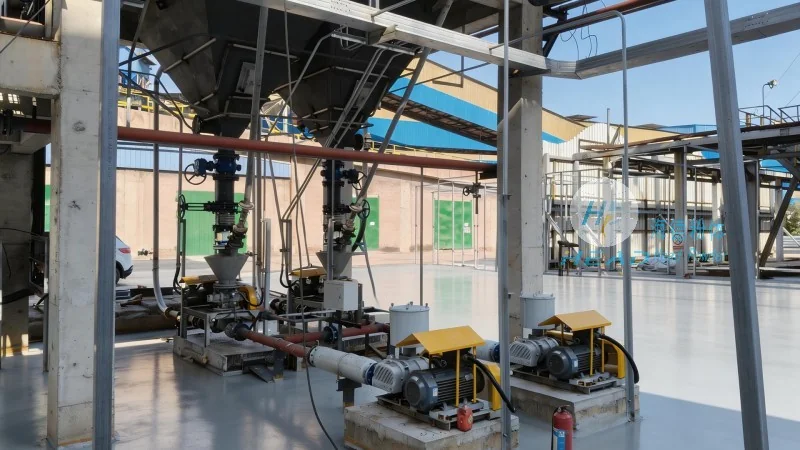
Dust gas-pneumatic conveying equipment is widely used in various industries, including pharmaceuticals, food processing, and chemical manufacturing. In the pharmaceutical industry, it is used to transport fine powders and granules, ensuring that the materials remain sterile and free from contamination. In food processing, the equipment is employed to handle ingredients such as flour, sugar, and spices, maintaining the quality and safety of the products. In chemical manufacturing, it is used to transport powders and granules, which may be hazardous or sensitive to moisture. The equipment is also used in the mining and mineral processing industries to transport ore and other materials from processing plants to storage facilities. These applications highlight the versatility and reliability of the dust gas-pneumatic conveying system in handling diverse material types and operational requirements.
Proper maintenance and operational considerations are essential to ensure the longevity and efficiency of the dust gas-pneumatic conveying equipment. Regular cleaning of the hopper and pipeline is necessary to prevent material buildup and blockages. The air compressor should be checked regularly for proper pressure and air quality, as contaminants can affect the performance of the system. The control valves and sensors should be inspected to ensure they are functioning correctly, as any malfunction can lead to system inefficiencies or safety issues. Additionally, the system should be monitored for air leaks and pressure fluctuations, as these can impact the conveying process. By following proper maintenance procedures and operational guidelines, the equipment can operate reliably and efficiently for extended periods.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top