HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for various agricultural products, including barley. This article explores the fundamental principles behind these systems and highlights key working scene characteristics that make them efficient and reliable in handling barley and similar bulk materials.
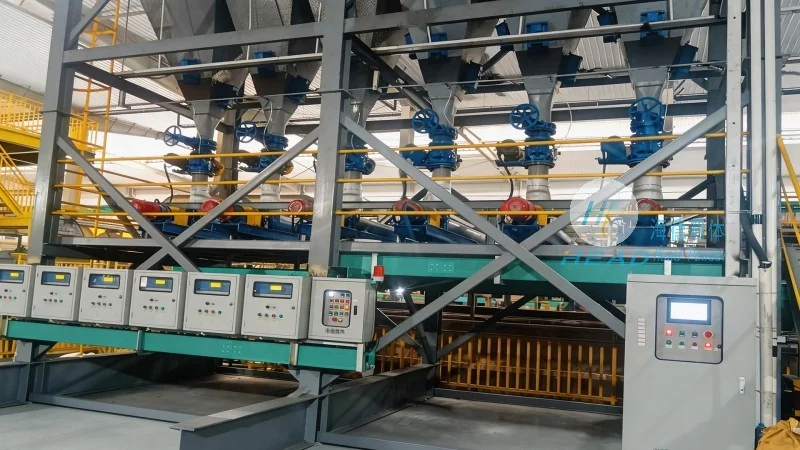
Pneumatic conveying systems operate on the principle of transporting bulk materials like barley through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical conveyors, which rely on mechanical components such as belts or screws, pneumatic systems utilize pressure differentials to move materials. The process typically involves a hopper where barley is stored, a blower or compressor that generates the necessary airflow, and a pipeline network that directs the material to its destination. The system can be categorized into two main types: dilute-phase and dense-phase, each with distinct characteristics suitable for different operational needs. Dilute-phase systems use higher air velocities to transport materials in a suspended state, while dense-phase systems employ lower velocities to move material in a more compacted form, reducing the risk of product degradation and blockages.
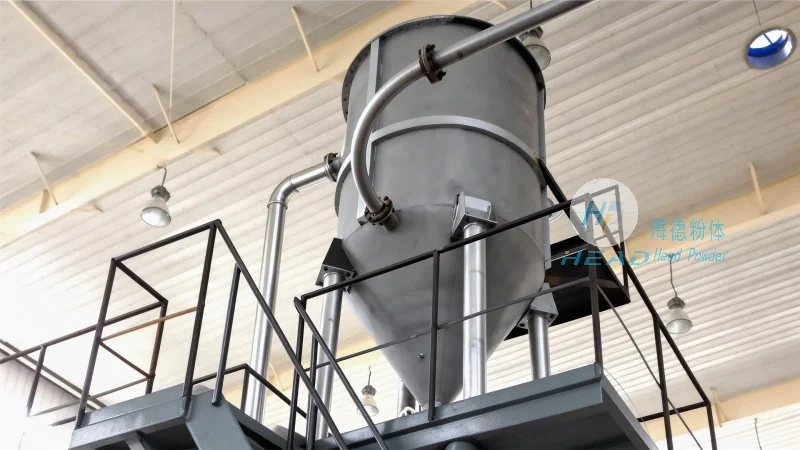
The effectiveness of a barley pneumatic conveying system is heavily influenced by several working scene characteristics that must be considered during design and operation. First, the material's physical properties, such as particle size, density, and moisture content, play a critical role. Barley, with its relatively uniform particle size and moderate density, is well-suited for pneumatic transport, but variations in these properties can affect system performance. Second, the system's layout and the distance between the source and destination points are crucial. Longer conveying distances may require additional boosters or larger-diameter pipelines to maintain adequate airflow and prevent pressure losses. Third, the need for product handling in different environments, such as on-farm storage, processing facilities, or grain elevators, dictates the system's configuration. For instance, on-farm applications may involve short-distance transport from storage bins to processing equipment, while industrial facilities might require longer-distance transport between different processing stages. Additionally, the system's integration with other equipment, such as cleaning or sorting machines, is essential for maintaining product quality and operational efficiency. The ability to handle varying throughput rates and adapt to different operational conditions is another key characteristic, ensuring that the system can meet the demands of fluctuating production schedules.
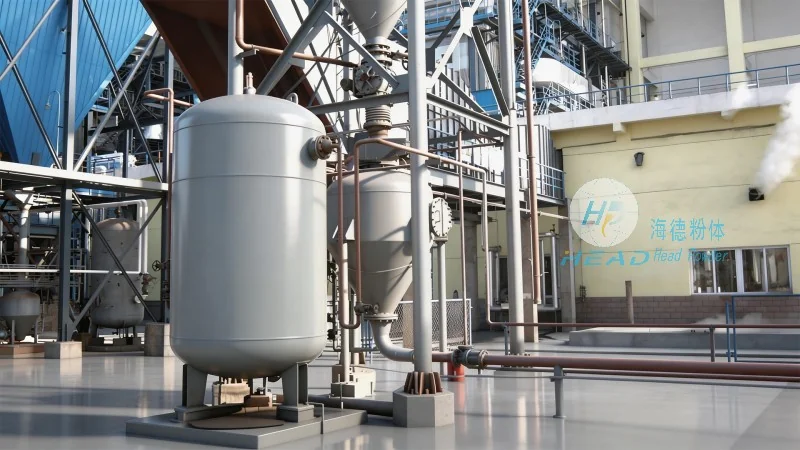
Barley pneumatic conveying systems are widely used in various agricultural and industrial settings due to their versatility and efficiency. In on-farm operations, these systems are commonly employed to transport barley from storage silos to processing equipment, such as malting or milling facilities. The ability to handle large volumes of barley with minimal manual intervention makes them ideal for modern farming operations. In industrial processing plants, pneumatic conveying systems are integrated into larger production lines, where barley is conveyed between different processing stages, such as cleaning, sorting, and grinding. The systems' ability to maintain product integrity and prevent contamination is particularly important in these applications. Additionally, the systems are used in grain elevators and bulk handling facilities to transport barley from storage areas to loading docks or transportation vehicles. The flexibility of pneumatic conveying systems allows them to adapt to different operational requirements, making them a preferred choice for handling barley in diverse working environments.
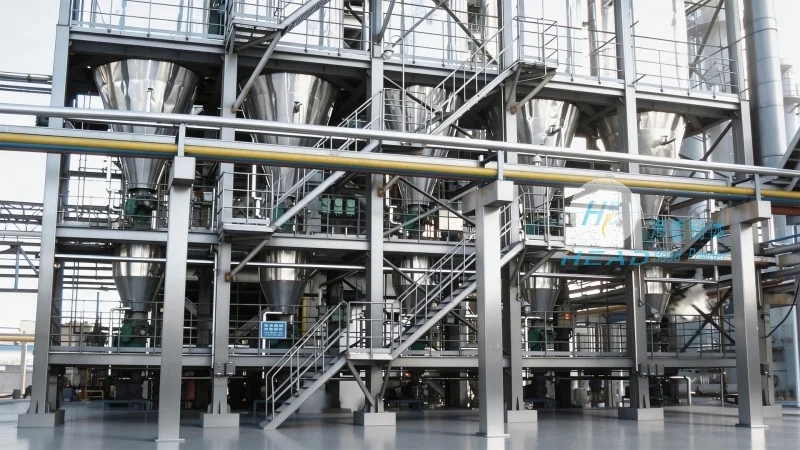
HeadPowder's expertise in designing and implementing barley pneumatic conveying systems ensures that clients receive tailored solutions that meet their specific operational needs. By understanding the fundamental principles of pneumatic transport and considering key working scene characteristics, the company provides efficient and reliable systems that enhance productivity and product quality. With a focus on innovation and customer satisfaction, HeadPowder continues to be a leader in the agricultural engineering sector, delivering high-quality pneumatic conveying solutions for barley and other bulk materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top