Positive pressure dilute phase pneumatic conveying systems represent a sophisticated technology in material handling, offering efficient and flexible solutions for transporting bulk materials over varying distances. This system operates by using compressed air to move particles through a pipeline, creating a dilute phase where the material is suspended in the air stream. The positive pressure design ensures that the system maintains a consistent pressure above atmospheric, which is crucial for preventing material backflow and maintaining a stable conveying process.
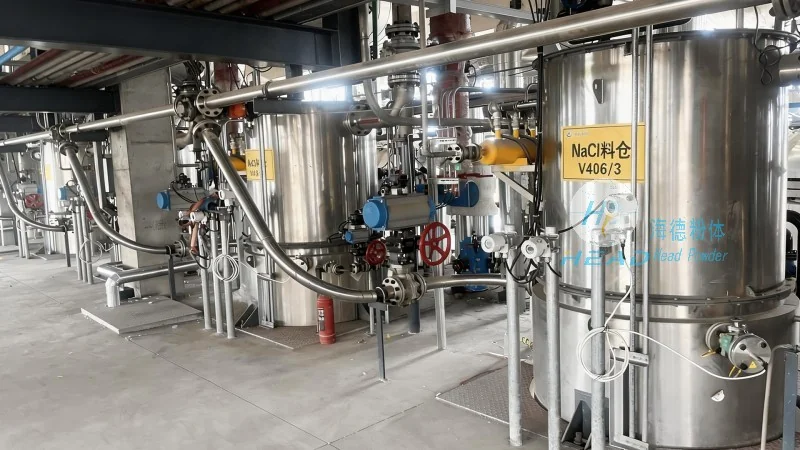
The fundamental principle of this system involves the generation of a high-pressure air stream that propels the material particles through a pipeline. Unlike negative pressure systems, which draw material into the system, positive pressure systems actively push the material forward. The air is typically introduced at the inlet of the conveying line, creating a low-resistance environment that allows the material to be suspended and transported efficiently. The system's design ensures that the air velocity is sufficient to keep the particles in a suspended state, minimizing particle deposition and ensuring smooth material flow.
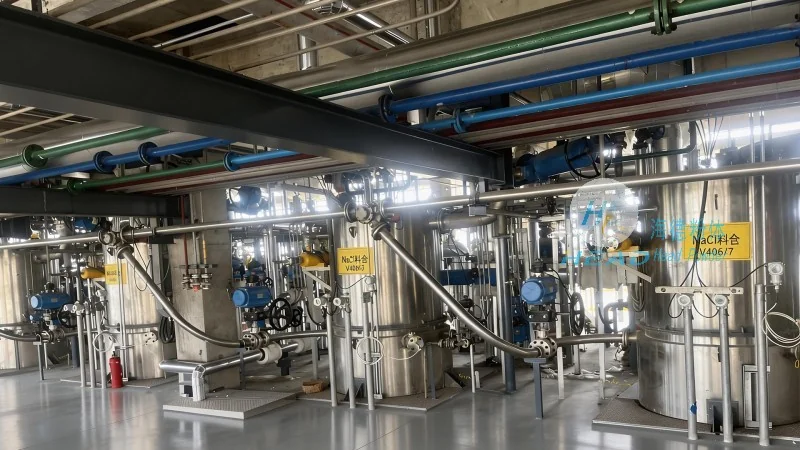
Positive pressure dilute phase systems are particularly well-suited for a variety of industrial applications where material handling demands precision and reliability. These systems are commonly used in industries such as food processing, pharmaceuticals, chemicals, and minerals, where the need to handle fine or sensitive materials without degradation is critical. The working scene characteristics include the ability to transport materials over long distances with minimal loss, maintain consistent material quality, and adapt to different material types and particle sizes. For instance, in food processing facilities, these systems can transport powders like flour, sugar, or spices without contamination or degradation, ensuring product integrity. In pharmaceutical industries, the positive pressure design helps maintain a sterile environment, preventing cross-contamination and ensuring compliance with regulatory standards.
One of the key advantages of positive pressure dilute phase pneumatic conveying is its high efficiency in material transport. The system can handle a wide range of materials, from fine powders to granules, with minimal maintenance requirements. The positive pressure design reduces the risk of material blockages and ensures continuous operation, which is essential for industrial production lines. Additionally, the system's ability to handle varying material flow rates makes it adaptable to different production needs, providing flexibility in material handling. The use of compressed air as the conveying medium also allows for easy integration with existing production systems, reducing the need for extensive modifications to the facility.
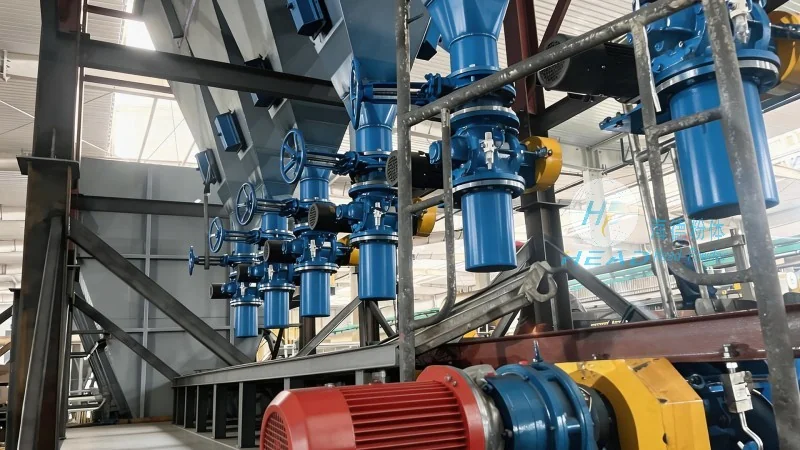
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced material handling systems, including positive pressure dilute phase pneumatic conveying solutions. With a focus on innovation and customer-centric solutions, the company has established itself as a leading provider in the industry. Headpowder's expertise lies in tailoring systems to meet specific client requirements, ensuring that each project is customized to optimize material transport efficiency and operational performance. The company's facilities are located in Shandong, China, where it leverages local resources and expertise to deliver high-quality products and services.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top