Nitrogen-protected material pneumatic conveying systems represent a sophisticated approach to material handling, particularly in industries where maintaining product integrity and preventing contamination is paramount. These systems utilize nitrogen gas as a protective medium to transport bulk materials through a sealed pipeline network. The core principle revolves around creating an inert gas environment that isolates the conveyed material from atmospheric oxygen and moisture, thereby preserving its quality and preventing oxidation or degradation during transit.
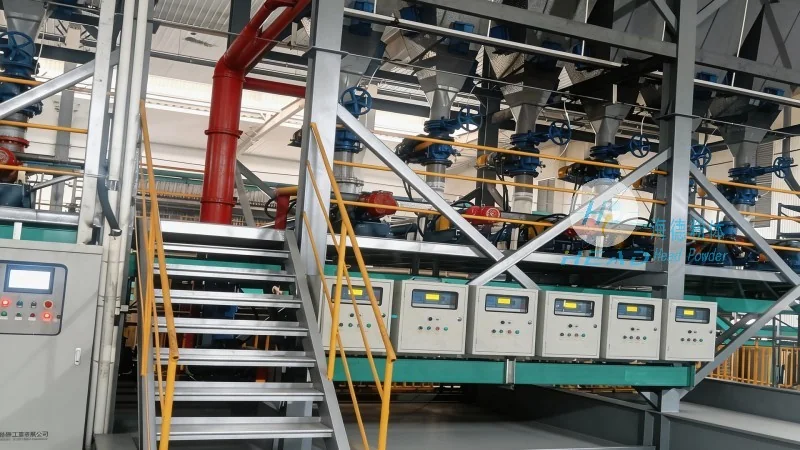
The fundamental mechanism of a nitrogen-protected pneumatic conveying system involves several key components and processes. At its heart is a nitrogen gas source, typically a high-purity nitrogen generator or a dedicated supply system, which provides the inert gas required to create a protective atmosphere. The system includes a hopper or feed hopper where the material is loaded, followed by a feeder that controls the material flow into the conveying line. As the material is introduced, it is entrained by the high-velocity nitrogen stream, forming a dense or dilute phase flow depending on the system design and material characteristics.
The conveying line itself is constructed from materials resistant to both the conveyed material and the nitrogen gas, ensuring durability and preventing leaks that could compromise the protective environment. At the discharge end, the material is deposited into a receiving container, while the nitrogen gas is either recycled back into the system or safely vented. This closed-loop operation minimizes gas consumption and maintains the integrity of the nitrogen atmosphere throughout the conveying process.
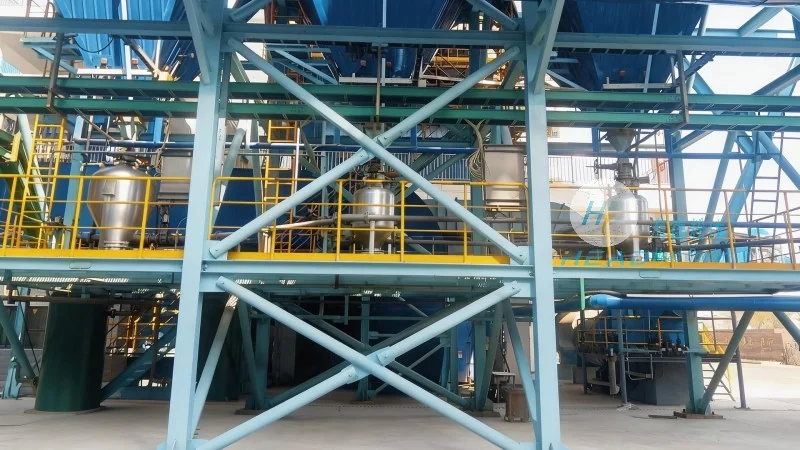
Several critical components work in tandem to ensure the efficient and reliable operation of a nitrogen-protected pneumatic conveying system. The nitrogen gas supply unit, which may include a compressor, dryer, and purification system, ensures the gas is of the required purity and pressure. The material feed system, comprising hoppers, feeders (such as rotary valves or screw feeders), and any necessary pre-processing equipment, controls the material flow rate and consistency. The conveying line, often made of stainless steel or other corrosion-resistant materials, is designed to handle the specific properties of the conveyed material, including its density, flowability, and potential for abrasion.
At the receiving end, a dust collector or filter may be integrated to capture any fine particles that escape, maintaining air quality and preventing contamination. Additionally, pressure sensors and flow meters are typically installed to monitor system performance and ensure optimal operation. These components collectively contribute to the system's ability to maintain a stable, inert environment while efficiently transporting the material.
The working scene characteristics of nitrogen-protected pneumatic conveying systems are tailored to specific industrial needs, making them suitable for a wide range of applications. These systems are particularly advantageous in industries where material quality is critical, such as pharmaceuticals, food processing, and electronics manufacturing. In pharmaceutical applications, for example, the system can prevent contamination of sensitive drugs during transport, ensuring compliance with stringent regulatory standards.
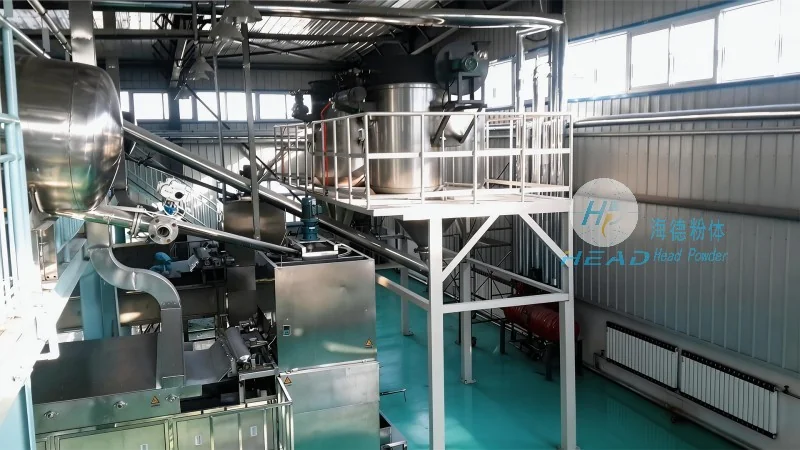
In the food industry, nitrogen-protected conveying is used to maintain the freshness and quality of products like powders, grains, and spices, preventing oxidation and spoilage. Similarly, in the electronics sector, the system protects sensitive components from moisture and dust, which could compromise their functionality. The system's ability to handle a variety of materials, from fine powders to bulk solids, makes it versatile across different industries.
Implementing a nitrogen-protected material pneumatic conveying system offers several advantages that enhance operational efficiency and product quality. One of the primary benefits is the preservation of material integrity, as the inert nitrogen atmosphere prevents oxidation, moisture absorption, and contamination. This is crucial for products that are sensitive to environmental factors, ensuring that the final product meets the required specifications.
Another key advantage is the system's ability to handle a wide range of materials, including those that are abrasive, corrosive, or prone to caking. The sealed pipeline design minimizes material degradation and reduces the risk of blockages or system failures. Additionally, the system can operate in a closed loop, reducing nitrogen gas consumption and lowering operational costs over time.
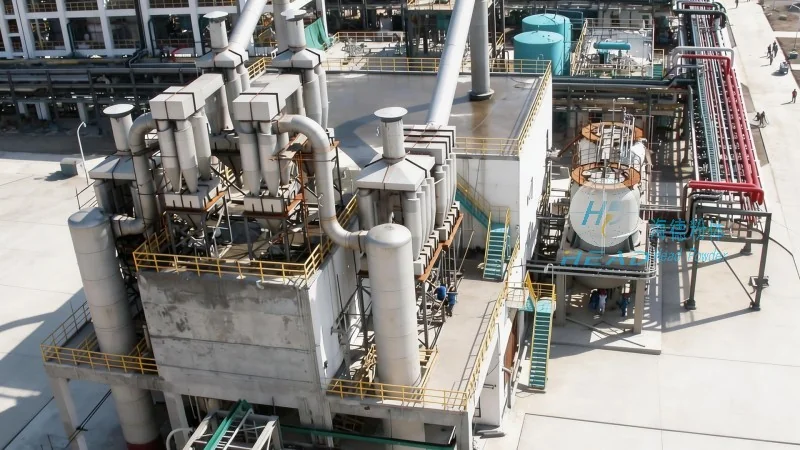
From an operational perspective, nitrogen-protected conveying systems offer improved safety and hygiene. By eliminating the need for manual handling of bulk materials, the risk of workplace accidents and cross-contamination is significantly reduced. The sealed environment also helps in maintaining a clean and controlled workspace, which is essential in industries like food and pharmaceuticals.
Overall, nitrogen-protected material pneumatic conveying systems represent a highly effective solution for industries requiring precise material handling with minimal risk to product quality. The combination of inert gas protection and efficient conveying technology ensures that materials are transported safely and efficiently, meeting the demands of modern industrial processes. When considering such a system, it is essential to evaluate the specific material properties, operational requirements, and environmental factors to ensure optimal performance and cost-effectiveness.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top