For industrial applications involving desulfurization processes, the efficient handling of sodium bicarbonate materials is crucial. Pneumatic conveying systems have emerged as a reliable method to transport these materials, offering advantages such as reduced equipment wear, improved safety, and enhanced process control. This article explores the fundamental principles behind pneumatic conveying for desulfurization sodium bicarbonate materials and highlights the key characteristics of working scenes where this technology is effectively applied.
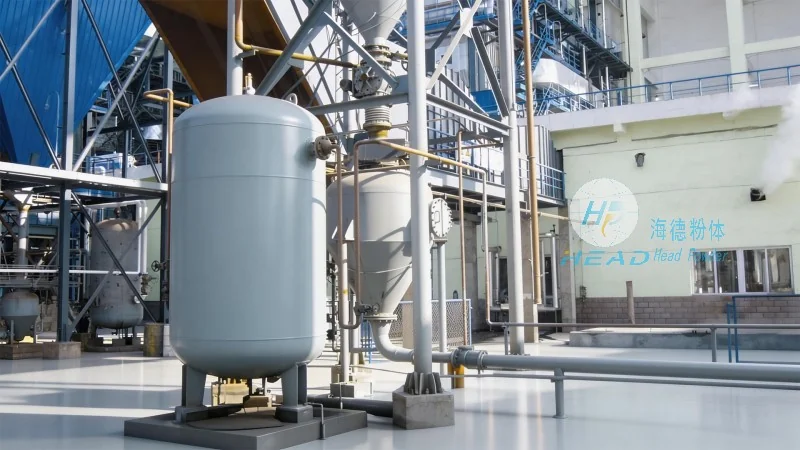
Pneumatic conveying operates by using air or gas to transport bulk materials through a pipeline. The system typically consists of a blower or compressor to generate the necessary airflow, a hopper to store the material, and a conveying line. For desulfurization sodium bicarbonate, which is often in a powder or granular form, the choice of conveying method—whether positive pressure or negative pressure—depends on factors like material properties, distance, and system complexity. Positive pressure systems push air and material through the line, while negative pressure systems draw material into the line using a vacuum. In the case of sodium bicarbonate, which can be abrasive and prone to dust generation, the selection of appropriate equipment, such as rotary valves and cyclone separators, is critical to ensure efficient and safe operation. The conveying velocity and pressure are carefully controlled to prevent material degradation and maintain system performance. By understanding these principles, industrial operators can optimize the pneumatic conveying process for their specific desulfurization applications.
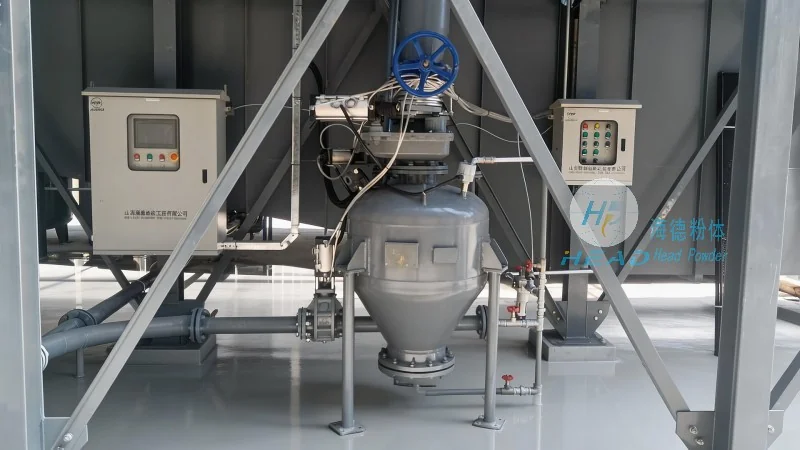
The effectiveness of pneumatic conveying for desulfurization sodium bicarbonate is heavily influenced by the working scene characteristics. These include the scale of the operation, the distance between the source and destination, the environmental conditions, and the integration with other process equipment. In large-scale power plants or chemical facilities, where desulfurization is a critical component of emissions control, the need for high-capacity conveying systems is evident. The working scene may involve transporting sodium bicarbonate from storage silos to reactors or from reaction zones to storage areas, often over considerable distances. The system must be designed to handle varying material flow rates and maintain consistent performance under different operational conditions. Additionally, the working scene may require integration with other equipment, such as dust collectors and material feeders, to ensure a seamless flow of materials. The characteristics of the working scene also impact the choice of conveying line material and the type of air filtration required to prevent dust contamination. By analyzing these characteristics, engineers can tailor the pneumatic conveying system to meet the specific demands of the desulfurization process, ensuring reliability and efficiency.
Real-world applications of pneumatic conveying for desulfurization sodium bicarbonate illustrate its practical benefits. For instance, in a coal-fired power plant, the desulfurization system may require the continuous supply of sodium bicarbonate to the absorber. A positive pressure pneumatic conveying system can efficiently transport the material from a bulk storage tank to the absorber, even over long distances. The system's ability to handle abrasive materials without excessive wear on components is particularly valuable in such applications. Similarly, in a chemical manufacturing facility, the process of producing sodium bicarbonate may involve transporting the material from a reaction vessel to a drying and packaging unit. The use of a negative pressure system can effectively capture and convey the material, minimizing dust emissions and ensuring a clean working environment. The operational benefits of pneumatic conveying include reduced labor costs due to automated material handling, improved safety by eliminating manual handling of powders, and enhanced process control through precise flow regulation. These advantages make pneumatic conveying a preferred choice for industries seeking to optimize their desulfurization processes.
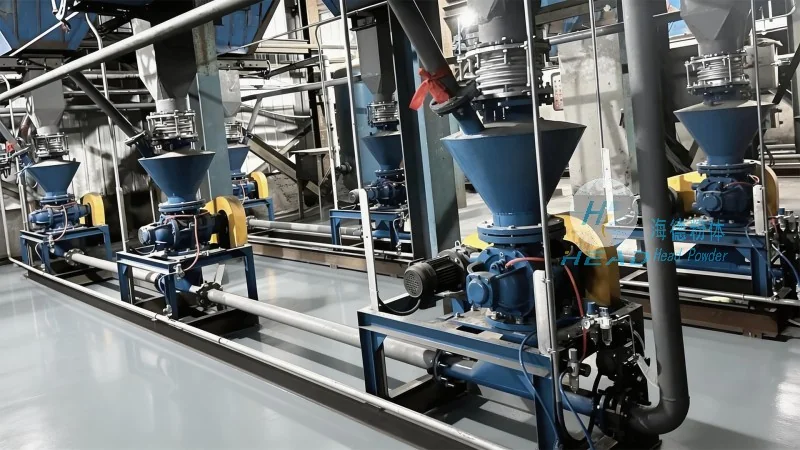
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of engineering solutions for material handling and processing. With a focus on innovative technologies, HeadPowder specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of various industries, including power generation, chemical manufacturing, and environmental protection. The company's expertise lies in understanding the unique challenges of handling materials like desulfurization sodium bicarbonate and developing customized solutions that enhance operational efficiency and safety. HeadPowder's commitment to quality and customer satisfaction has established it as a trusted partner in the industry, delivering reliable and efficient material handling systems that meet the highest standards. With a strong presence in China, HeadPowder continues to expand its services globally, providing advanced solutions for modern industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top