Pneumatic conveying technology has become an essential method for handling and transporting nickel sulfate crystalline materials in industrial applications. This process involves the use of air or other gases to move solid particles through a pipeline system. The fundamental principle of pneumatic conveying relies on the creation of a pressure differential between the conveying line and the ambient environment, which allows the material to be suspended and transported efficiently. For nickel sulfate, a critical industrial chemical used in battery production and other applications, effective material handling is crucial for maintaining production efficiency and product quality. This article explores the underlying principles of pneumatic conveying for nickel sulfate crystalline materials and highlights the key characteristics of its application scenarios.
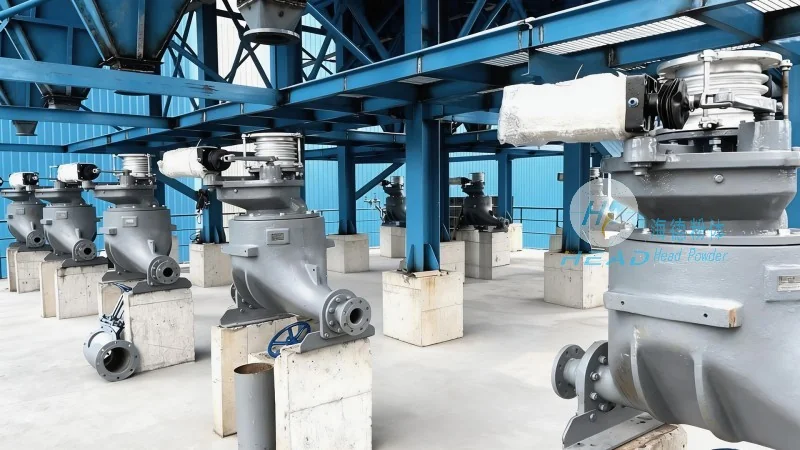
The operation of pneumatic conveying systems for nickel sulfate crystalline materials is based on several key principles. The first principle is the generation of a sufficient airflow to lift and transport the solid particles. This is typically achieved by using a blower or compressor to create a pressure difference. The second principle involves the design of the conveying line, which must be appropriately sized and configured to handle the specific properties of the material, such as its particle size, density, and moisture content. The third principle is the control of the conveying velocity and pressure, which are critical for preventing material degradation, blockages, or excessive energy consumption. In the case of nickel sulfate, the material's hygroscopic nature and potential for agglomeration require careful consideration of these parameters to ensure reliable and efficient transport.
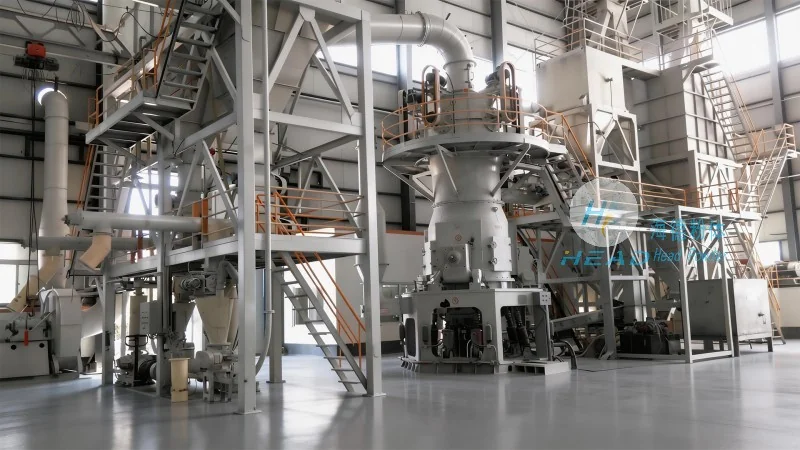
The application scenarios for pneumatic conveying of nickel sulfate crystalline materials vary based on the specific industrial processes and operational requirements. One common scenario is in the battery manufacturing industry, where nickel sulfate is used as a precursor for lithium-ion batteries. In this context, the material needs to be transported from storage silos to mixing and processing units without loss of quality or moisture. The operational characteristics in such scenarios include high-volume, continuous conveying with minimal downtime, and strict control of particle size distribution to meet downstream process specifications. Another scenario involves the material handling in chemical processing plants, where the material may be transferred between different processing stages, such as from crystallization tanks to drying equipment. Here, the conveying system must be designed to handle varying material flow rates and potential changes in particle characteristics due to processing conditions. Additionally, the work environment in these applications often demands robust and reliable equipment that can withstand the corrosive nature of the material and the operational stresses of continuous use.
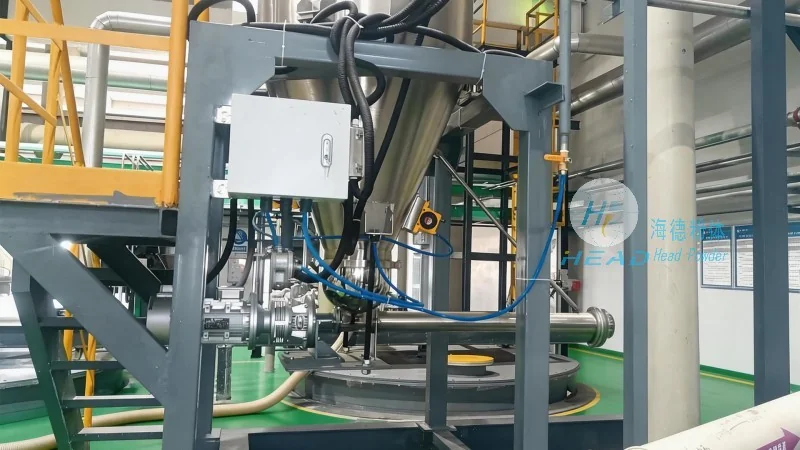
Pneumatic conveying offers several advantages for the transport of nickel sulfate crystalline materials. These include the ability to handle fine or cohesive materials that may be difficult to transport using traditional methods like belt conveyors or bucket elevators. The system also provides a closed-loop operation, which helps in maintaining material integrity and preventing contamination from external sources. Furthermore, pneumatic conveying can be integrated with other processing equipment, allowing for a more streamlined and automated material handling workflow. However, there are also considerations to keep in mind. For instance, the energy consumption of pneumatic conveying systems can be higher compared to some other transport methods, and the design must account for potential pressure losses and the need for regular maintenance to ensure optimal performance. In the case of nickel sulfate, the hygroscopic properties of the material may lead to moisture absorption during transport, which could affect the material's quality if not properly controlled. Therefore, the system design must include features such as moisture control and temperature regulation to mitigate these issues.
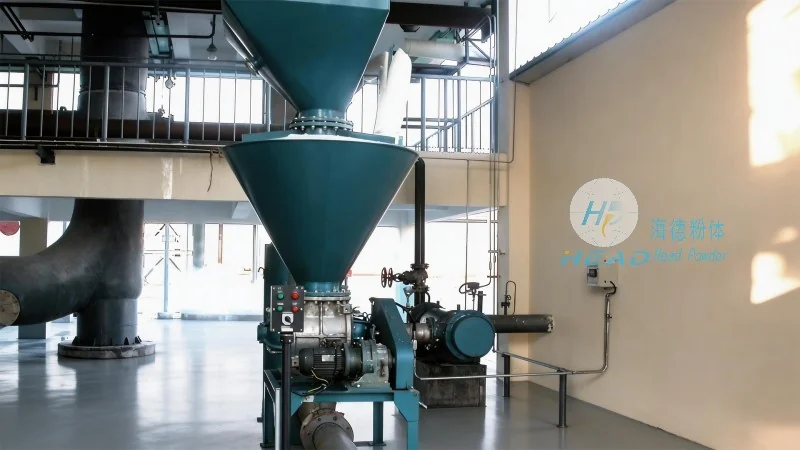
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of engineering solutions for material handling and processing in the chemical and battery industries. With a strong focus on innovation and customer satisfaction, the company specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients. Headpowder's expertise lies in understanding the unique challenges of handling materials like nickel sulfate, and developing solutions that enhance operational efficiency, reduce downtime, and ensure product quality. The company's facilities are located in Shandong, China, where it leverages advanced technology and experienced engineering teams to deliver high-quality products and services to the global market. By combining technical knowledge with practical application experience, headpowder helps industries optimize their material handling processes and achieve their production goals effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top