Quicklime powder conveying systems are critical components in industrial processes that handle calcium oxide (quicklime) powder. These systems are designed to efficiently transport quicklime from storage to processing units, ensuring consistent material flow and minimizing operational disruptions. Understanding the underlying principles and typical working scenarios of such systems is essential for optimizing industrial operations and selecting the most suitable equipment for specific applications.
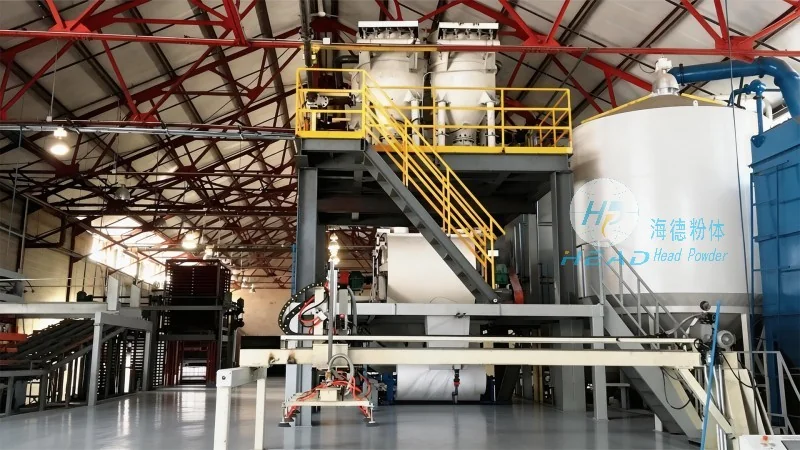
The fundamental principle of quicklime powder conveying systems revolves around the use of mechanical or pneumatic methods to move dry, fine powders like quicklime. Key components typically include hoppers, feeders, conveyors (such as screw conveyors, pneumatic ducts, or bucket elevators), and control systems. The design of these systems must address challenges like dust generation, material segregation, and the need for precise flow control. For instance, pneumatic conveying systems use compressed air to transport quicklime through pipelines, while mechanical systems rely on rotating components to move the material. The choice of method depends on factors such as the material's properties, the distance to be conveyed, and the required flow rate.
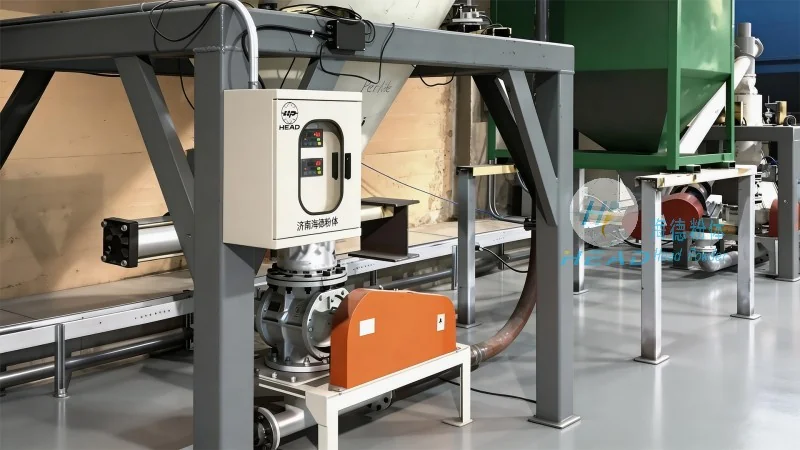
Quicklime powder conveying systems are commonly employed in various industrial settings, each with distinct characteristics that influence system design and operation. One typical working scene is in cement production facilities, where quicklime is a key raw material. In such environments, the system must handle large volumes of quicklime and integrate seamlessly with other production equipment. Another common scenario is in chemical processing plants, where quicklime is used for neutralization or as a reagent. Here, the system may need to operate under controlled conditions to prevent moisture absorption or reaction with other chemicals. Additionally, in mining and mineral processing operations, quicklime is used for ore treatment, and the conveying system must be robust enough to handle abrasive materials and varying particle sizes. Each working scene demands specific adaptations, such as different conveyor speeds, material handling capacities, or environmental controls, to ensure optimal performance and safety.
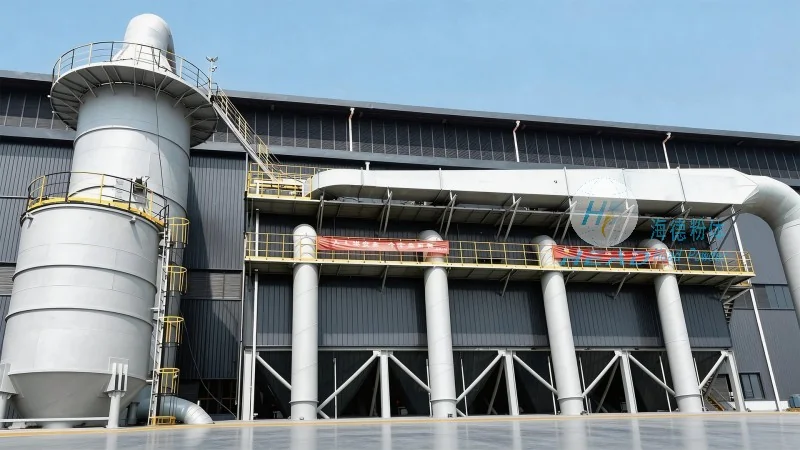
Modern quicklime powder conveying systems, such as those offered by companies like Shandong HeadPowder Engineering Co., Ltd., offer several advantages that enhance operational efficiency and safety. One significant feature is the ability to maintain a closed system, which minimizes dust emissions and protects workers from exposure to fine powders. This is achieved through sealed hoppers, ducts, and feeders, often equipped with dust collection systems. Another advantage is the precise control over material flow, which helps in maintaining consistent product quality and reducing waste. Advanced control systems, including sensors and automation, allow for real-time monitoring and adjustment of conveyor speed, pressure, and flow rate. This not only improves efficiency but also extends the lifespan of equipment by preventing overloading or excessive wear. Furthermore, the modular design of many systems enables easy integration with existing infrastructure and facilitates maintenance, reducing downtime and operational costs.
When selecting or designing a quicklime powder conveying system, several application-specific considerations must be taken into account. The first is the material's physical properties, including particle size distribution, moisture content, and bulk density. Quicklime is a fine powder with a high reactivity, which can affect the choice of conveyor type and operating parameters. For example, systems handling very fine quicklime may require additional filtration or dust suppression measures to prevent clogging. The second consideration is the conveying distance and layout of the facility. Short-distance conveying might use screw conveyors or bucket elevators, while long-distance applications often rely on pneumatic systems with multiple stages to maintain pressure and material flow. The third factor is the environmental regulations and safety standards applicable to the industry. Compliance with local regulations regarding dust control and material handling is crucial, and many modern systems are designed to meet or exceed these standards. Finally, the integration with downstream processes, such as mixing or reaction units, requires coordination of the conveying system's output with the input requirements of these units. This ensures a smooth and continuous flow of materials throughout the production line.
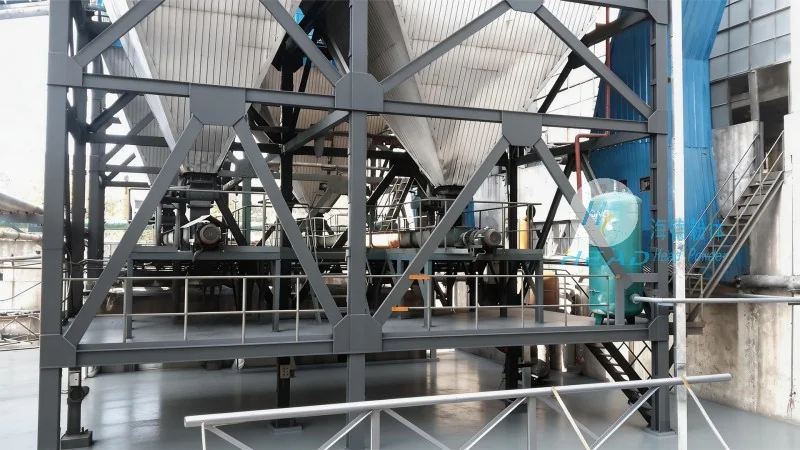
In conclusion, quicklime powder conveying systems play a vital role in industrial operations by ensuring efficient and safe transport of this essential material. The principles behind these systems, combined with their working scene characteristics, highlight the importance of tailored solutions that address specific operational needs. By leveraging advanced technology and design, modern conveying systems offer significant advantages in terms of efficiency, safety, and cost-effectiveness. For industries relying on quicklime, investing in a well-designed and properly maintained conveying system is a strategic decision that can enhance overall productivity and product quality. As the demand for quicklime continues to grow, the development of more sophisticated and reliable conveying systems will remain a key focus in industrial engineering.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top