Sulfur powder is a common material in industrial processes, and its efficient handling is crucial for maintaining production efficiency and safety. A sulfur powder pneumatic conveying system is a specialized equipment designed to transport sulfur powder through the use of air or other gas streams. This system offers a reliable and effective method for moving bulk sulfur powder from one location to another within a facility, ensuring minimal dust generation and improved operational safety.
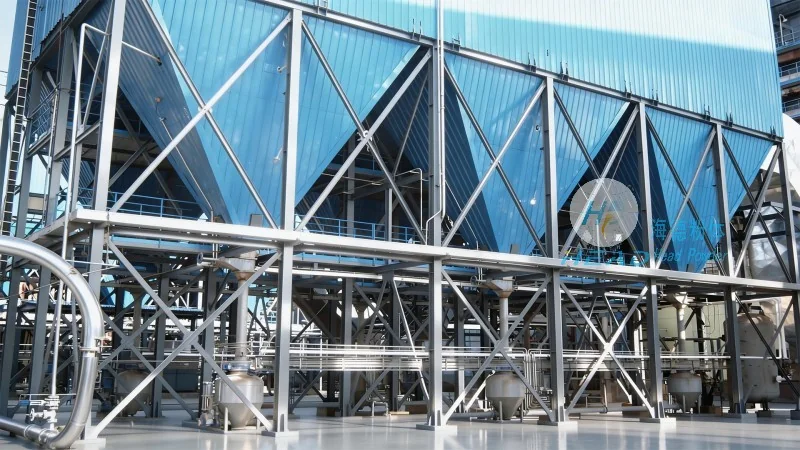
The sulfur powder pneumatic conveying system operates by creating a pressure differential or using vacuum to move the powder through a network of pipes. The system typically consists of a hopper, a conveyor line, and a receiver. The hopper holds the sulfur powder, and when the system is activated, air is introduced to create a flow that carries the powder through the pipes to the receiver. This method is particularly advantageous for sulfur powder due to its fine particle size and potential for dust explosion risks, as it minimizes direct contact with the powder and reduces the risk of ignition sources.
The design of a sulfur powder pneumatic conveying system involves several critical principles to ensure optimal performance and safety. First, the system must be designed to handle the specific properties of sulfur powder, such as its particle size distribution, density, and flow characteristics. The selection of appropriate air velocities and pressure levels is essential to prevent particle segregation and ensure consistent flow. Additionally, the system incorporates features like pulse-jet or rotary airlock valves to control the flow and prevent blockages, which are common issues in pneumatic conveying systems. The materials used in the construction of the system components, such as stainless steel or special coatings, are chosen to resist corrosion and chemical reactions with sulfur, ensuring long-term durability and reliability.
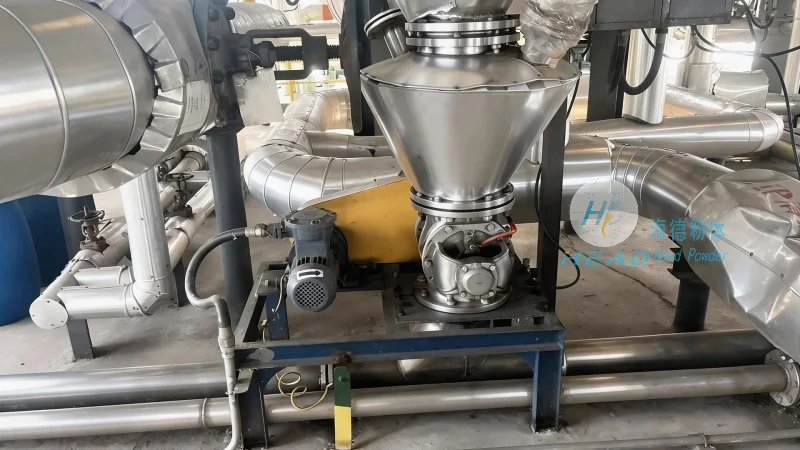
The sulfur powder pneumatic conveying system comprises several key components, each playing a vital role in the overall operation. The hopper serves as the storage and feeding unit, where the sulfur powder is loaded and prepared for transport. The conveyor line, typically made of flexible or rigid pipes, transports the powder from the hopper to the receiver. The receiver collects the conveyed sulfur powder and may include a dust collection system to capture any particles that escape during the process. The air supply unit, which can be a blower or a vacuum pump, generates the necessary airflow to move the powder. The control system manages the operation of the components, ensuring smooth and safe operation by monitoring pressure, flow rates, and other critical parameters.
Implementing a sulfur powder pneumatic conveying system offers numerous advantages over traditional methods like bucket elevators or belt conveyors. One of the primary benefits is the reduction in dust generation, which enhances workplace safety and compliance with environmental regulations. The system also minimizes the risk of material degradation or contamination, as the powder is enclosed within the pipes, preventing exposure to external elements. Furthermore, the system allows for precise control over the flow rate and direction of the powder, enabling better integration with downstream processes. The compact design of the system also saves space in industrial facilities, making it suitable for applications with limited floor area.
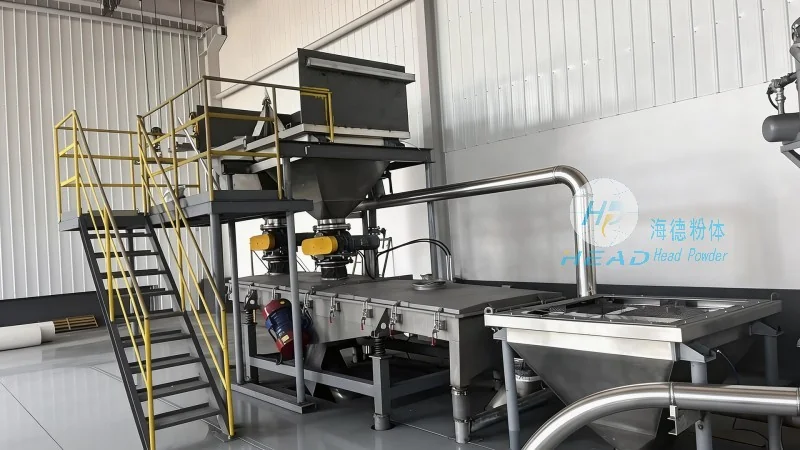
Sulfur powder pneumatic conveying systems are widely used in various industries that handle sulfur powder, including chemical manufacturing, fertilizer production, and petrochemical processing. In chemical plants, the system is used to transport sulfur powder for the production of sulfuric acid or other sulfur-based chemicals. In fertilizer facilities, it helps in the handling of sulfur-based fertilizers, ensuring efficient distribution to production lines. The petrochemical industry also utilizes these systems for transporting sulfur in the processing of crude oil and natural gas. The versatility of the system makes it suitable for a range of applications where reliable and safe sulfur powder transport is required.
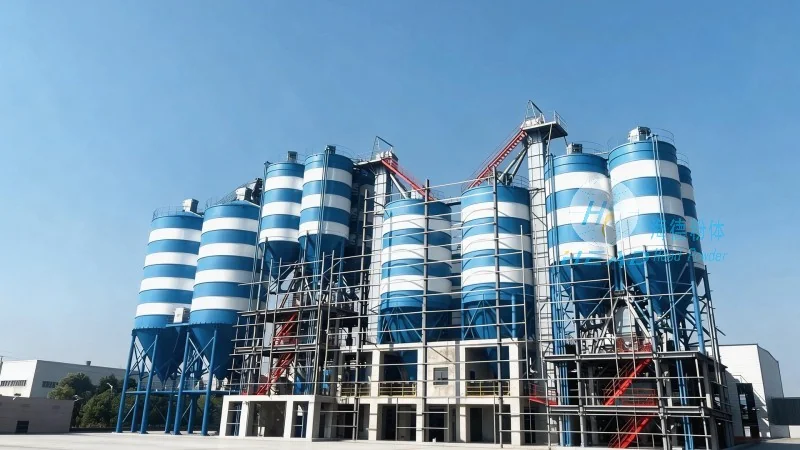
Maintaining the sulfur powder pneumatic conveying system is essential to ensure its longevity and safe operation. Regular inspections of the hopper, conveyor lines, and receiver are necessary to check for wear and tear or blockages. Cleaning the system periodically, especially after handling different materials, helps prevent the buildup of residue that could affect performance. Safety considerations are paramount due to the potential hazards associated with sulfur powder, such as dust explosions. The system should be equipped with explosion-proof components and proper ventilation systems to mitigate these risks. Additionally, training operators on the safe operation of the system and emergency procedures is crucial for preventing accidents and ensuring compliance with safety regulations.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling equipment, specializes in designing and supplying high-quality sulfur powder pneumatic conveying systems. With years of experience and a commitment to innovation, the company provides customized solutions tailored to the specific needs of its clients. HeadPowder's systems are engineered to meet the highest standards of performance, safety, and durability, ensuring reliable operation in demanding industrial environments. The company's headquarters is located in Shandong, China, where it leverages advanced technology and skilled expertise to deliver superior products and services to the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top