For industrial applications involving the handling of magnesium sulfate, an efficient and reliable material transport solution is crucial. This article explores the concept of a magnesium sulfate pneumatic conveying system, detailing its operational principles and design considerations. By understanding these aspects, industries can optimize material handling processes, enhance safety, and improve overall operational efficiency.
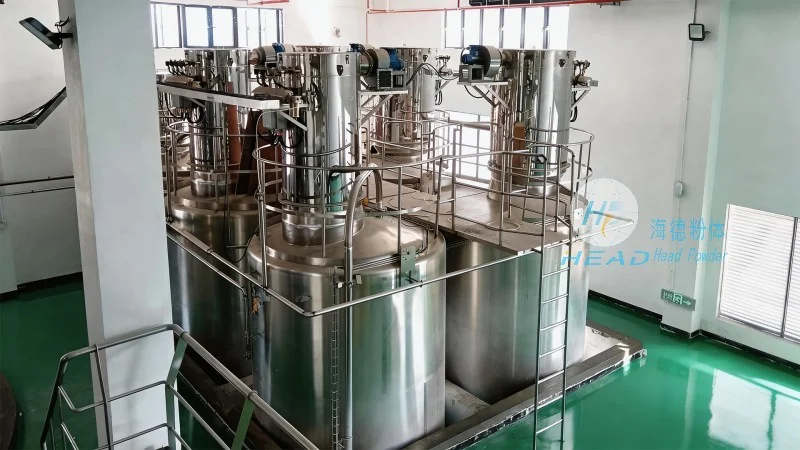
Magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industries, including pharmaceuticals, agriculture, and food processing. Handling this material requires specialized equipment to ensure safe and efficient transport from storage to processing units. A pneumatic conveying system offers a solution by utilizing air pressure to move the material through a pipeline network. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational safety.
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of advanced material handling systems, specializing in the design and implementation of pneumatic conveying solutions. With years of experience in the industry, HeadPowder has developed expertise in handling diverse materials, including magnesium sulfate. The company is located in Shandong, China, and its commitment to quality, innovation, and customer satisfaction has made it a trusted name in the field. HeadPowder’s systems are engineered to meet the specific needs of clients, ensuring optimal performance and reliability.
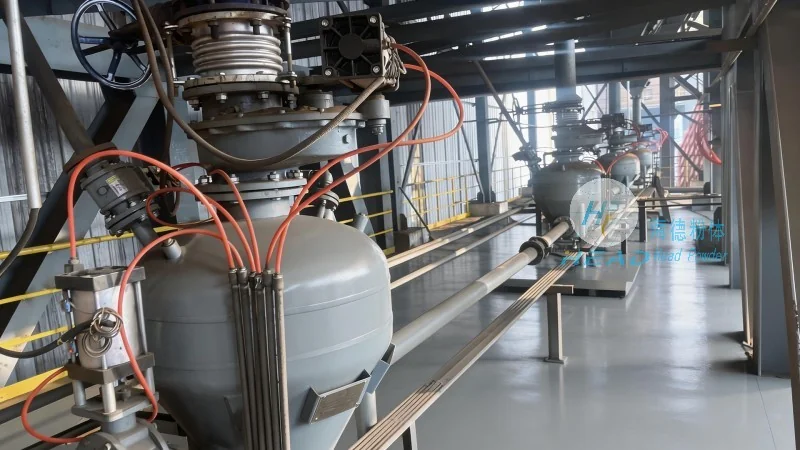
The design of a magnesium sulfate pneumatic conveying system involves several key principles to ensure effective material transport. The system typically consists of a blower or compressor that generates the necessary air pressure to move the material. The material is then introduced into the system, often through a hopper or feeder, and mixed with the air stream. The air-material mixture travels through the pipeline to the destination point, where it is separated from the air and collected. The design must consider factors such as material properties, flow rates, pipeline length, and pressure requirements to achieve efficient and consistent transport.
Several components are integral to the operation of a magnesium sulfate pneumatic conveying system. The blower or compressor is responsible for generating the air pressure needed to move the material. The hopper or feeder ensures a consistent supply of magnesium sulfate into the system, preventing blockages and maintaining a steady flow. The pipeline network connects the source and destination points, with appropriate sizing to handle the material-air mixture without excessive pressure loss. The separator, typically a cyclone or bag filter, separates the material from the air at the end of the pipeline, allowing the air to be recirculated or vented safely. The control system monitors and regulates the operation of the blower, feeder, and other components to maintain optimal performance.
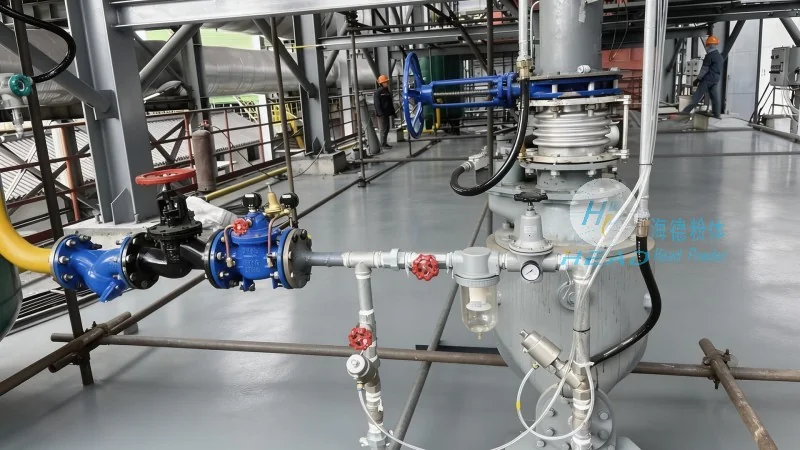
Implementing a pneumatic conveying system for magnesium sulfate offers numerous advantages over traditional mechanical methods. One of the primary benefits is the elimination of direct human contact with the material, enhancing workplace safety. The system also reduces the risk of material contamination, as it operates in a closed environment. Additionally, pneumatic conveying systems are more flexible, allowing for changes in material flow rates and destinations without major modifications. The lack of moving parts reduces maintenance requirements and downtime, leading to lower operational costs. Furthermore, the system can handle a wide range of material sizes and moisture content, making it suitable for various industrial applications.
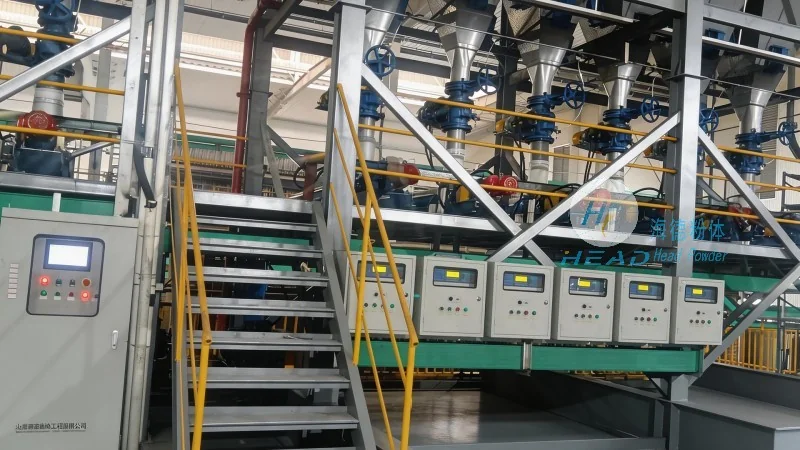
Magnesium sulfate pneumatic conveying systems are widely used in industries where the material needs to be transported over long distances or through complex layouts. For example, in pharmaceutical manufacturing, the system ensures that raw materials are delivered to processing units without contamination, maintaining product quality. In agricultural applications, the system facilitates the transport of magnesium sulfate for fertilizer production, improving efficiency in the supply chain. The reliability and efficiency of these systems contribute to increased productivity and reduced operational costs for businesses. By optimizing material handling, industries can focus on core processes and enhance their overall competitiveness.
In conclusion, a magnesium sulfate pneumatic conveying system is a sophisticated and efficient solution for handling this chemical compound. The design principles and components work together to ensure safe, reliable, and cost-effective material transport. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can implement these systems to improve their operational performance. As technology advances, future developments may include more energy-efficient blowers, advanced control systems, and materials that enhance the durability of the pipeline network. These innovations will further optimize the use of pneumatic conveying systems in the handling of magnesium sulfate and other materials, driving industrial efficiency and sustainability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top