Ammonium fertilizer, a critical component in modern agricultural practices, requires efficient and reliable transport systems to ensure optimal distribution and application. Pneumatic conveying systems have emerged as a preferred method for handling these materials due to their ability to transport powders over long distances with minimal loss and contamination. This article explores the fundamental aspects of an ammonium fertilizer pneumatic conveying system, focusing on its design principles and the technical considerations that enable effective operation.
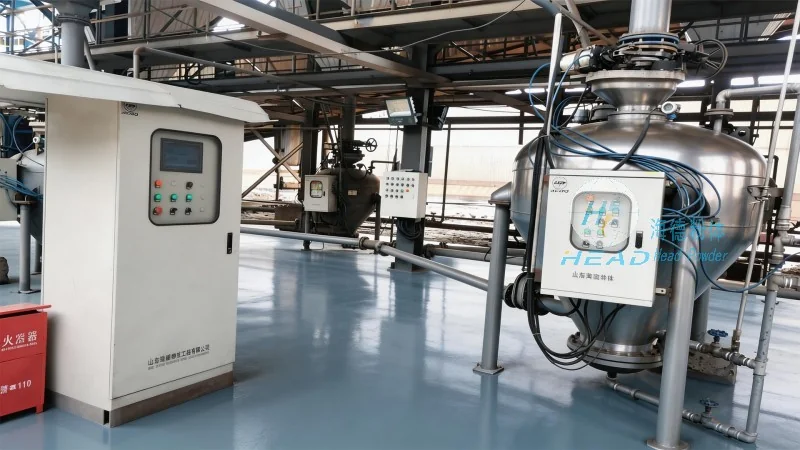
An ammonium fertilizer pneumatic conveying system is a mechanical process that uses air or other gases to transport dry, granular materials like ammonium-based fertilizers from one location to another. Unlike traditional methods such as belt conveyors or bucket elevators, pneumatic systems offer advantages in terms of flexibility, scalability, and the ability to handle materials that are prone to dust or clumping. The system typically consists of a series of components including a material hopper, a conveying line, a dust collection system, and a discharge outlet. These components work in tandem to create a pressure differential that propels the fertilizer through the system, ensuring a continuous and controlled flow.
The primary function of a pneumatic conveying system for ammonium fertilizer is to move the material from a storage or production area to a processing or application site. This process involves several key steps: first, the fertilizer is fed into the system from a hopper; second, a fan or blower generates the necessary airflow to create a pressure difference; third, the material is entrained by the air and transported through the pipeline; and fourth, the material is discharged at the destination. The efficiency of this process depends on the system's ability to maintain consistent airflow and pressure, which directly impacts the conveying rate and the overall system performance.
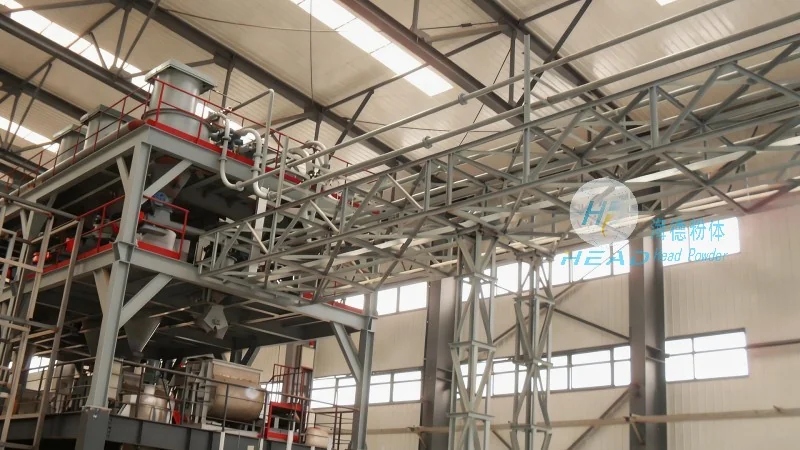
Designing an effective pneumatic conveying system for ammonium fertilizer involves several critical principles that ensure safety, efficiency, and durability. First, the system must be designed to handle the specific properties of ammonium-based fertilizers, such as their particle size, moisture content, and potential for dust generation. This includes selecting appropriate materials for the conveying line, such as stainless steel or corrosion-resistant alloys, to prevent material degradation and equipment wear. Second, the system must be engineered to maintain a consistent pressure and airflow, which is crucial for preventing blockages and ensuring a smooth flow. This often involves using variable frequency drives (VFDs) to control the fan speed and adjust airflow based on the material load. Third, the system must incorporate effective dust collection and filtration systems to comply with environmental regulations and protect personnel from exposure to fine particles. Finally, the design must consider the system's scalability, allowing for future expansion or integration with other processing equipment.
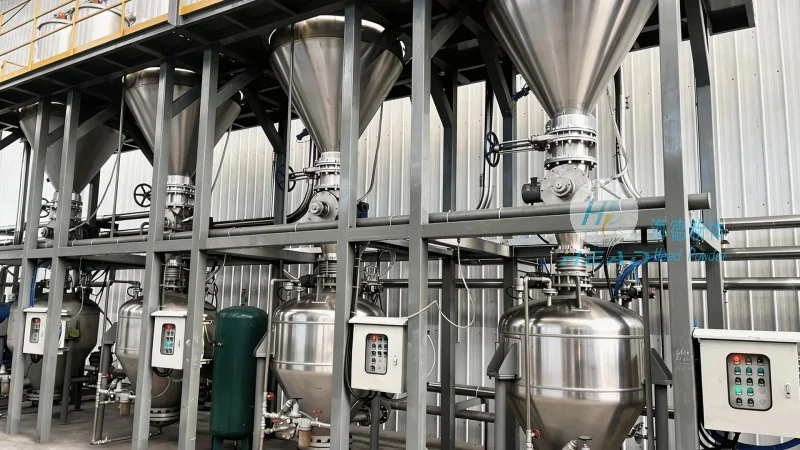
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pneumatic conveying systems tailored for the fertilizer industry. With a focus on innovation and customer-centric solutions, HeadPowder has developed advanced systems that address the unique challenges of handling ammonium fertilizers. The company's expertise lies in designing customized solutions that meet the specific requirements of each client, whether it's for small-scale agricultural operations or large industrial facilities. HeadPowder's systems are built with high-quality components, including durable fans, efficient filtration systems, and robust conveying lines, ensuring long-term reliability and minimal maintenance. The company also provides comprehensive technical support and after-sales services, helping clients optimize their operations and maximize the efficiency of their fertilizer handling processes.
Operational considerations for ammonium fertilizer pneumatic conveying systems include monitoring system performance, maintaining proper airflow, and ensuring the system is regularly cleaned and maintained. Regular maintenance is essential to prevent clogging and ensure the system operates at peak efficiency. This includes checking fan performance, cleaning filters, and inspecting the conveying line for any signs of wear or damage. Additionally, system operators must be trained to handle potential issues such as pressure fluctuations or material blockages, which can impact the overall efficiency of the process. By adhering to best practices in maintenance and operation, users can extend the lifespan of their equipment and minimize downtime, ultimately improving the cost-effectiveness of their fertilizer handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top