Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional engineering company based in Shandong, China. The company specializes in the design, manufacturing, and installation of pneumatic conveying systems, with a particular focus on solutions for sintered ash transportation. Headpowder leverages advanced engineering principles and years of industry experience to deliver efficient and reliable systems tailored to diverse industrial needs.
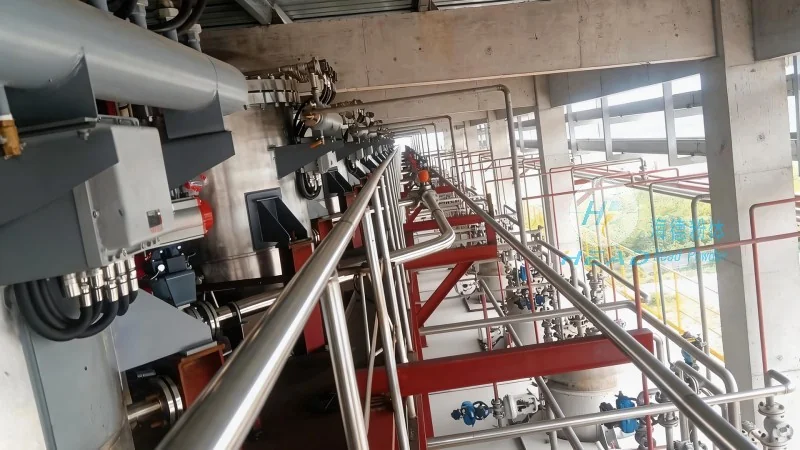
The sintered ash pneumatic conveying system operates on the fundamental principle of air-based transportation, where solid materials are transported through a pipeline using compressed air. In this system, sintered ash, a byproduct of the sintering process in metallurgical industries, is introduced into a hopper or feeder. The material is then fed into the pipeline under the pressure of compressed air, which propels the ash particles forward. The system typically includes components such as a feeding device, a conveying pipeline, a separation unit, and a dust collection system. The compressed air acts as the driving force, ensuring the efficient movement of sintered ash from the source to the destination. The design of the system is optimized to handle the specific characteristics of sintered ash, including its particle size, moisture content, and flowability, to minimize blockages and ensure consistent performance.
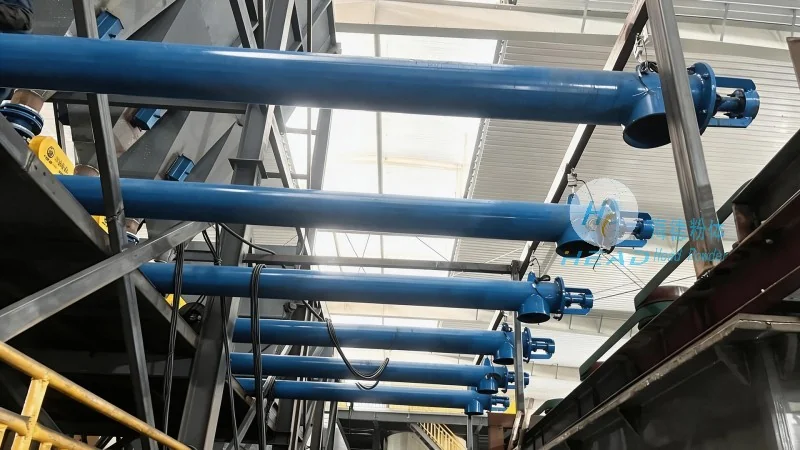
The sintered ash pneumatic conveying system is designed to operate in various industrial environments, particularly in the metallurgical and mining sectors. The system is well-suited for applications where sintered ash needs to be transported over long distances or between different processing units within a plant. Key characteristics of the working scene include the need for high efficiency and reliability, as sintered ash is often a critical material in the production process. The system is also adapted to handle varying material loads and flow rates, ensuring smooth operation even under fluctuating conditions. Additionally, the system is built to meet safety and environmental standards, with features like dust suppression and air filtration to minimize the impact on the surrounding environment. The working scene may involve integration with other industrial equipment, such as sintering furnaces, storage silos, and processing machinery, requiring seamless coordination to maintain operational efficiency.
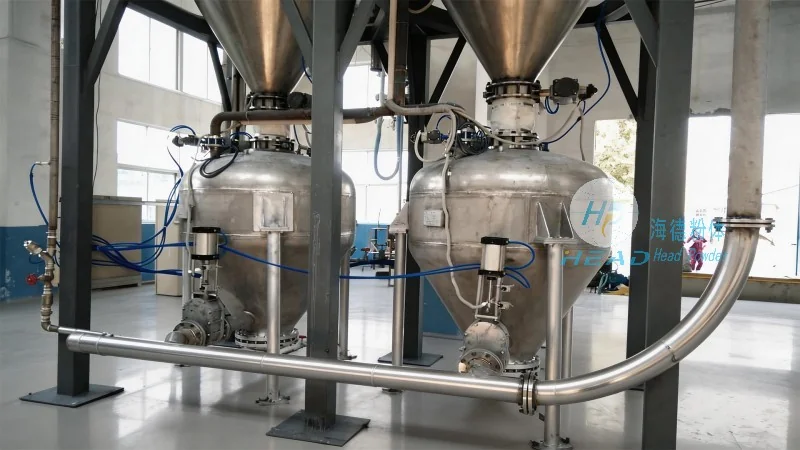
The sintered ash pneumatic conveying system offers several advantages that make it a preferred choice for industrial applications. One of the primary benefits is its ability to transport sintered ash without the need for mechanical components like conveyor belts or buckets, reducing maintenance costs and operational downtime. The system is also highly flexible, allowing for changes in the conveying route or capacity without major modifications. Another advantage is its energy efficiency, as the compressed air system can be optimized to use minimal energy while maintaining high transport efficiency. The system is particularly suitable for applications where the material is sensitive to mechanical handling, as the air-based transport minimizes wear and tear on the ash particles. In terms of applicable scenarios, the system is commonly used in sintering plants, where sintered ash is transported from the sintering machine to storage facilities or for further processing. It can also be applied in mining operations, where sintered ash is transported from processing units to disposal or recycling facilities. The system's adaptability makes it suitable for both new installations and retrofitting existing plants to improve material handling efficiency.
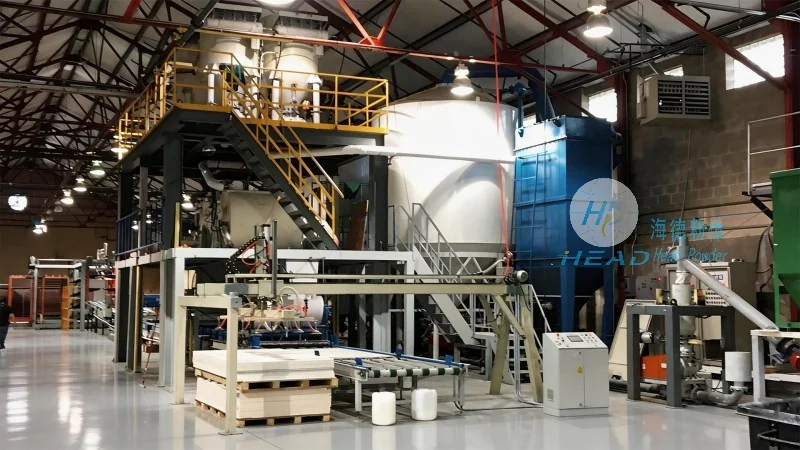
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for sintered ash pneumatic conveying systems, combining advanced engineering with practical application experience. The system's design ensures efficient, reliable, and environmentally friendly transportation of sintered ash, meeting the diverse needs of industrial clients. By leveraging the company's expertise and innovative technology, businesses can enhance their material handling processes, reduce operational costs, and improve overall productivity. The sintered ash pneumatic conveying system is a testament to headpowder's commitment to delivering high-quality engineering solutions that address the specific challenges of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top