For industries dealing with bulk materials, efficient and reliable material handling systems are crucial for maintaining operational efficiency and ensuring product quality. The tonne bag packaging material conveying system, offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to streamline the process of transporting and packaging bulk materials. This article explores the working principle and key features of this system, providing insights into how it enhances productivity and operational performance.
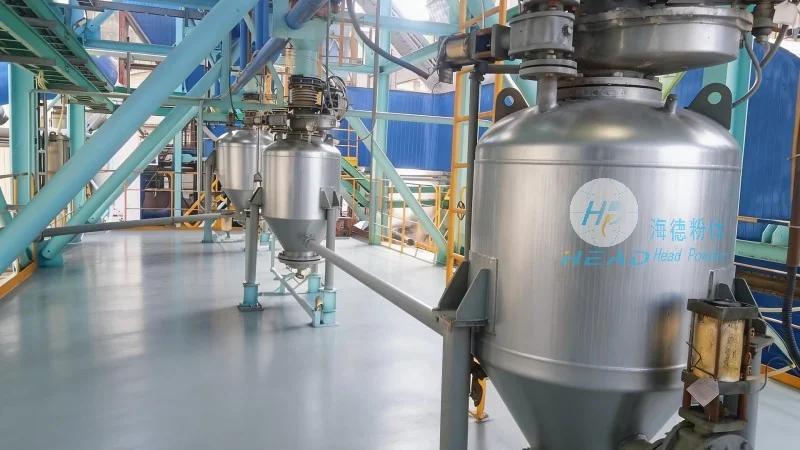
Tonne bags, also known as super sacks or big bags, are widely used in various industries for the storage and transportation of bulk materials such as grains, chemicals, and minerals. The tonne bag packaging material conveying system is a specialized equipment setup that integrates conveying mechanisms with packaging processes to facilitate the seamless movement of materials from storage to packaging units. This system is particularly beneficial for businesses that require large-scale material handling with minimal manual intervention.
The tonne bag packaging material conveying system operates on a systematic approach that combines several key components to achieve efficient material transport. The process typically begins with the loading of bulk materials into a hopper or storage silo. From there, the materials are fed into a conveyor system, which may include belt conveyors, screw conveyors, or pneumatic conveyors, depending on the material characteristics and application requirements. The conveyor system transports the materials to the packaging area where they are filled into tonne bags. The system may also incorporate mechanisms for bag sealing, labeling, and stacking, ensuring that the packaged bags are ready for transport or storage.
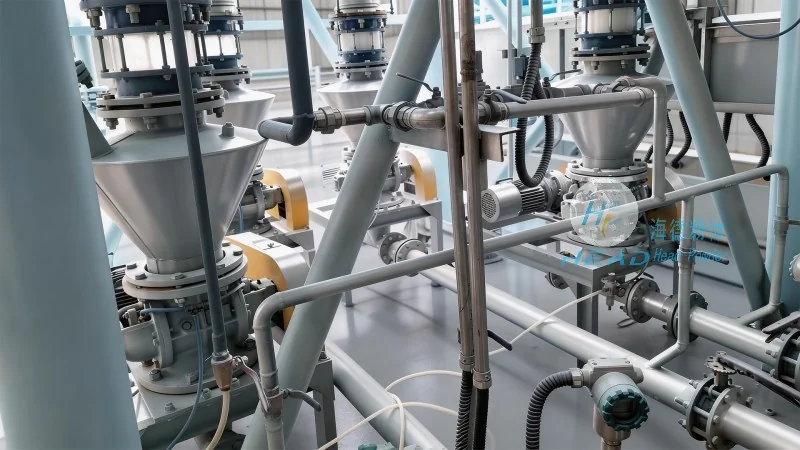
Key components of the system include the material feed hopper, which regulates the flow of bulk materials into the conveyor. The conveyor itself, which can be customized based on the material's density, flowability, and size, ensures smooth and continuous movement. The filling mechanism, often equipped with sensors and control systems, precisely measures the material volume to meet packaging specifications. Additionally, the system may feature automated bag handling equipment, such as bag openers and sealers, to streamline the packaging process and reduce human error. The entire operation is typically controlled by a centralized system that monitors and adjusts the flow of materials, ensuring optimal performance and consistency.
The tonne bag packaging material conveying system from Shandong HeadPowder Engineering Co., Ltd. is designed with several advanced features that enhance its functionality and user experience. One of the primary features is its high capacity and efficiency, capable of handling large volumes of materials with minimal downtime. The system is built with durable materials and components, ensuring long-term reliability and reduced maintenance costs. It also incorporates advanced control systems that allow for real-time monitoring and adjustment of the conveying process, improving operational flexibility and adaptability to varying production demands.
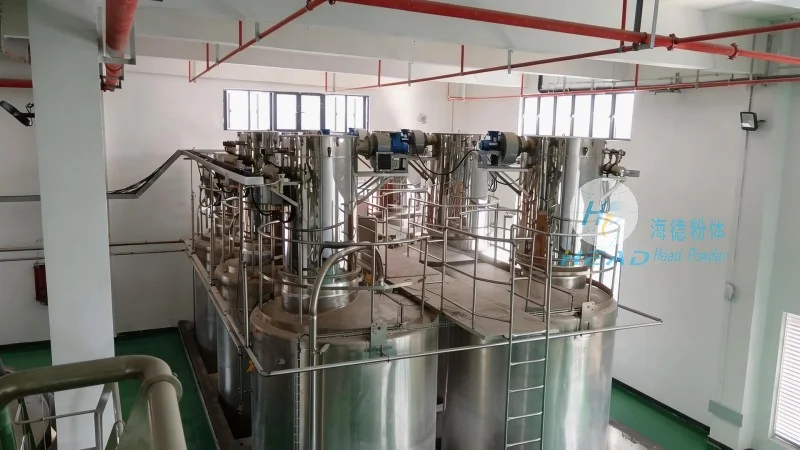
Another notable feature is the system's adaptability to different material types. Whether dealing with granular, powdery, or even wet materials, the system can be configured to handle a wide range of bulk materials, making it versatile for various industrial applications. The integration of automated bag handling equipment, such as bag openers and sealers, further enhances the system's efficiency by reducing the need for manual labor and minimizing packaging errors. Additionally, the system is designed for easy maintenance and cleaning, with components that can be easily accessed and serviced, ensuring consistent performance over time.
Adopting a tonne bag packaging material conveying system offers numerous benefits for businesses in the bulk material handling sector. The primary advantage is the significant improvement in operational efficiency, as the system automates the material transport and packaging process, reducing the time and labor required for these tasks. This leads to increased productivity and lower operational costs. The system also enhances product quality by ensuring consistent filling levels and proper packaging, minimizing material loss and contamination.
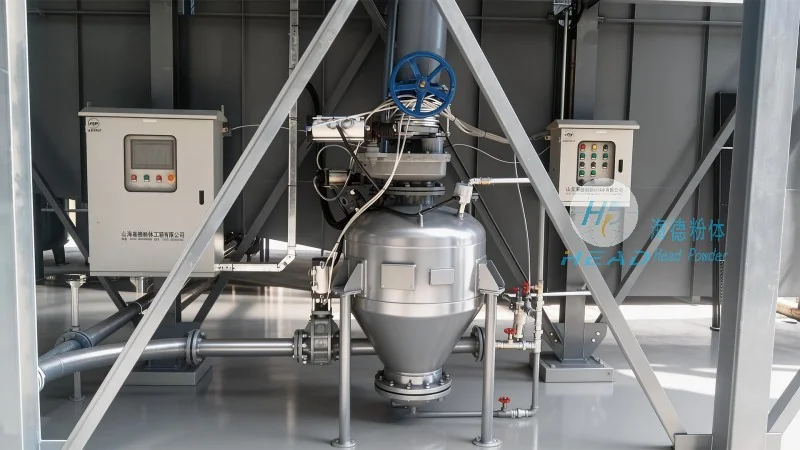
Furthermore, the system contributes to better safety in the workplace by reducing manual handling of heavy materials, thereby minimizing the risk of injuries. The automated nature of the system also reduces the likelihood of human error, ensuring that each tonne bag is filled accurately and consistently. From a logistical perspective, the system facilitates the efficient storage and transport of packaged materials, as tonne bags are designed for easy handling and transportation. This makes it easier to manage inventory and meet customer delivery requirements.
The tonne bag packaging material conveying system is a vital piece of equipment for businesses seeking to optimize their bulk material handling processes. By understanding its working principle and key features, organizations can make informed decisions about implementing such systems to enhance their operational efficiency and productivity. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, offers high-quality systems tailored to meet the specific needs of various industries. With a focus on durability, efficiency, and adaptability, their tonne bag packaging material conveying systems provide reliable solutions for businesses looking to streamline their material handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top