Silica fume, also known as microsilica, is a byproduct of silicon metal production or ferrosilicon production. It is a fine powder with a high surface area and unique chemical properties, making it a valuable additive in concrete, refractory materials, and other industrial applications. Efficient material handling of silica fume is crucial for maintaining product quality, ensuring safety, and optimizing production processes. This article explores the key aspects of silica fume material handling systems and the underlying design principles that guide their development.
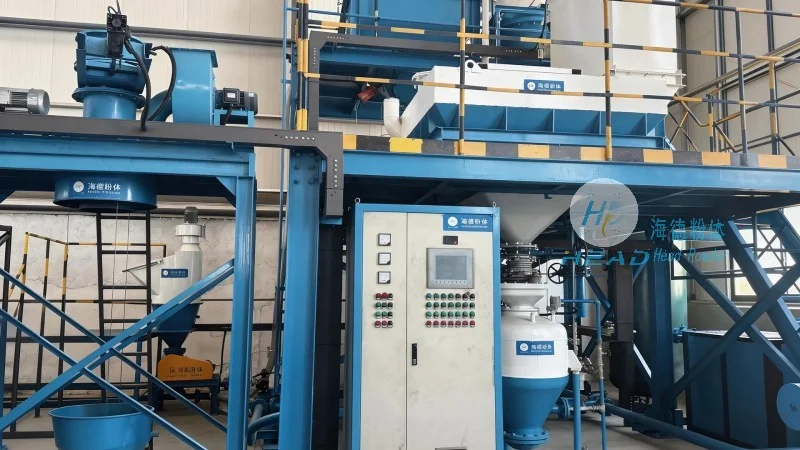
Proper handling of silica fume is essential to prevent dust generation, which can pose health risks to workers and affect the quality of the final product. Silica fume particles are extremely fine, often with a particle size distribution that includes a significant proportion of sub-micron particles. This fineness makes it challenging to handle without specialized equipment. Effective material handling systems must address issues such as dust control, material flow, and equipment durability. At Shandong HeadPowder Engineering Co., Ltd., we specialize in designing and implementing solutions that meet these challenges, ensuring that silica fume is transported safely and efficiently from storage to processing or end-use applications.
Designing a silica fume material handling system involves considering several critical factors to ensure optimal performance. The first principle is to minimize dust generation and exposure. This is achieved through the use of enclosed systems, such as silos, hoppers, and conveyor belts with dust collection systems. The second principle is to maintain consistent material flow. Silica fume can be prone to bridging or caking in storage silos, which can disrupt the flow and lead to blockages. To address this, systems often incorporate vibration devices or air knives to break up agglomerates and ensure smooth material movement. The third principle is to protect equipment from wear and corrosion. Silica fume is abrasive and can cause significant wear on metal surfaces. Therefore, materials of construction such as stainless steel, special alloys, or wear-resistant coatings are commonly used for components like hoppers, chutes, and conveyor belts.
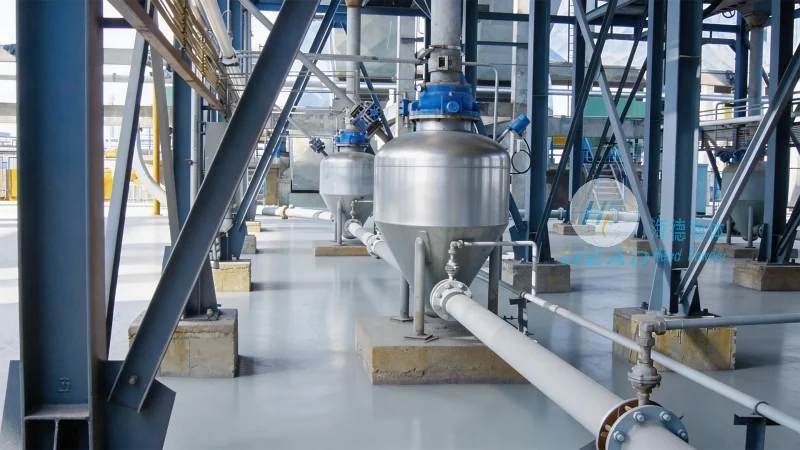
A typical silica fume material handling system consists of several key components that work together to transport the material from storage to the point of use. The primary storage unit is usually a large, airtight silo or hopper, designed to hold the bulk of the material. These storage vessels are often equipped with level sensors to monitor the material level and prevent overfilling. From the storage silo, the material is transferred to a conveyor system, which may include screw conveyors, belt conveyors, or pneumatic conveying lines. Screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle fine powders without the need for additional air. Belt conveyors are suitable for longer horizontal distances and can be integrated with dust collection systems to control airborne particles. Pneumatic conveying systems use air to transport the material, which is effective for long-distance or vertical transport but requires careful consideration of air pressure and flow rates to prevent material degradation or blockages.
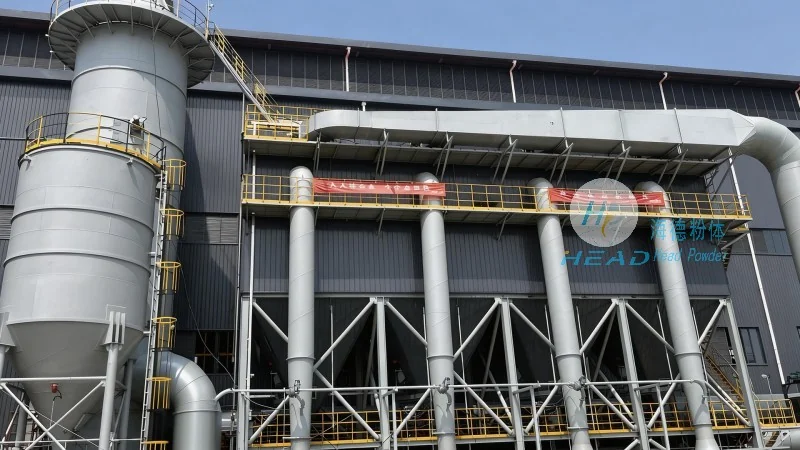
Handling silica fume requires adherence to safety standards and regulations to protect workers and the environment. The system design must include features such as explosion-proof components, especially in areas where dust accumulation is possible. Dust collection systems are critical to maintaining air quality and preventing dust explosions. These systems typically include cyclones, baghouses, or cartridge filters to capture and remove fine particles from the air stream. Additionally, the system should be equipped with safety interlocks and emergency shutdown mechanisms to prevent accidents in case of equipment failure or overpressure. At HeadPowder, we prioritize safety in all our designs, ensuring that our clients' silica fume handling systems meet or exceed industry standards and regulatory requirements.
The design of a silica fume material handling system must also consider the specific application of the material. For example, in concrete production, the system may need to integrate with batching plants and mixers, requiring precise control over the flow rate and dosage of silica fume. In refractory applications, the system may need to handle higher temperatures or more abrasive conditions, necessitating specialized equipment such as high-temperature conveyors or heat-resistant hoppers. The flexibility of the system is also important, as silica fume demand can vary based on production schedules or market conditions. A well-designed system should allow for easy adjustments to flow rates, storage capacity, or integration with other processing equipment to accommodate these changes without significant downtime or modification.
Efficient and safe material handling of silica fume is a complex task that requires careful consideration of material properties, equipment design, and operational requirements. The design principles outlined above, combined with the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., ensure that silica fume is handled in a way that maximizes product quality, minimizes environmental impact, and ensures worker safety. By investing in properly designed material handling systems, industries can improve their overall efficiency, reduce costs, and meet the growing demand for high-quality silica fume products. The key to successful silica fume material handling lies in understanding the unique challenges of the material and applying innovative engineering solutions to address them effectively.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top