Understanding the mechanisms and design principles behind sodium phosphate material handling is crucial for industries that rely on efficient and safe transport of this chemical compound. This article delves into the core concepts, technical considerations, and practical applications of sodium phosphate material handling systems, providing a comprehensive overview for professionals in the field.
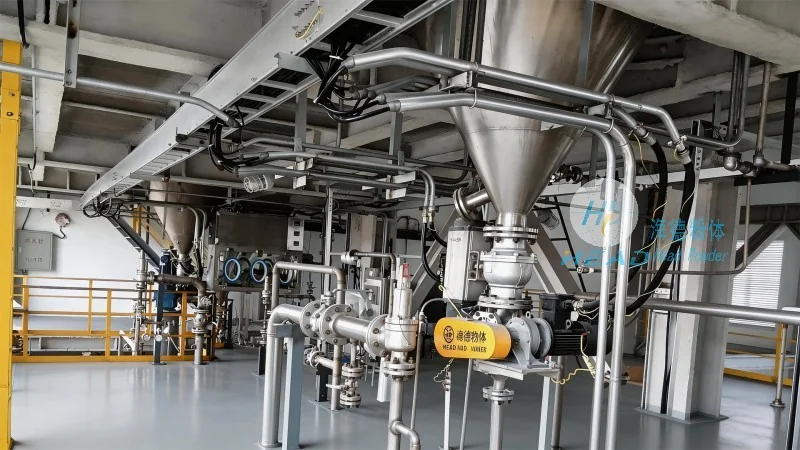
Sodium phosphate material handling refers to the processes and systems used to transport, store, and manage sodium phosphate, a widely used chemical compound in various industrial applications. This compound, often in the form of powders or granules, requires specialized handling equipment to ensure safety, efficiency, and compliance with industry standards. The design of these systems is tailored to the physical and chemical properties of sodium phosphate, such as its reactivity, dust generation, and flow characteristics.
The design of sodium phosphate material handling systems is guided by several critical principles to ensure optimal performance and safety. First, the system must address the dust control and explosion prevention measures, as sodium phosphate can be a dust explosion hazard under certain conditions. This involves implementing proper ventilation, dust collection systems, and explosion-proof equipment. Second, the design focuses on minimizing material degradation and maintaining product quality. This includes using appropriate materials for hoppers, conveyors, and storage vessels to prevent contamination or chemical reactions. Third, the system is designed for efficient flow and minimal downtime, ensuring that the material is moved from storage to processing areas with minimal friction and blockages. Additionally, the design considers the ergonomic and operational aspects, ensuring that the system is easy to maintain and operate, reducing the risk of human error.
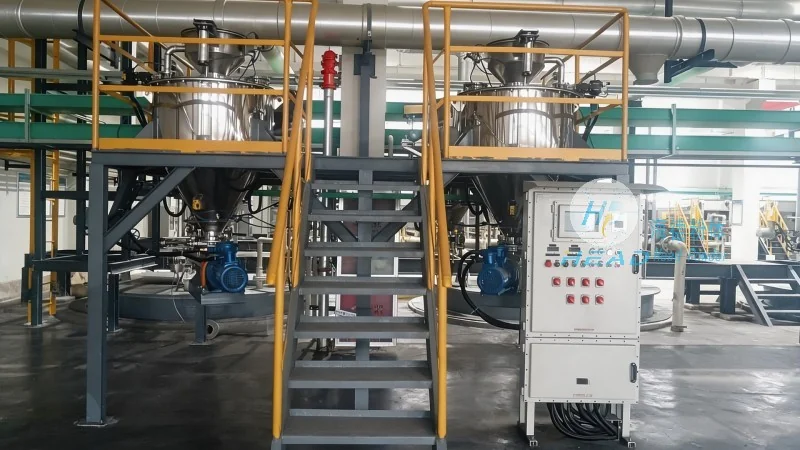
A typical sodium phosphate material handling system comprises several key components that work in tandem to achieve efficient transport. The primary components include storage silos or hoppers, which are designed to hold the bulk material. These containers are often equipped with agitators or vibrators to prevent material bridging and ensure consistent flow. Conveying systems, such as screw conveyors or pneumatic transport lines, are used to move the material from the storage area to processing equipment. These conveyors are designed with smooth surfaces and appropriate angles to minimize friction and prevent material buildup. Additionally, the system includes feeding devices, such as rotary valves or star feeders, which control the flow rate of the material into downstream processes. Finally, the system may include dust collection and filtration systems to capture any airborne particles and ensure a safe working environment.
Sodium phosphate material handling systems are utilized across a wide range of industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, sodium phosphate is used as a food additive and requires strict handling to maintain food safety standards. The systems in this sector are designed to be hygienic and easy to clean, with stainless steel components and sealed systems to prevent contamination. In pharmaceutical applications, the material handling systems must meet stringent regulatory requirements, ensuring that the material is handled in a clean and controlled environment. Chemical manufacturing industries use sodium phosphate in various processes, and the material handling systems are designed to handle the compound's reactivity and flow characteristics. Each industry has specific requirements for the system, but all share the common goal of ensuring safe and efficient transport of the material.
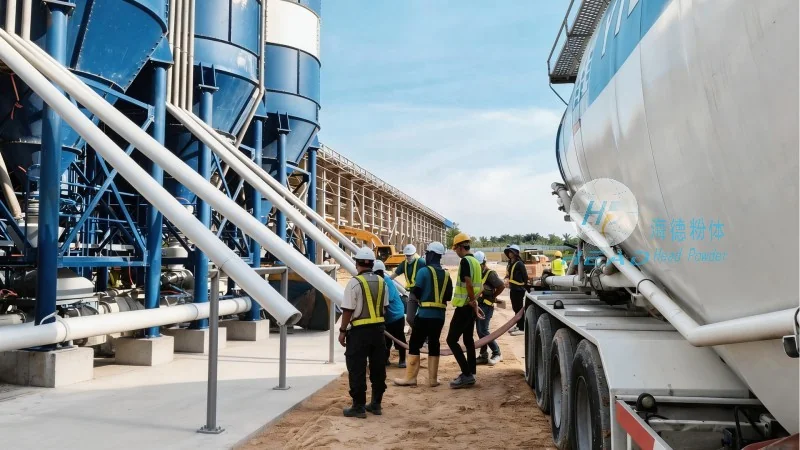
Handling sodium phosphate presents several challenges that must be addressed through careful system design. One of the primary challenges is dust explosion prevention. To mitigate this risk, systems incorporate explosion-proof equipment, proper ventilation, and dust collection systems. Another challenge is material bridging and flow issues, which can lead to blockages and downtime. This is addressed by using agitators, vibrators, and appropriate hopper designs to ensure consistent flow. Additionally, the system must be designed to handle the material's reactivity, ensuring that it does not come into contact with incompatible substances that could cause chemical reactions. The solutions to these challenges involve a combination of engineering principles, material selection, and operational practices, all aimed at ensuring the safety and efficiency of the material handling process.
In conclusion, the design of sodium phosphate material handling systems is a critical aspect of industrial operations, ensuring the safe and efficient transport of this essential chemical compound. By adhering to key design principles, such as dust control, material quality maintenance, and efficient flow, industries can minimize risks and maximize productivity. The components of these systems, including storage, conveying, and feeding equipment, are carefully selected and integrated to meet the specific needs of the application. As industries continue to rely on sodium phosphate in their processes, the importance of well-designed material handling systems will only grow, ensuring that the compound is handled safely and effectively. For companies like Shandong HeadPowder Engineering Co., Ltd., based in China, the expertise in designing and manufacturing these systems is vital to meeting the demands of various industries and maintaining high standards of safety and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top