Brewery waste material conveying, often referred to as brewery slurry or spent grain handling, is a critical process in the brewing industry. It involves the transportation of byproducts such as spent grain, yeast, and other solid residues from the brewing process to disposal or further processing sites. The efficiency and reliability of this conveying system directly impact operational costs, environmental compliance, and overall productivity in breweries. Understanding the design principles behind these systems is essential for optimizing performance and ensuring sustainable operations. For breweries, effective waste management is not just an environmental responsibility but also a financial one, as improper handling can lead to increased disposal fees and operational inefficiencies.
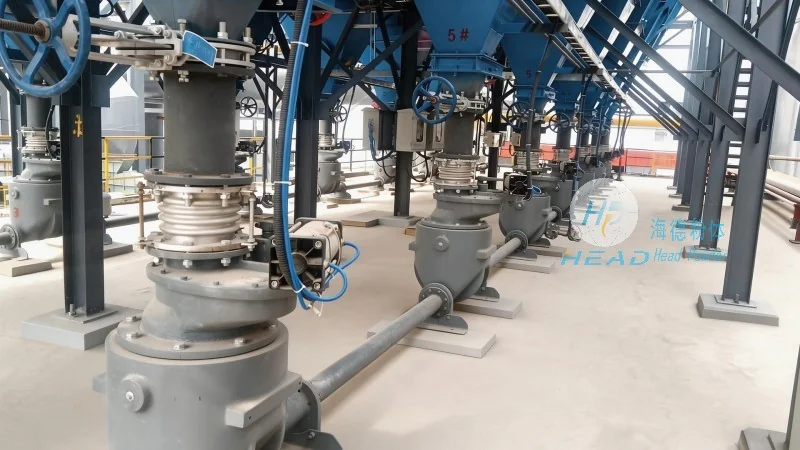
Effective brewery waste material conveying systems typically consist of several key components that work in tandem to move the material from its source to the destination. These components include feed hoppers, conveyor mechanisms (such as screw conveyors, belt conveyors, or pneumatic systems), control systems, and discharge equipment. Each component plays a vital role in ensuring the smooth and continuous movement of the material, minimizing downtime and maximizing throughput. Feed hoppers are designed to collect and store the waste material before it is fed into the conveyor, ensuring a consistent supply. Conveyor mechanisms are chosen based on the material's characteristics and the distance to be covered, with screw conveyors being ideal for handling wet or sticky materials, while belt conveyors are suitable for drier, bulkier waste. Control systems monitor and regulate the conveyor's operation, ensuring it runs at optimal speed and adjusts to changes in material flow. Discharge equipment then delivers the material to its final destination, such as a storage tank or a disposal site.
The design of a brewery waste material conveying system is guided by several fundamental principles aimed at optimizing performance, durability, and cost-effectiveness. First, the system must be capable of handling the specific characteristics of the waste material, including its moisture content, density, and particle size. This often requires specialized equipment, such as heavy-duty screw conveyors or high-capacity belt systems, to prevent clogging and ensure consistent flow. For example, if the waste is highly moist and sticky, a screw conveyor with a larger pitch or a special coating may be necessary to prevent material buildup. Second, the design must consider the overall layout of the brewery and the distance the material needs to travel, as this influences the choice of conveyor type and power requirements. Longer distances may require more powerful motors or multiple conveyor sections connected in series to maintain the material's momentum. Third, material handling efficiency is prioritized, with designs that minimize energy consumption and maintenance needs while maximizing the volume of material transported per unit of time. This involves selecting the right conveyor speed, ensuring proper alignment, and using efficient drive systems to reduce energy waste.
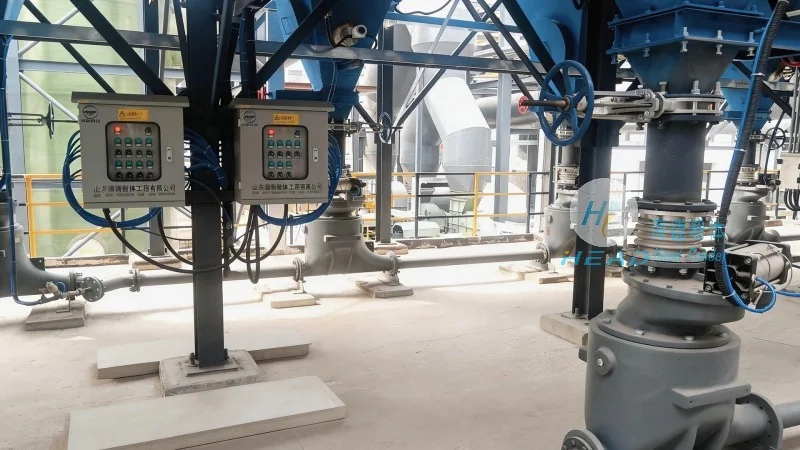
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial engineering solutions, specializes in designing and manufacturing customized brewery waste material conveying systems. With a focus on innovation and practical application, HeadPowder Engineering combines years of industry experience with advanced engineering techniques to deliver solutions tailored to the unique needs of each brewery. The company’s approach emphasizes durability, efficiency, and compliance with environmental regulations, ensuring that their systems not only meet current operational demands but also support long-term sustainability goals. HeadPowder Engineering has a proven track record of working with breweries of all sizes, from small craft breweries to large-scale commercial operations, providing systems that are both effective and cost-efficient.
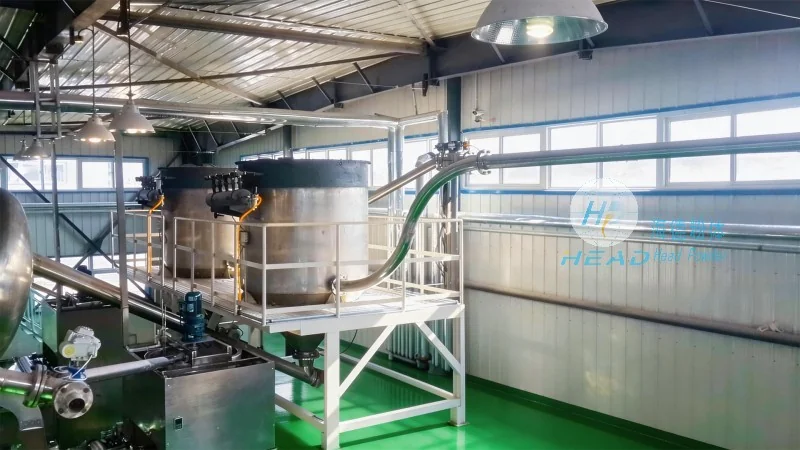
One of the key advantages of working with HeadPowder Engineering is the ability to customize conveying systems to fit specific brewery requirements. This includes adapting conveyor dimensions, speed, and control mechanisms to accommodate varying waste volumes and processing speeds. For instance, a small craft brewery may require a compact, low-power system, while a large commercial brewery may need a high-capacity system with multiple conveyor sections. Additionally, the company integrates conveying systems with other brewery equipment, such as storage tanks and processing units, to create a seamless material flow. This integration reduces bottlenecks, improves overall process efficiency, and enhances the reliability of the entire operation. By customizing the system, HeadPowder Engineering ensures that the brewery can optimize its waste handling process without compromising on performance or budget.
Reliability is a top priority in brewery waste material conveying, as downtime can lead to significant losses in production and increased disposal costs. HeadPowder Engineering designs their systems with robust construction and high-quality materials to withstand the harsh conditions of waste handling. For example, components such as conveyor screws, belts, and bearings are made from materials resistant to corrosion and wear, ensuring long service life. Regular maintenance is also a critical aspect of system performance, and the company provides comprehensive support, including maintenance plans and spare parts availability, to ensure that systems remain operational and efficient over their lifespan. This proactive approach to maintenance helps prevent unexpected breakdowns and reduces the need for costly repairs, contributing to the overall cost-effectiveness of the system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top