HeadPowder, a leading engineering company based in Shandong, China, specializes in advanced material handling solutions, particularly in the realm of sodium bicarbonate pneumatic conveying. This article provides a comprehensive exploration of the two primary pneumatic conveying methods—negative pressure and positive pressure systems—highlighting their technical nuances, operational principles, and practical applications in industrial settings.
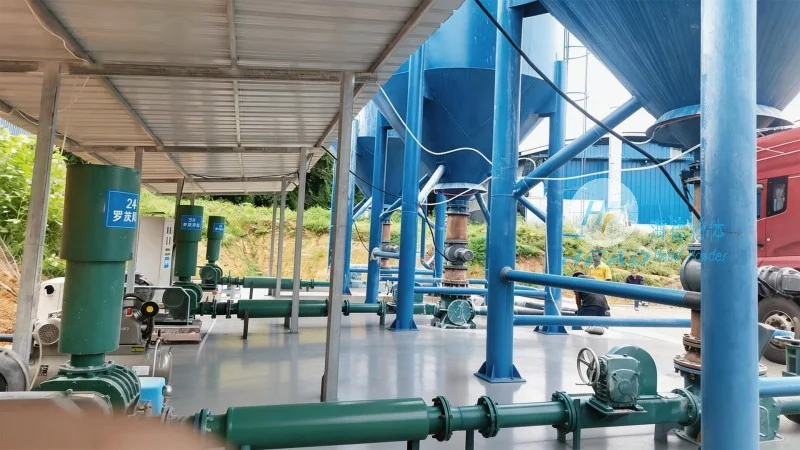
Negative pressure, or suction, pneumatic conveying systems operate by creating a vacuum at the material inlet to draw particles into the conveying line. This method is particularly effective for transporting materials from multiple source points to a single destination, such as in bulk material handling for sodium bicarbonate. The system typically includes a vacuum pump, a hopper with a rotary valve, and a pipeline network. The key advantage of negative pressure systems is their ability to handle fine powders and prevent product contamination, as the material is drawn rather than forced through the system. However, they have limitations in terms of distance and material density, as the vacuum pressure may not be sufficient for long-distance or high-density material transport.
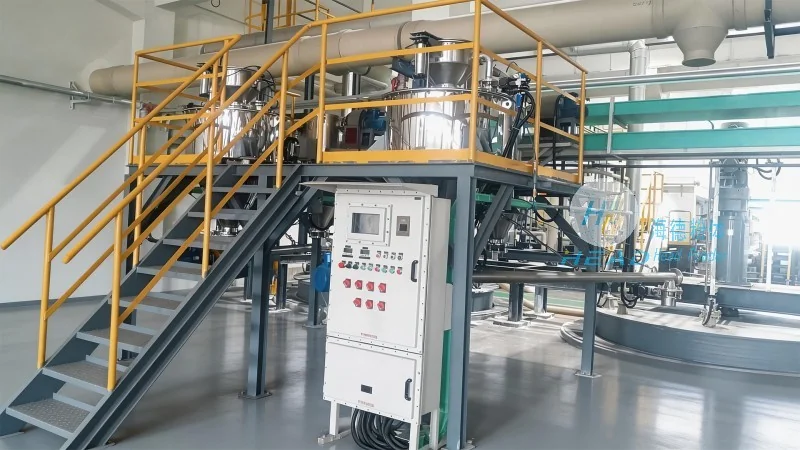
Positive pressure, or pressure, pneumatic conveying systems generate compressed air to push material through the conveying line. Unlike negative pressure systems, these systems are ideal for long-distance transport and handling of larger particles or bulk materials. The setup includes a blower, a material hopper with a discharge valve, and a pipeline with appropriate pressure ratings. Positive pressure systems offer higher conveying capacity and can handle more challenging materials, including those with higher moisture content or abrasive properties. However, they require more robust equipment and may pose higher operational costs due to the need for compressed air generation and system maintenance.
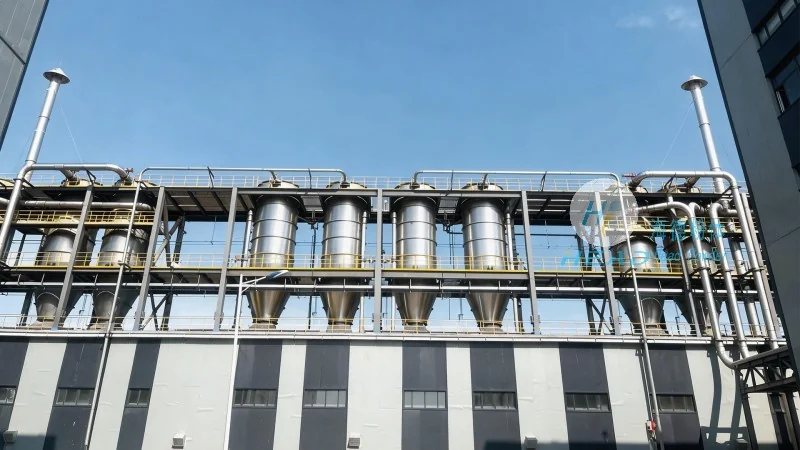
When selecting between negative and positive pressure pneumatic conveying systems for sodium bicarbonate applications, several factors must be considered. The choice depends on the specific operational requirements, such as the distance between the source and destination, the material's physical properties (e.g., particle size, density, moisture content), and the desired system efficiency. Negative pressure systems are often preferred for short to medium distances and fine powders due to their lower energy consumption and reduced risk of product degradation. In contrast, positive pressure systems are more suitable for long-distance transport or when handling bulk materials with higher flow rates. The decision also involves evaluating the initial investment costs versus long-term operational expenses, as well as the maintenance requirements for each system type.
Sodium bicarbonate, commonly used in food, pharmaceutical, and chemical industries, requires efficient and hygienic material handling to maintain product quality and safety. Pneumatic conveying systems, whether negative or positive pressure, offer a non-contact method of transport that minimizes contamination risks. For example, in food processing facilities, negative pressure systems are often employed to transport sodium bicarbonate from storage silos to production lines, ensuring a clean and controlled environment. In pharmaceutical applications, positive pressure systems may be preferred to maintain sterile conditions and prevent cross-contamination, as they can be designed with sealed components and integrated filtration systems. Additionally, the choice of system affects the overall system design, including the layout of pipelines, the placement of hoppers and receivers, and the integration with existing production equipment. Proper system sizing and material flow analysis are critical to ensure optimal performance and minimize downtime.
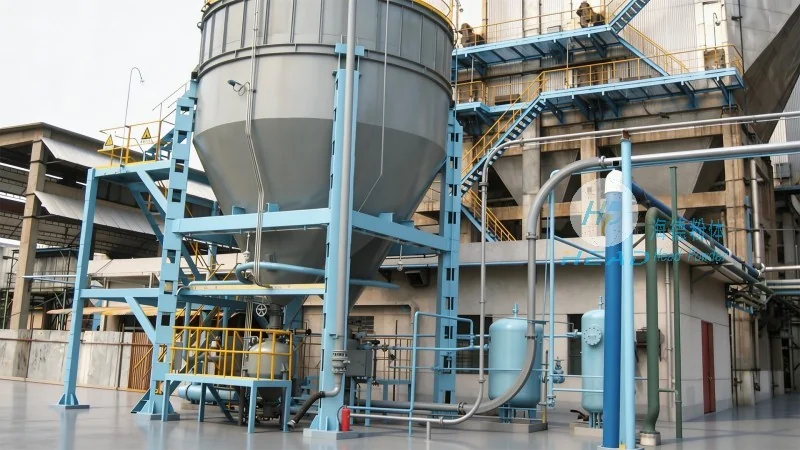
HeadPowder's expertise in sodium bicarbonate pneumatic conveying technology provides industrial clients with reliable and efficient solutions tailored to their specific needs. By understanding the technical differences between negative and positive pressure systems, companies can select the most appropriate method for their operations, balancing factors such as distance, material properties, and operational costs. The company's commitment to advanced engineering and customer-centric solutions ensures that clients receive systems that enhance productivity, maintain product integrity, and comply with industry standards. Whether for short-distance fine powder transport or long-distance bulk material handling, HeadPowder's pneumatic conveying systems offer robust and effective solutions for sodium bicarbonate applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top