For industrial applications involving malt handling, efficient and reliable material transport is crucial. The malt pneumatic conveying system, a specialized technology for moving malt grains and other bulk materials, offers a solution that combines performance with flexibility. This article explores the classification and key components of such systems, providing insights into their design and functionality, as presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for bulk material handling.
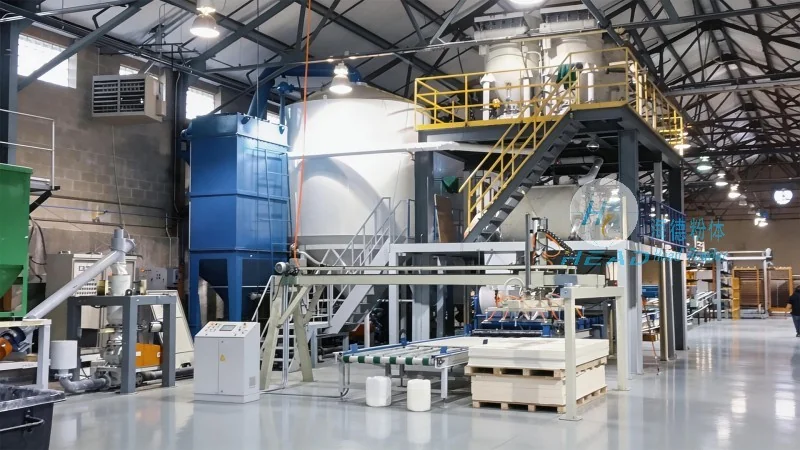
Malt pneumatic conveying systems are engineered to transport malt from one location to another within a production facility or between different stages of processing. These systems utilize air or gas as the conveying medium, enabling the movement of malt through pipelines without the need for mechanical components like belts or buckets. The primary goal is to ensure consistent, low-damage transport of malt, which is essential for maintaining product quality in brewing and other food processing applications.
Malt pneumatic conveying systems can be broadly categorized into two main types based on the pressure differential used during operation: positive pressure systems and negative pressure systems. Each type has distinct characteristics and is suited to different operational requirements.
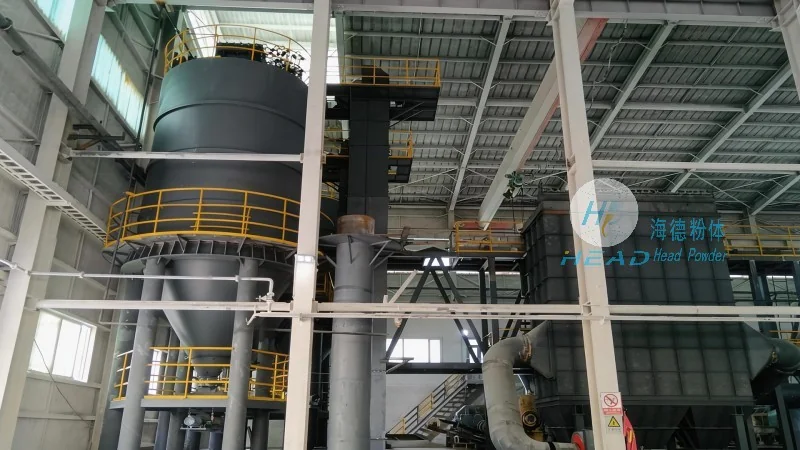
Positive pressure systems operate by blowing air or gas into the conveying line, creating a pressure higher than the ambient air pressure. This method is often preferred for applications where the receiving hopper or silo is at a higher elevation than the source, as the system can effectively lift the malt vertically. The positive pressure also helps in preventing contamination and maintaining product integrity by ensuring a sealed environment.
Negative pressure systems, on the other hand, operate by creating a vacuum in the conveying line, drawing the malt from the source into the system. This approach is typically used when the receiving point is at a lower level than the source, as the system can pull the malt down through the pipelines. Negative pressure systems are also beneficial in environments where dust control is a priority, as the sealed pipeline prevents dust from escaping into the surrounding air.
Regardless of the classification, a typical malt pneumatic conveying system consists of several essential components that work in tandem to ensure efficient operation. These components include the feeding device, conveying pipeline, separation and collection equipment, and air filtration units.
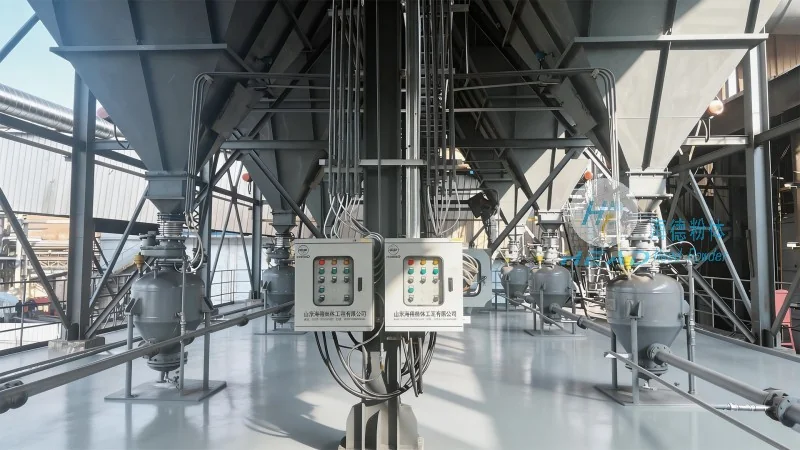
The feeding device is responsible for introducing the malt into the conveying system. It is designed to handle bulk materials and ensure a consistent flow rate. Common feeding devices include rotary valves, star feeders, and screw feeders. The choice of feeding device depends on the specific characteristics of the malt, such as its size, moisture content, and flowability. For malt, which can be somewhat sticky or have irregular shapes, a rotary valve or star feeder is often preferred as it can handle the material without causing blockages or damage.
The conveying pipeline is the core of the system, responsible for transporting the malt through the system. It is typically made of materials such as stainless steel or plastic, which are resistant to corrosion and wear. The pipeline is designed with smooth internal surfaces to minimize friction and prevent the buildup of malt particles. The diameter and length of the pipeline are carefully selected based on the required conveying capacity and the distance between the source and the receiving point. For malt, a pipeline diameter of 100mm to 200mm is commonly used, depending on the flow rate and the type of system (positive or negative pressure).
After the malt has been conveyed to its destination, it needs to be separated from the conveying air and collected in a hopper or silo. The separation equipment typically includes a cyclone separator and a bag filter. The cyclone separator uses centrifugal force to separate the malt from the air, while the bag filter captures any remaining dust particles. The collected malt is then stored in a container for further processing. The efficiency of the separation system is critical to maintaining product quality and preventing contamination.
Since malt is a dry, powdery material, it can generate significant dust during the conveying process. To ensure a clean and safe working environment, air filtration units are essential. These units typically consist of a pre-filter and a final filter, which remove dust particles from the air before it is released back into the environment. The choice of filter material depends on the dust characteristics and the required filtration efficiency. For malt, a high-efficiency particulate air (HEPA) filter is often used to ensure that the air is free from any residual dust particles.
Malt pneumatic conveying systems are widely used in the brewing industry and other food processing applications where malt is a key ingredient. The benefits of using such systems include improved efficiency, reduced labor costs, and enhanced product quality. By eliminating the need for manual handling, the system minimizes the risk of contamination and damage to the malt. Additionally, the sealed environment of the system helps in maintaining the moisture content and flavor of the malt, which is crucial for producing high-quality beer and other malt-based products.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top