Malt material handling systems are essential components in the brewing and food processing industries, designed to efficiently transport malt grains and other raw materials from storage to processing areas. These systems play a critical role in ensuring smooth production workflows, maintaining product quality, and optimizing operational efficiency. For businesses involved in malt production, understanding the functionality and design principles of such systems is crucial for maintaining competitiveness and meeting production demands.
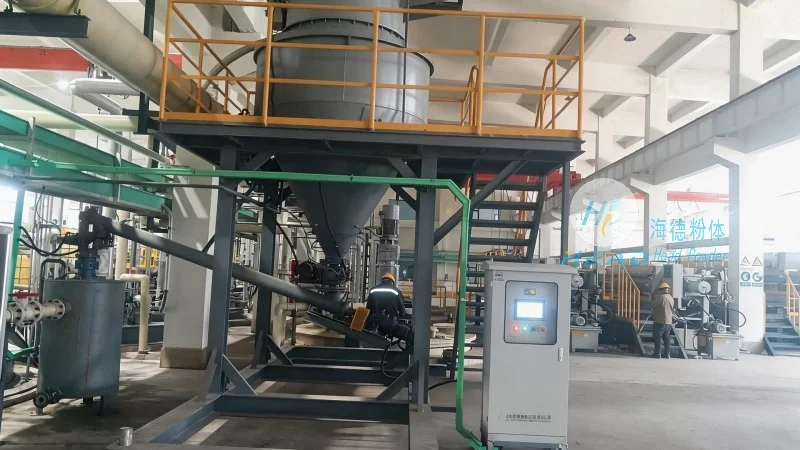
HeadPowder Engineering, based in Shandong, China, is a leading provider of specialized engineering solutions for the food and beverage industry. With a strong focus on innovation and customer-centric design, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling systems. HeadPowder Engineering combines years of industry experience with advanced technology to deliver tailored solutions that meet the unique needs of each client.
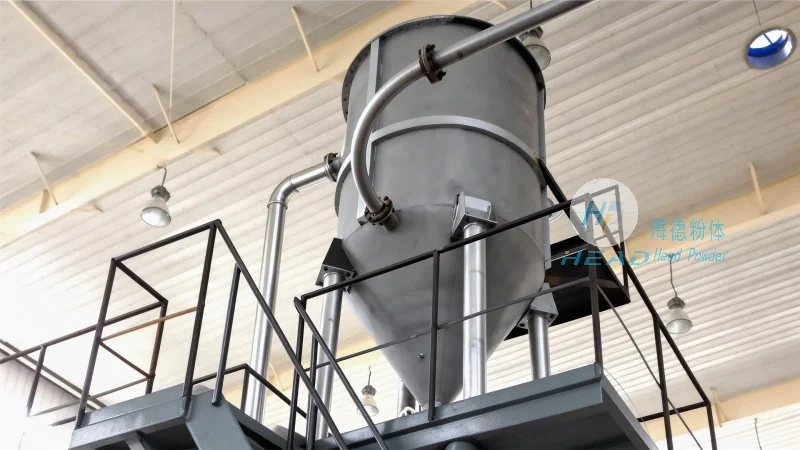
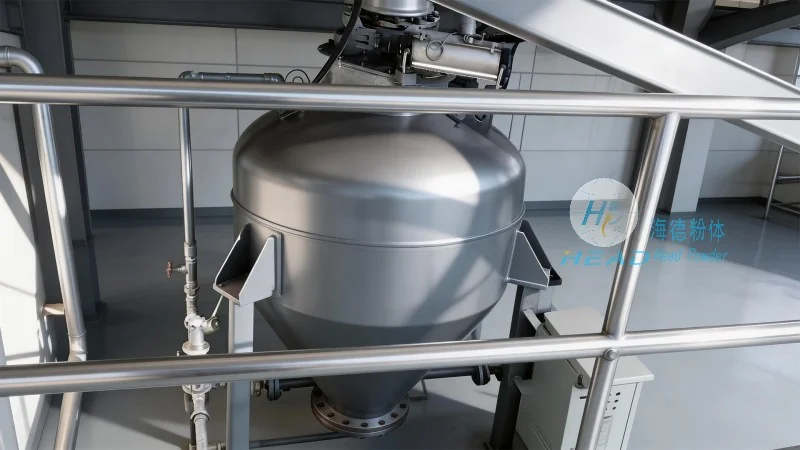
The design of a malt material handling system involves several key principles aimed at ensuring durability, efficiency, and safety. First, the system must be constructed from materials that are resistant to corrosion and wear, as malt grains can be abrasive and contain moisture. Common materials include stainless steel, which provides excellent resistance to chemical and physical stress. Second, the system's layout is carefully planned to minimize material handling distances and reduce energy consumption. This includes the use of gravity-fed chutes, conveyor belts, and elevators that are sized and positioned to optimize flow rates. Third, the system incorporates safety features such as emergency stop buttons, overload protection, and proper ventilation to protect operators and prevent accidents. Additionally, the design considers the need for easy maintenance and cleaning, with components that can be easily accessed and disassembled for routine checks and sanitation.
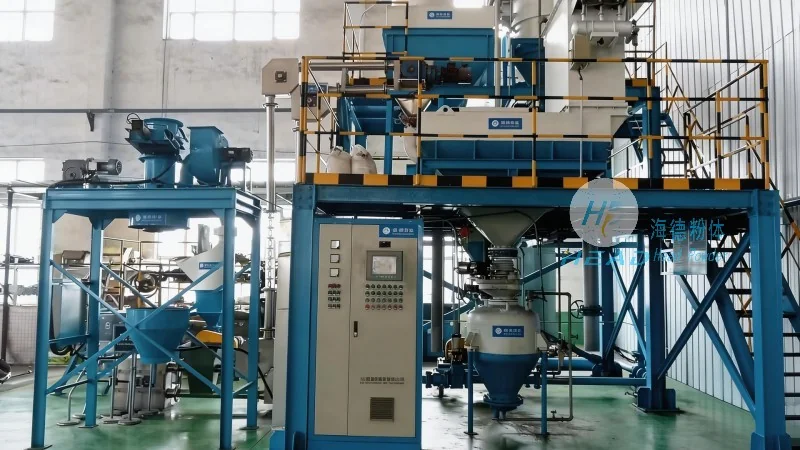
A typical malt material handling system consists of several interconnected components that work together to move and store malt. The primary components include storage silos or bins, feeders (such as rotary or vibratory feeders) that control the flow of malt from storage to processing equipment, conveyors (including belt conveyors, screw conveyors, and bucket elevators) that transport malt horizontally or vertically, and transfer points that direct the flow to different parts of the production line. Each component is designed to handle the specific characteristics of malt, such as its density, moisture content, and particle size. For example, belt conveyors are commonly used for horizontal transport due to their ability to handle large volumes of material with minimal maintenance, while bucket elevators are ideal for vertical lifting due to their high capacity and efficiency. The feeders are crucial for controlling the flow rate, as they prevent overloading of downstream equipment and ensure consistent material supply. Additionally, the system may include dust collection and filtration systems to maintain a clean and safe working environment, as malt dust can be a fire hazard and pose health risks.
Implementing a well-designed malt material handling system offers numerous benefits for breweries and food processing facilities. First, it significantly improves production efficiency by reducing the time and labor required to move malt from storage to processing. This allows for faster batch processing and increased overall output. Second, the system enhances product quality by maintaining consistent material flow and preventing contamination or degradation of the malt. This is particularly important for sensitive malt varieties that require careful handling to preserve their flavor and nutritional properties. Third, the system improves safety by reducing manual handling of heavy or bulky malt bags, minimizing the risk of workplace injuries. Additionally, the use of automated systems reduces the need for human intervention, which can lead to lower labor costs and improved consistency in production. The applications of malt material handling systems are widespread, including in traditional breweries, craft beer producers, malt houses, and food processing plants that use malt as an ingredient in products such as malted milk, breakfast cereals, and snacks.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top