Coal ash granular material conveying systems are essential components in industrial processes, particularly in power generation and waste management sectors. These systems are designed to transport coal ash, a byproduct of coal combustion, from one location to another efficiently and safely. Understanding the components and design principles of such systems is crucial for optimizing operational efficiency and ensuring compliance with environmental standards.
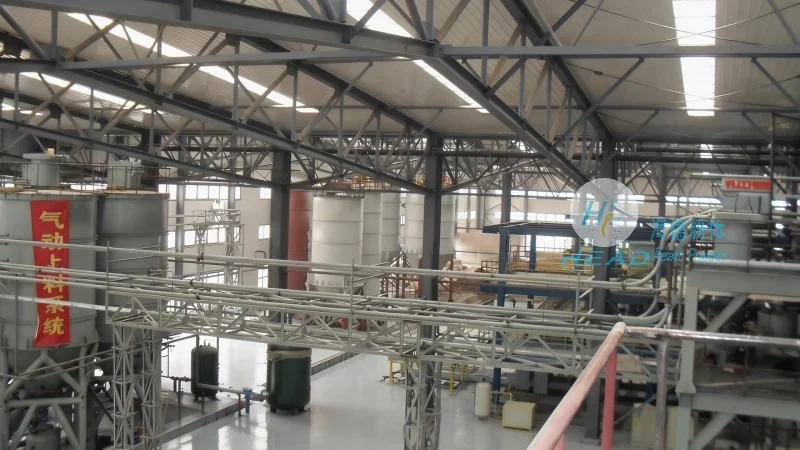
HeadPowder, a prominent engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling systems. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient conveying solutions. The company’s expertise in coal ash handling systems is built on years of experience and a commitment to delivering high-quality, durable equipment tailored to specific operational needs.
The design of coal ash granular material conveying systems involves several key principles aimed at ensuring optimal performance, safety, and longevity. One of the primary considerations is the material's physical properties, such as particle size, density, and moisture content, which influence the choice of conveying method. For coal ash, which typically consists of fine particles, pneumatic conveying systems are often preferred due to their ability to handle dry, dusty materials without the need for mechanical components that might cause wear and tear.
Another critical design principle is the system's capacity and flow rate. Engineers must calculate the required throughput based on the plant's production capacity and the volume of coal ash generated. This involves selecting appropriate equipment like screw conveyors, bucket elevators, or pneumatic pipelines that can handle the desired flow rates while minimizing energy consumption. The system's layout also plays a significant role, as it must be integrated seamlessly with existing infrastructure to avoid disruptions in the overall process.
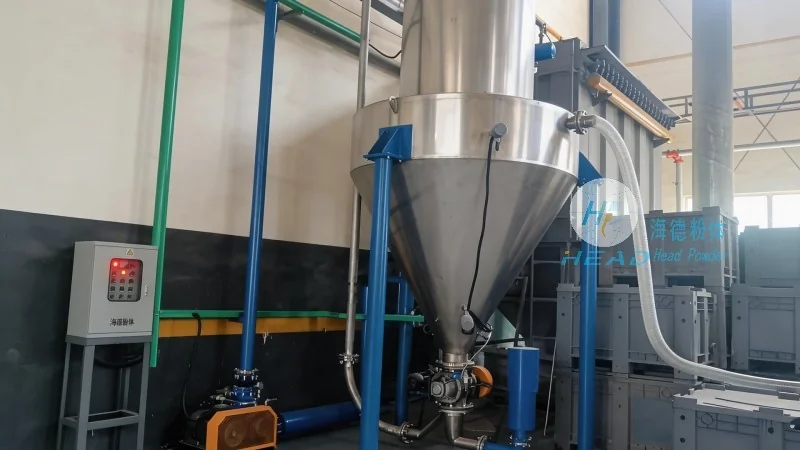
Coal ash granular material conveying systems typically consist of several interconnected components, each serving a specific function to ensure smooth operation. The primary components include feeders, conveyors, and control systems. Feeders, such as rotary valves or vibratory feeders, are used to regulate the flow of coal ash from storage silos or hoppers into the conveying system. These devices ensure a consistent feed rate, preventing overloading or underloading of the conveyor. Conveyors, which can be either mechanical (e.g., screw conveyors, belt conveyors) or pneumatic (e.g., positive displacement blowers, vacuum pumps), transport the coal ash from the feeder to the discharge point. Mechanical conveyors are suitable for handling larger particles or bulk materials, while pneumatic systems are ideal for fine, dusty coal ash that requires dust control measures.
Control systems are another essential part of the design, as they monitor and regulate the operation of the conveying system. These systems may include sensors to detect material levels, flow rates, and pressure, as well as automated controls to adjust the system's performance based on real-time conditions. For example, a control system might adjust the speed of a screw conveyor to maintain a constant flow rate or activate a dust suppression system when high dust levels are detected. This integration of sensors and controls enhances the system's efficiency and safety, reducing the risk of material buildup or equipment failure.
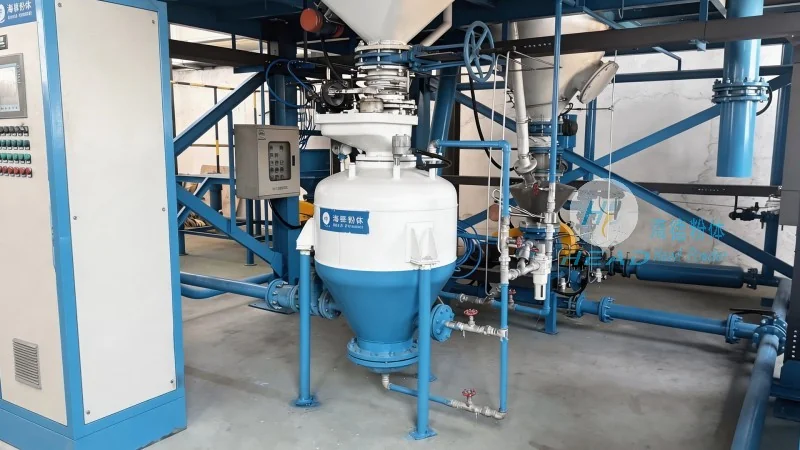
Implementing a coal ash granular material conveying system offers several advantages for industrial operations. First, it improves operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing downtime. Automated systems can operate continuously, ensuring a steady supply of coal ash to downstream processes like storage or disposal. Second, these systems enhance safety by eliminating the need for workers to handle or transport heavy, dusty materials manually. This reduces the risk of occupational hazards, such as respiratory illnesses or injuries from handling bulk materials. Third, the design of modern conveying systems focuses on energy efficiency, using less power to achieve the desired throughput compared to older, less efficient methods. This not only reduces operational costs but also contributes to environmental sustainability by minimizing energy consumption.
Additionally, coal ash conveying systems are designed to be durable and long-lasting, with components made from materials resistant to corrosion and wear. For example, screw conveyors are often constructed from stainless steel or other corrosion-resistant alloys to withstand the acidic and abrasive nature of coal ash. Pneumatic pipelines are typically made from high-quality plastic or metal, ensuring they can handle the pressure and flow rates required for efficient material transport. The use of durable materials reduces maintenance costs and extends the system's service life, providing a better return on investment for industrial facilities.
Coal ash granular material conveying systems are critical for the efficient and safe handling of coal ash in industrial applications. The design principles and components discussed above highlight the importance of tailored solutions that address specific operational needs. HeadPowder, with its expertise and commitment to quality, offers comprehensive engineering solutions for coal ash handling systems. Based in Shandong, China, HeadPowder leverages years of experience to design and deliver systems that meet the highest standards of performance, safety, and reliability. By choosing HeadPowder, industrial facilities can ensure their coal ash conveying operations are optimized for efficiency, cost-effectiveness, and environmental compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top