Silicate materials, such as clay, glass, and cement raw materials, are fundamental components in various industrial applications. Handling these materials efficiently is crucial for maintaining production efficiency and ensuring product quality. A silicate material handling system is a specialized setup designed to transport, store, and manage these materials from raw form to processing stages. This system integrates various equipment and processes tailored to the unique properties of silicate materials, which often include high moisture content, abrasive nature, and varying particle sizes.
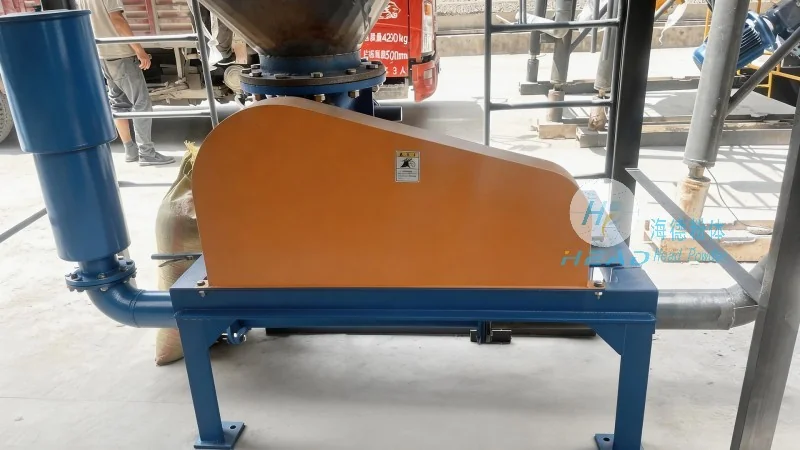
Silicate materials are characterized by their complex chemical and physical properties. For instance, clay, a common silicate, is often sticky and can cause equipment wear if not handled properly. Glass raw materials, on the other hand, are brittle and require gentle handling to prevent breakage. Cement raw materials, including limestone and silica sand, are typically bulk materials that need to be moved in large quantities. The handling needs for these materials vary, but common challenges include material flow control, dust suppression, and equipment durability. A well-designed silicate material handling system addresses these challenges by incorporating features like conveyor belts, silos, and dust collection systems.
A typical silicate material handling system consists of several key components that work in tandem to ensure smooth material flow. The primary components include:
- **Conveyors**: These are the backbone of the system, used to transport materials horizontally or vertically. Belt conveyors are commonly used for bulk silicate materials due to their ability to handle high volumes and abrasive materials. Screw conveyors are ideal for handling fine powders and materials with high moisture content.
- **Silos and Hoppers**: These storage vessels are used to hold raw silicate materials before processing. They are designed to prevent material bridging and ensure uniform flow. The design of silos and hoppers is critical, as improper design can lead to material clogging or uneven discharge.
- **Dust Collection Systems**: Silicate materials are often dusty, and effective dust control is essential for safety and environmental compliance. These systems typically include cyclones, baghouses, or electrostatic precipitators to capture and filter dust particles.
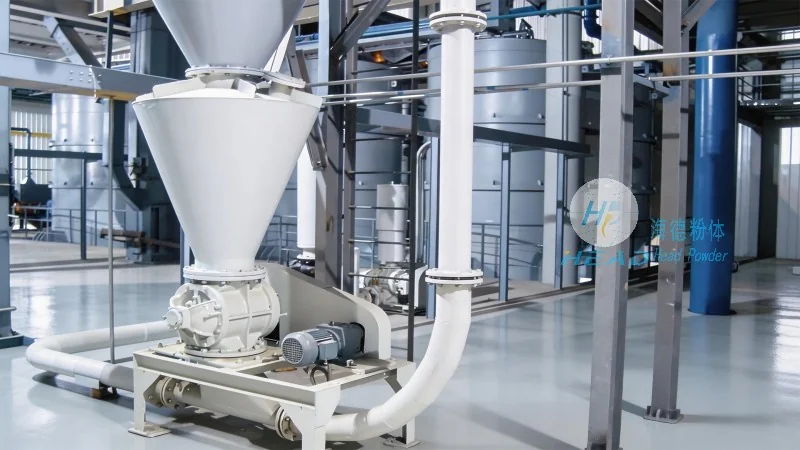
- **Control Systems**: Modern silicate material handling systems are equipped with advanced control systems that monitor and regulate the flow of materials. These systems use sensors and automation to ensure optimal performance and prevent equipment damage.
The design of a silicate material handling system follows several key principles to ensure efficiency and reliability. First, **material compatibility** is crucial. The system's components must be made of materials that can withstand the abrasive and corrosive nature of silicate materials. For example, conveyor belts are often made of rubber or special plastics to resist wear from clay or cement particles.
Second, **flow optimization** is essential. The system is designed to minimize material buildup and ensure consistent flow rates. This involves proper hopper design, slope of conveyor belts, and the use of feeders to control the rate of material discharge.
Third, **dust control** is a critical design consideration. The system must include effective dust suppression measures to protect workers and the environment. This may include wetting the material, using enclosed systems, or installing dust collection equipment.
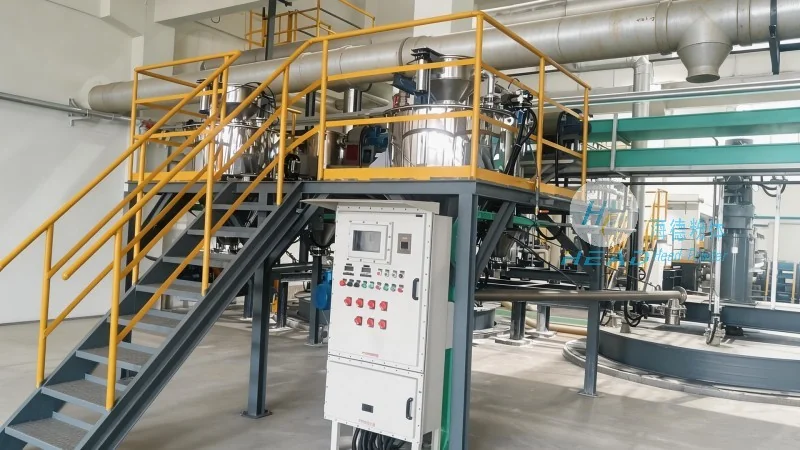
Fourth, **safety and maintenance** are integral to the design. The system is built with safety features such as emergency stops and protective guards. Regular maintenance schedules are also incorporated to ensure the system operates at peak efficiency.
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of specialized material handling solutions for silicate industries. With years of experience, HeadPowder has developed a comprehensive range of systems tailored to the unique needs of silicate material processing. The company's expertise lies in designing and manufacturing equipment that addresses the challenges of handling abrasive, dusty, and high-volume silicate materials.
HeadPowder's solutions include custom-designed conveyor systems, silos, and dust control equipment. The company's team of engineers works closely with clients to understand their specific requirements and develop tailored solutions. For example, a client in the glass industry might require a system that handles silica sand with high precision, while a client in the cement industry might need a system that can handle limestone and other raw materials efficiently.
HeadPowder's commitment to quality and innovation has made it a trusted partner in the silicate material handling industry. The company's products are designed to meet international standards and are backed by a comprehensive warranty and after-sales support. By choosing HeadPowder, clients can ensure that their silicate material handling systems are efficient, reliable, and cost-effective.
Silicate material handling systems are essential for the efficient processing of silicate materials in various industries. A well-designed system integrates key components and follows critical design principles to ensure smooth material flow, minimize downtime, and maintain product quality. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing specialized solutions that address the unique challenges of silicate material handling. By investing in a high-quality silicate material handling system, industries can enhance their production efficiency, reduce costs, and improve overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top