Understanding the ABS Granular Material Conveying System and Its Design Principles
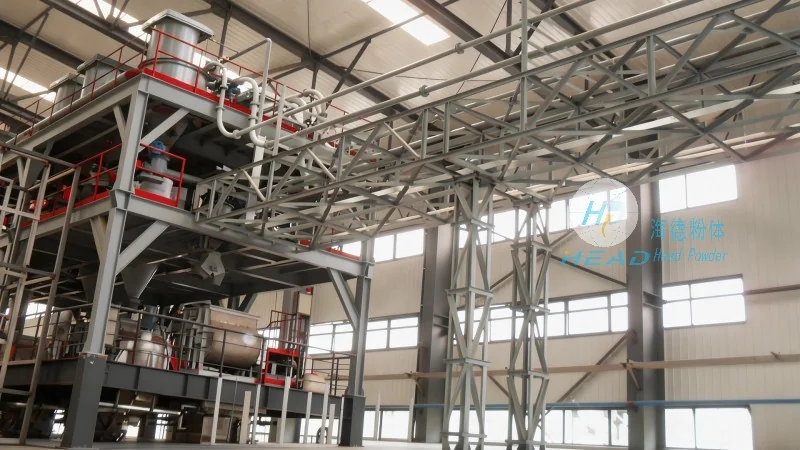
The ABS granular material conveying system is a specialized industrial solution designed to efficiently transport bulk materials in powder or granular form. As a key component in various manufacturing and processing industries, this system plays a crucial role in ensuring smooth material flow, enhancing operational efficiency, and maintaining product quality. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, the system integrates advanced engineering principles and robust construction to meet the demanding requirements of modern production environments.
HeadPowder, the professional brand under Shandong HeadPowder Engineering Co., Ltd., is dedicated to delivering high-quality conveying solutions tailored to the needs of diverse industries. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the material handling sector. Headquartered in Shandong, China, HeadPowder leverages years of experience and technical expertise to design, manufacture, and supply reliable conveying systems that optimize material transport processes. The company’s focus on precision engineering and customer-centric approach ensures that each system is tailored to meet specific operational challenges and performance standards.
The design of the ABS granular material conveying system is built upon several fundamental principles that ensure optimal performance and durability. First, the system incorporates a robust frame and components that can withstand the mechanical stresses associated with handling abrasive or heavy granular materials. The use of high-quality materials, such as stainless steel or corrosion-resistant alloys, is critical in maintaining the integrity of the system over extended periods of operation. Additionally, the system is engineered to minimize material degradation and contamination, which is essential for industries where product purity is paramount.
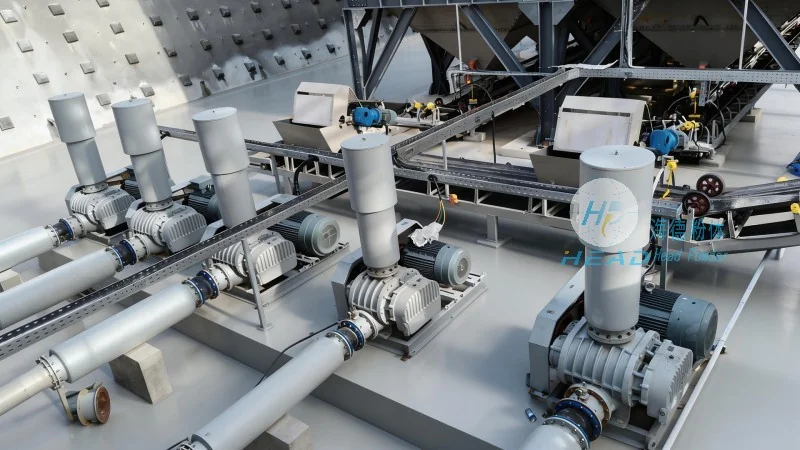
Second, the conveying mechanism is designed to provide consistent and controlled material flow. This is achieved through the integration of precision-driven components, including drive systems, pulleys, and tensioning mechanisms. The system’s design allows for adjustable speed and flow rates, enabling operators to adapt to varying production demands. Furthermore, the system incorporates features such as material separation and cleaning mechanisms to prevent blockages and ensure continuous operation. These design elements collectively contribute to the system’s reliability and efficiency in transporting granular materials.
Third, the system emphasizes energy efficiency and operational cost reduction. By optimizing the drive system and reducing friction in moving parts, the conveying system minimizes energy consumption while maintaining high throughput. The use of advanced control systems allows for real-time monitoring and adjustment of operational parameters, further enhancing energy efficiency. Additionally, the modular design of the system facilitates easy maintenance and replacement of components, reducing downtime and overall operational costs. These design considerations make the ABS granular material conveying system a cost-effective solution for industries seeking to improve their material handling processes.
The ABS granular material conveying system offers several key features that enhance its performance and usability. One of the primary advantages is its ability to handle a wide range of materials, including powders, granules, and even fine particles. The system’s design accommodates different material characteristics, such as density, moisture content, and abrasiveness, ensuring effective transport without degradation. Another significant feature is the system’s flexibility in terms of layout and integration with existing production lines. The modular construction allows for easy installation and customization to fit specific facility requirements, minimizing the need for extensive modifications.
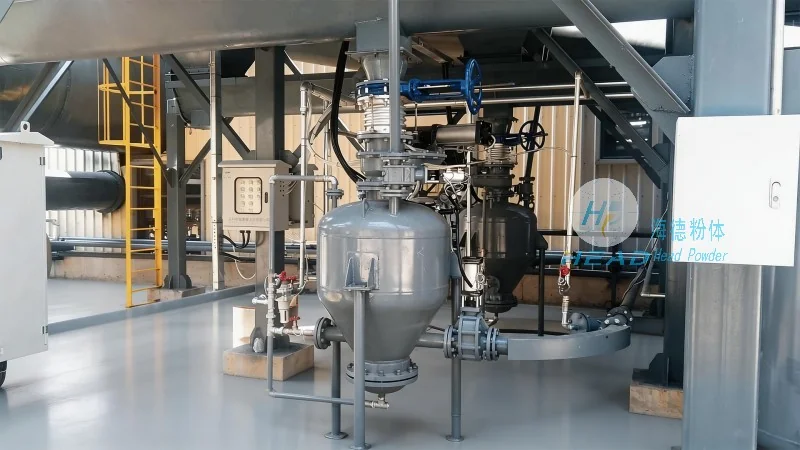
Furthermore, the system is equipped with advanced safety features to protect operators and equipment. These include emergency stop mechanisms, overload protection, and monitoring systems that alert operators to potential issues. The use of sealed components and proper ventilation helps maintain a safe working environment by preventing dust accumulation and ensuring proper air quality. The system’s durability and low maintenance requirements also contribute to its long-term cost-effectiveness, making it a preferred choice for industries with high operational demands.
The ABS granular material conveying system is widely used across various industries that rely on bulk material handling. In the chemical industry, the system is employed to transport raw materials and finished products, ensuring smooth production processes. The food and beverage industry utilizes the system for handling ingredients like flour, sugar, and other granular components, maintaining product purity and quality. The pharmaceutical industry also benefits from the system’s ability to handle sensitive materials, ensuring compliance with stringent regulatory standards. Additionally, the system is used in the mining and construction sectors for transporting raw materials such as sand, gravel, and minerals. Its versatility and reliability make it an essential component in these industries, contributing to increased productivity and operational efficiency.
In conclusion, the ABS granular material conveying system is a sophisticated and reliable solution for efficiently transporting bulk materials in various industrial applications. Developed by Shandong HeadPowder Engineering Co., Ltd., the system incorporates advanced design principles, robust construction, and user-friendly features that enhance performance and operational efficiency. By understanding the design principles and benefits of this system, industries can make informed decisions to improve their material handling processes and achieve greater productivity. With its commitment to quality and innovation, HeadPowder continues to provide cutting-edge conveying solutions that meet the evolving needs of modern manufacturing and processing industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top