Continuous material feeding conveyor systems are essential industrial equipment designed to transport bulk materials or products in a continuous, unbroken flow. These systems are widely used across various industries to enhance production efficiency, improve material handling accuracy, and streamline manufacturing processes. Understanding the core functions and design principles of such systems is crucial for optimizing operational performance and ensuring reliable material transfer.
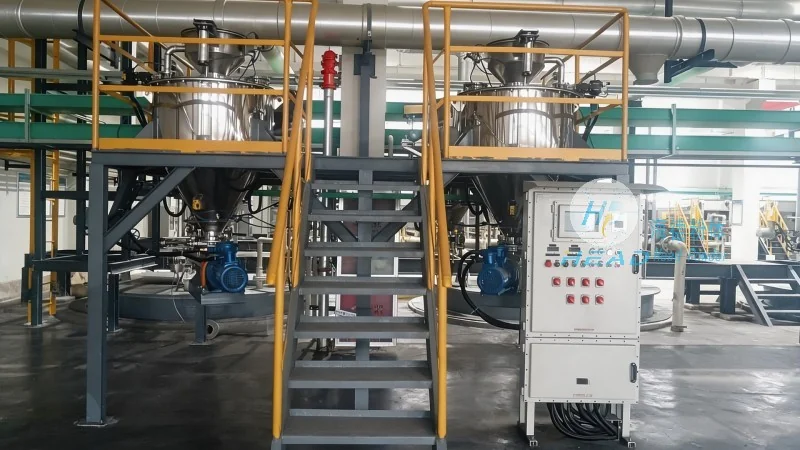
A continuous material feeding conveyor system, often referred to as a bulk material conveyor or feeding conveyor, is a mechanical device that moves materials from one location to another without interruption. Unlike batch processing systems, these conveyors operate continuously, ensuring a steady supply of materials to downstream processes. The primary goal is to facilitate efficient material transfer, reduce labor costs, and minimize downtime in industrial settings. These systems are particularly valuable in applications where large volumes of materials need to be handled, such as in mining, agriculture, manufacturing, and logistics.
The design of a continuous material feeding conveyor system is based on several key principles that ensure optimal performance and reliability. These principles include structural integrity, material compatibility, and operational efficiency. Engineers typically consider factors like the type of material being conveyed (e.g., granular, powders, or bulk solids), the required conveying capacity, and the distance over which materials need to be transported. The design also incorporates elements such as drive mechanisms, control systems, and safety features to meet industry standards and user requirements.
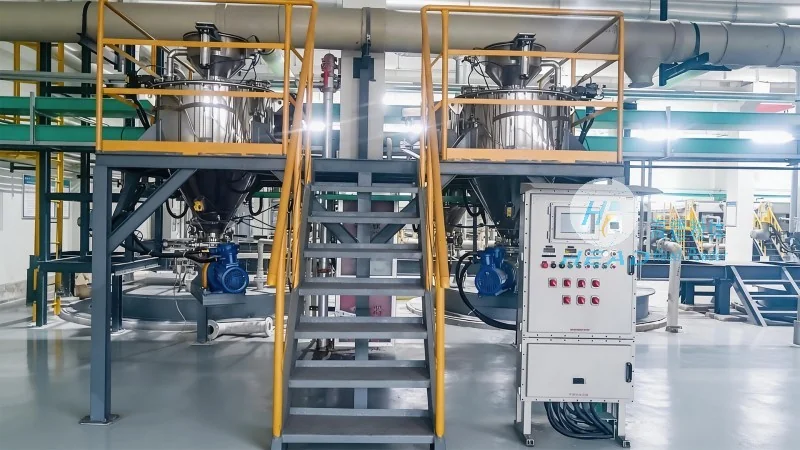
Continuous material feeding conveyor systems consist of several critical components that work in harmony to achieve effective material transfer. The main components include the feeding mechanism, conveyor belt or conveyor structure, drive system, control panel, and safety devices. The feeding mechanism, such as a hopper or feeder, is responsible for supplying materials to the conveyor. The conveyor belt or structure, made from durable materials like rubber or metal, transports the materials along the designated path. The drive system, which may include motors and pulleys, provides the necessary power to move the conveyor. The control panel allows operators to monitor and adjust the system's operation, while safety devices ensure compliance with safety regulations and prevent accidents.
Continuous material feeding conveyor systems are versatile and find applications in a wide range of industries. In the chemical industry, these systems are used to transport raw materials and finished products, ensuring a consistent flow of chemicals. In the food and beverage sector, they are employed to handle ingredients like grains, powders, and liquids, maintaining hygiene and efficiency. The pharmaceutical industry also utilizes such systems for the safe and precise handling of medicinal ingredients. Additionally, in the mining and construction sectors, these conveyors are essential for transporting minerals, ores, and construction materials. The adaptability of continuous material feeding systems makes them suitable for various operational environments and material types.
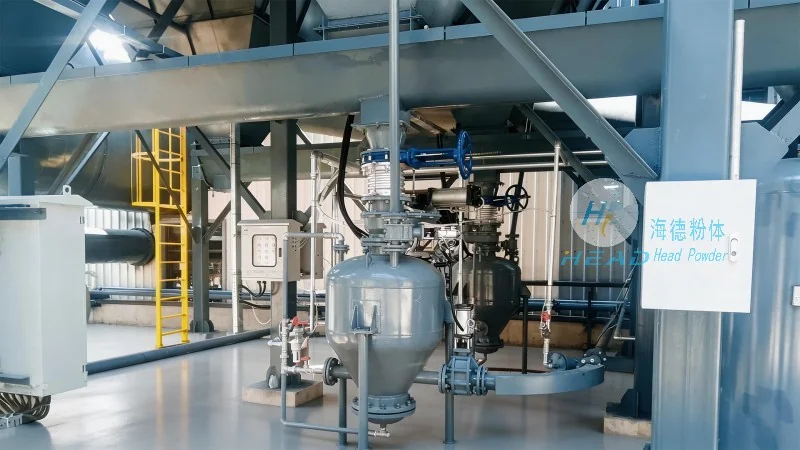
Implementing continuous material feeding conveyor systems offers numerous advantages that contribute to improved operational outcomes. One of the primary benefits is increased efficiency, as these systems can handle large volumes of materials at a consistent rate, reducing bottlenecks in production lines. Another advantage is enhanced accuracy and precision, as the continuous flow minimizes material loss and ensures uniform distribution. Automation is another key benefit, as these systems can be integrated with other industrial equipment, reducing the need for manual intervention and lowering labor costs. Furthermore, continuous feeding systems improve safety by minimizing human exposure to hazardous materials and reducing the risk of accidents associated with manual handling. These advantages make continuous material feeding systems a preferred choice for modern industrial operations.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of industrial conveyor systems and material handling equipment. The company is headquartered in Shandong, China, and specializes in designing, manufacturing, and supplying high-quality continuous material feeding conveyor systems tailored to meet the diverse needs of various industries. With a strong commitment to innovation and quality, headpowder leverages advanced engineering techniques and materials to develop reliable and efficient conveyor solutions. The company's products are widely recognized for their durability, performance, and adherence to international standards, making them a trusted choice for businesses seeking to optimize their material handling processes. HeadPowder Engineering Co., Ltd. continues to be a key player in the global conveyor industry, providing cutting-edge solutions that enhance operational efficiency and productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top