Bicarbonate powder pneumatic conveying is a specialized method used in industrial processes to transport dry powders, such as sodium bicarbonate, through a pipeline using air or gas as the conveying medium. This technology offers a flexible and efficient solution for moving bulk materials, especially in applications where traditional mechanical conveyors may not be suitable. The process involves creating a pressure differential or using vacuum to move the powder particles along the pipeline, ensuring minimal product degradation and consistent flow rates.
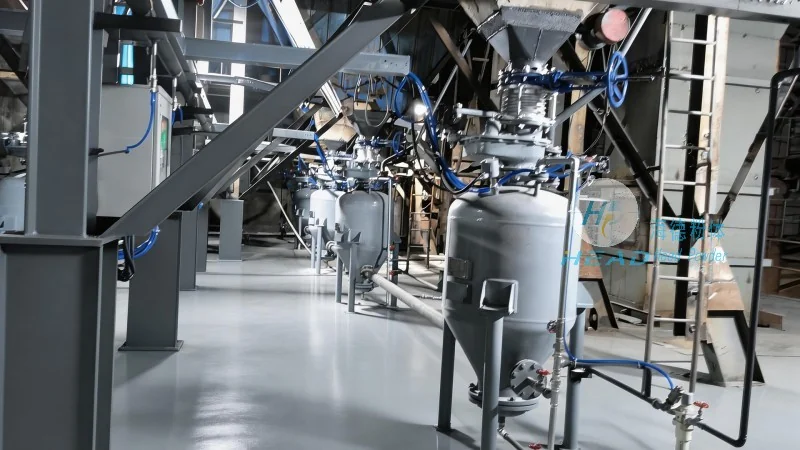
Bicarbonate powder, commonly known as baking soda, is a white crystalline powder with various industrial applications. When transported via pneumatic conveying, it requires careful consideration of particle size, moisture content, and flow characteristics to ensure optimal performance. The method is particularly advantageous for materials that are prone to caking or agglomeration, as the air flow helps maintain particle separation and prevents blockages in the system.
Designing an effective bicarbonate powder pneumatic conveying system involves several key principles that ensure reliability and efficiency. First, the selection of the conveying medium—whether it's positive pressure or negative pressure—depends on the specific material properties and the distance to be covered. Positive pressure systems use a blower to push air and powder through the pipeline, while negative pressure systems use a vacuum to draw the material from the source. For sodium bicarbonate, which is relatively light and has a moderate flowability, positive pressure systems are often preferred due to their ability to handle longer distances and higher flow rates.
Second, the pipeline design is critical. The diameter and length of the pipeline, along with the number of bends and fittings, directly impact the pressure drop and overall system efficiency. Properly sized pipelines minimize friction losses and prevent excessive pressure buildup, which could lead to material degradation or equipment failure. Additionally, the use of smooth, corrosion-resistant materials like stainless steel is essential to avoid contamination and ensure long-term durability.
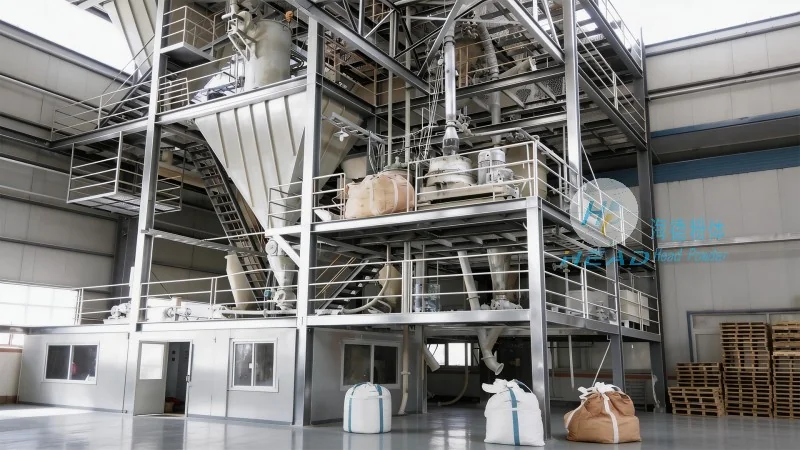
Several components work together to enable the smooth operation of a bicarbonate powder pneumatic conveying system. The feed hopper or silo is the initial point where the powder is stored and prepared for transport. It typically includes a hopper with a discharge valve to control the flow rate and prevent overfilling. The feeder, often a rotary valve or a screw feeder, regulates the amount of powder entering the pipeline, ensuring a consistent feed rate that matches the conveying capacity.
The conveying unit, such as a blower or a vacuum pump, provides the necessary pressure or vacuum to move the powder. For positive pressure systems, a high-pressure blower is used to generate the air flow, while negative pressure systems rely on a vacuum pump to create the suction. The choice of equipment depends on factors like the required flow rate, the distance of the pipeline, and the specific material characteristics. In the case of sodium bicarbonate, a blower with sufficient capacity to handle the light powder particles is essential to maintain the desired velocity and prevent settling.
The pipeline itself is a crucial component, as it must be designed to handle the pressure and flow conditions without causing blockages or degradation. The use of flexible hoses or rigid pipes, depending on the application, allows for flexibility in layout while maintaining structural integrity. Additionally, the inclusion of filters and cyclones is important to separate the powder from the air and prevent dust accumulation in the system. These components help maintain air quality and ensure the longevity of downstream equipment.
Implementing a bicarbonate powder pneumatic conveying system offers several advantages, including the ability to transport materials over long distances, the flexibility to integrate with existing industrial setups, and the reduced risk of product contamination compared to mechanical conveyors. However, there are also considerations to keep in mind. For instance, the energy consumption of the system can be higher than mechanical conveyors, especially for long-distance applications. Additionally, the maintenance of the equipment, particularly the blower and pipeline, requires regular inspection to prevent wear and tear.
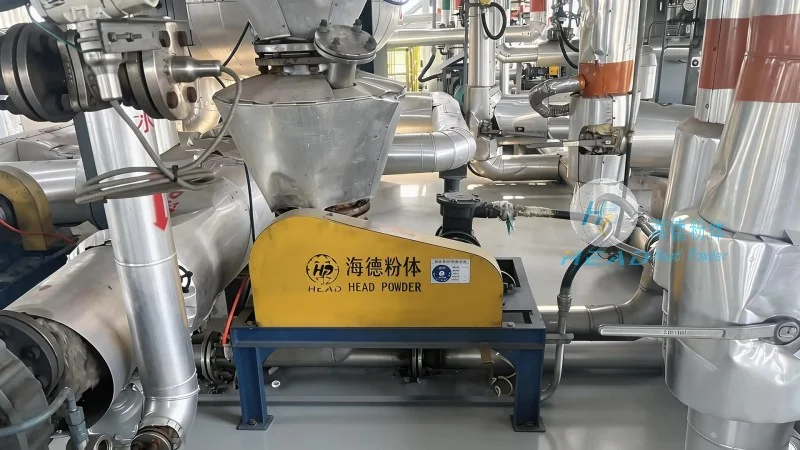
Another consideration is the potential for dust generation and air pollution. Proper filtration and dust collection systems are necessary to comply with environmental regulations and ensure workplace safety. The system's design must also account for the specific properties of sodium bicarbonate, such as its tendency to absorb moisture from the air, which could affect its flowability and quality. By addressing these factors, a well-designed pneumatic conveying system can effectively handle bicarbonate powder while maintaining efficiency and reliability.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of industrial conveying solutions specializing in the design and manufacturing of pneumatic conveying systems for various powder materials. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry, offering tailored solutions that meet the unique needs of its clients. HeadPowder's expertise in material handling and system design ensures that their products are reliable, efficient, and tailored to the specific requirements of each application.
HeadPowder is headquartered in Shandong, China, and has a strong commitment to quality and sustainability. The company adheres to international standards in its manufacturing processes, ensuring that all products are durable, safe, and environmentally friendly. By leveraging advanced technology and a team of experienced engineers, HeadPowder continuously improves its systems to deliver optimal performance and support for its clients. Whether for small-scale or large-scale industrial applications, HeadPowder provides comprehensive solutions that enhance productivity and efficiency in powder handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top